
 DP -70°C
Desiccant Dehumidifier
Rotary honeycomb silica/molecular sieve systems engineered for stable deep moisture adsorption across battery assembly lines.
View Solution SpecsExplore our core industrial air handling lines, built to meet stringent CE, UL, CSA, ASME, and EAC standards with PLC-driven closed-loop automation.
DP -70°C
Rotary honeycomb silica/molecular sieve systems engineered for stable deep moisture adsorption across battery assembly lines.
View Solution Specs Turnkey EPC
End-to-end design, modular hermetic enclosures, dual-rotor deep dehumidifiers, and environmental validation for battery gigafactories.
Explore Dry Rooms Recovery ≥99%
Closed-loop condensation recovery designed for electrode coating exhaustion, drastically lowering operational raw material costs.
NMP System Data RTO + Cooling
Deep-cooling condensation combined with regenerative thermal oxidizers (RTO) to neutralize hazardous stack emissions.
VOC Solutions High COP
Energy-optimized vapor compression dehumidification units tailored for warehouses, clean packing, and primary pre-cooling stages.
Review Units Ultra-Dry Air
Dual-cascade runner desiccant system delivering precise -50°C to -70°C dew point air for sensitive pouch and prism cell electrolyte handling.
Explore Dual-Rotor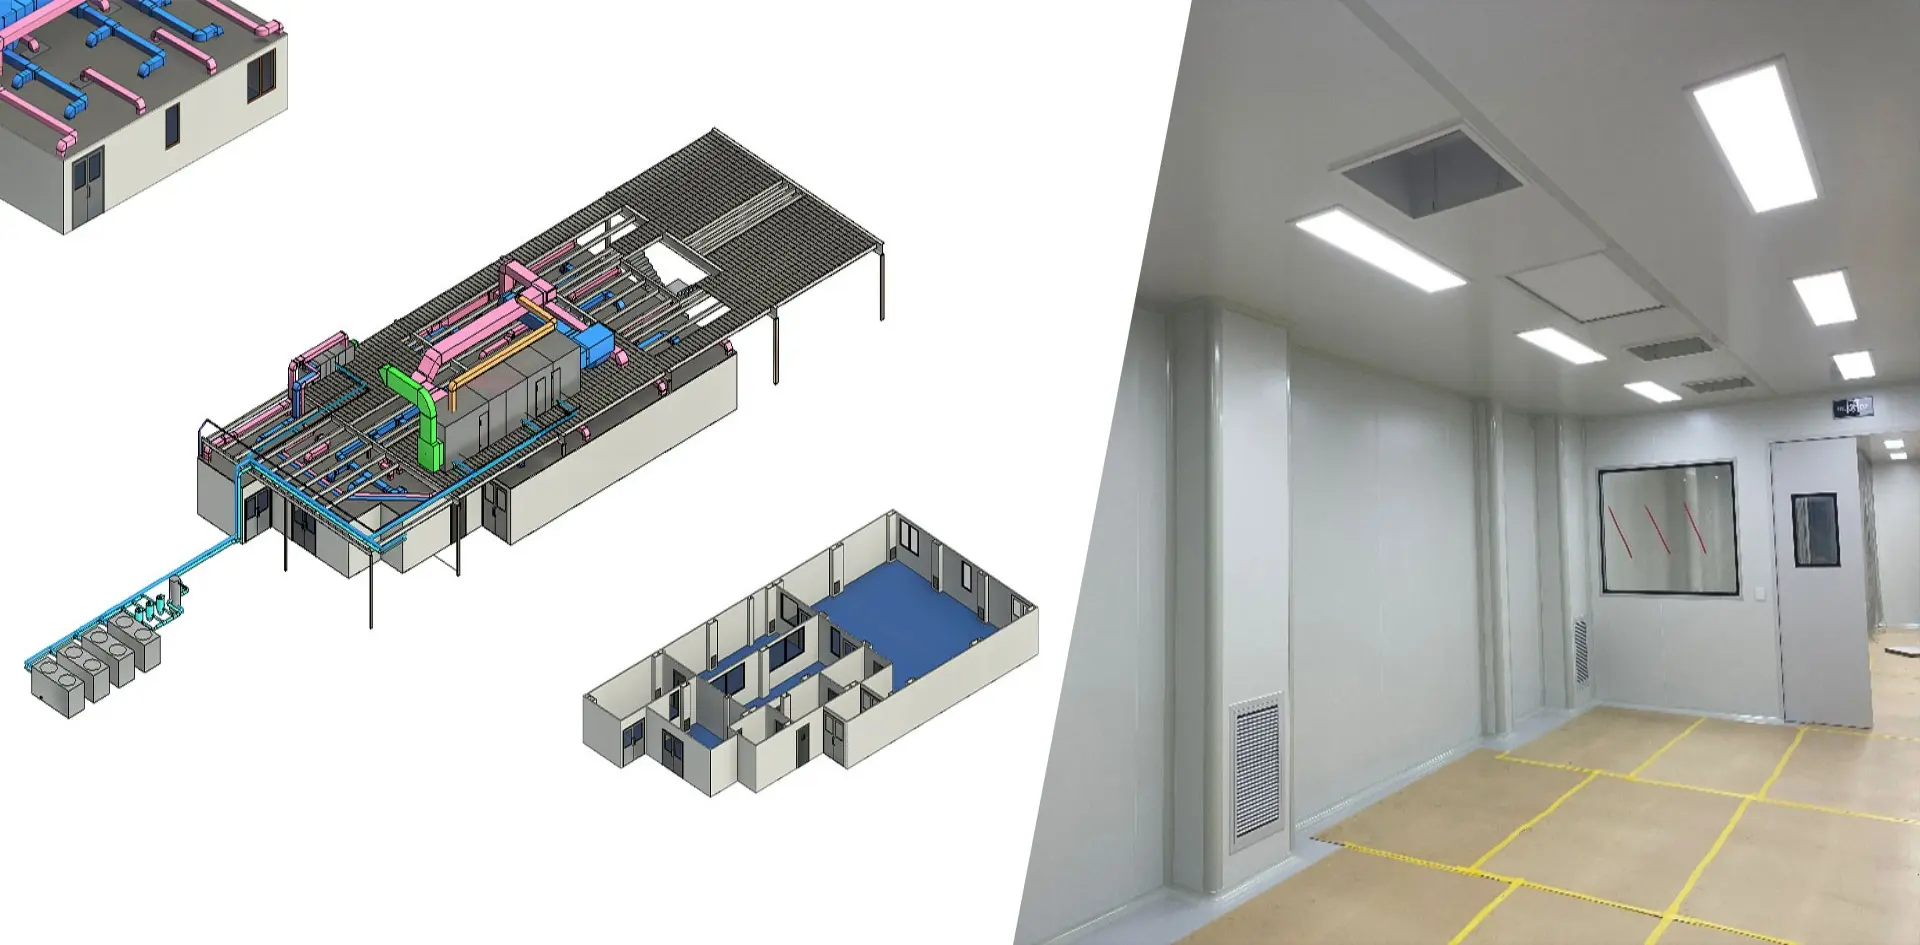 Petrochemical
Multistage compression and chilled condensation units capturing hydrocarbons and dangerous organic gases at transfer terminals.
Learn Chemical Unit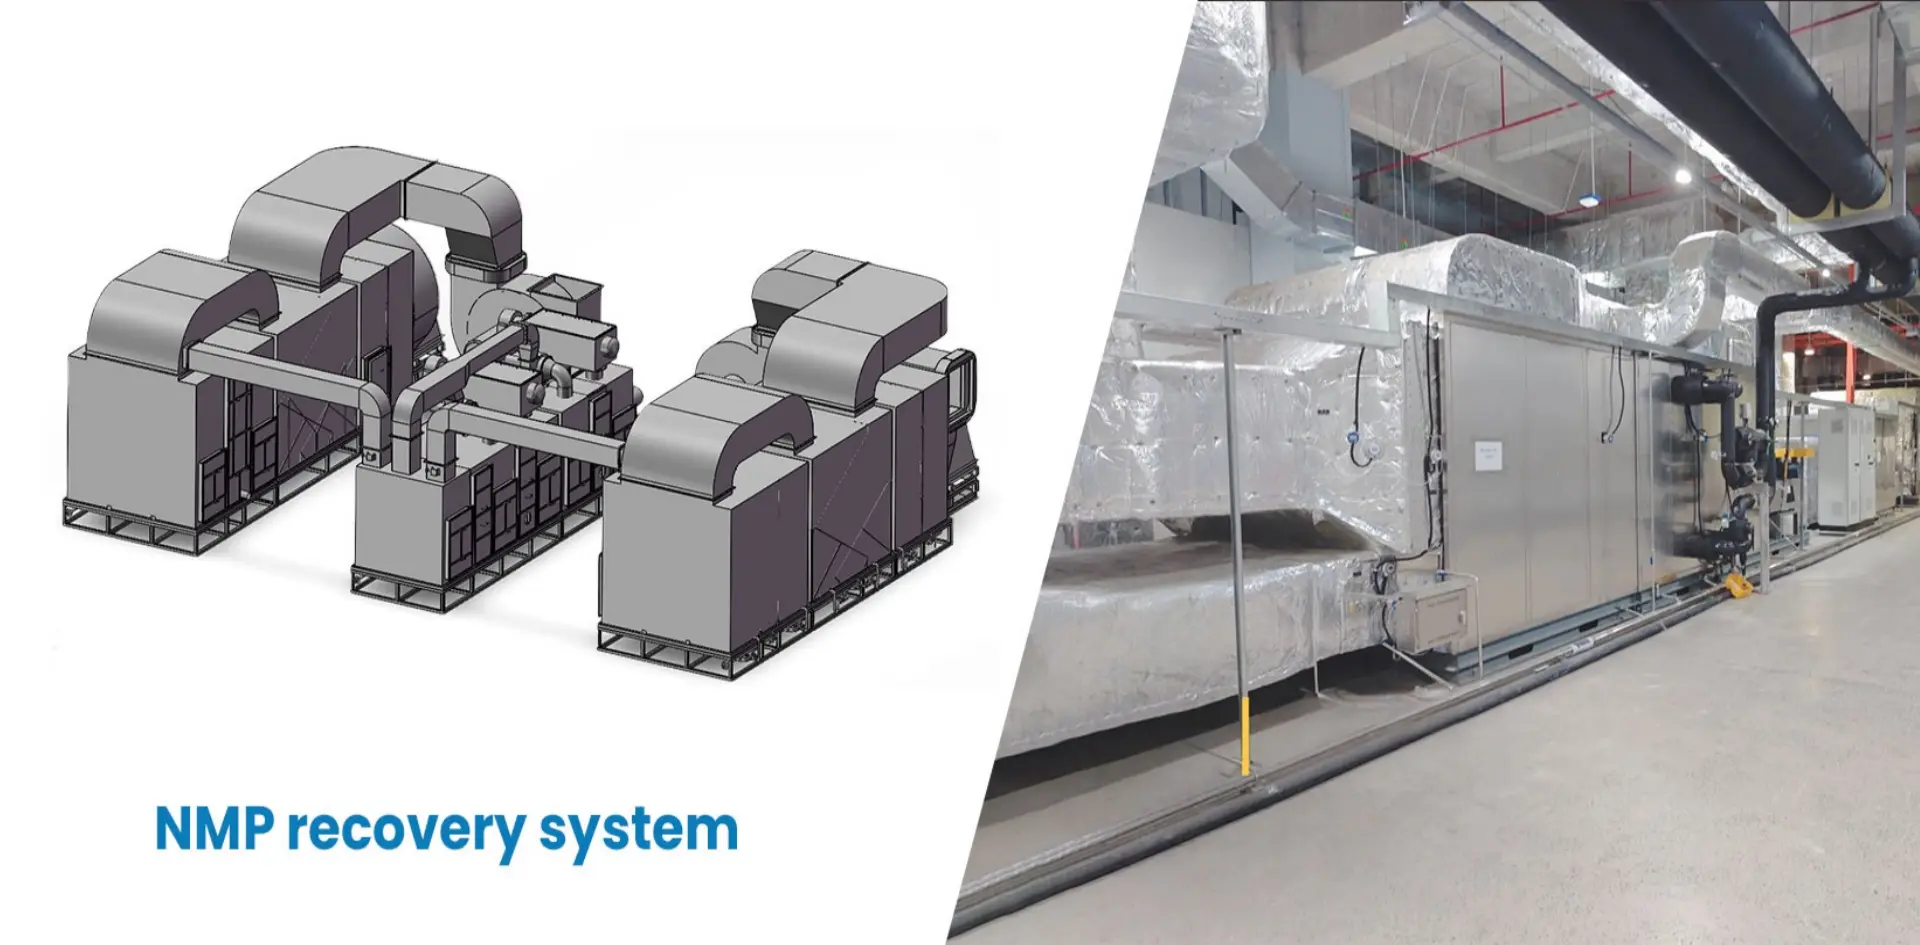 Integrated AHU
Custom packaged desiccant air handling units integrated with chillers, heat recovery coils, and automated Siemens S7 PLC controls.
Factory EngineeringAcross the international manufacturing ecosystem, humidity control has transitioned from a basic comfort HVAC requirement to a mission-critical process parameter dictating product longevity, safety tolerances, and yield viability.
Traces of atmospheric moisture react aggressively with lithium hexafluorophosphate (LiPF6) in electrolyte fluids, producing toxic hydrofluoric acid (HF). Maintaining an airtight environment with dew points below -40°C to -70°C is non-negotiable to prevent internal shorting and accelerated degradation.
Hygroscopic compounds, active pharmaceutical ingredients (APIs), and effervescent formulations cake, lose bio-stability, or fail tablet stamping pressures when relative humidity exceeds 15–20% RH. Automatic industrial desiccant dehumidifiers guarantee stringent cGMP compliance.
Photolithography and dry etching steps exhibit electrostatic discharges and nanoscale oxidation upon micro-fluctuations in atmospheric moisture. Precision PLC automation controls sensible and latent heat loads simultaneously with rapid response loops.
Built under the stringent GJB national military standard, our ruggedized dehumidifiers protect sensitive missile guidance systems, radar avionics, and munitions propellant from micro-corrosion and chemical decomposition during depot preservation.
Deploying automatic desiccant dehumidification systems globally demands acute engineering adaptability to local psychrometric realities, from tropical high-humidity coastal zones to sub-zero continental climates.
In regions such as Southeast Asia and the US Gulf Coast, incoming ambient air carries extreme moisture loads exceeding 28 g/kg. DryAir integrates dual-stage chilled-water pre-cooling coils to mechanically condense out bulk vapor before air impacts the desiccant rotor, cutting regeneration heater energy by up to 42%.
Meeting Western and Northern European directives requires optimized Specific Moisture Extraction Rates (SMER). Our installations integrate secondary waste-heat recovery loops using exhaust thermal energy to preheat the desiccant reactivation air stream, aligning with strict EU carbon budgets.
Delivered units for American Gigafactory programs feature complete compliance with UL 508A electrical panels, NFPA 79 machinery safety standards, and ASME-coded pressure vessels, ensuring seamless permit acquisition and on-site city inspection sign-offs.
Operating from Hangzhou, Zhejiang—the manufacturing epicentre of global clean technology—Hangzhou DryAir Treatment Co., Ltd. leverages comprehensive vertical integration to outpace traditional lead-time constraints.
Our dedicated manufacturing base spans heavy structural metal fabrication, precision laser-welding, rotor assembly bays, and climate-controlled assembly areas, enabling parallel construction of multi-megawatt battery dry room arrays without backlog.
With direct proximity to tier-1 component suppliers for blowers, heat exchangers, variable frequency drives, and synthesized silica gel desiccant substrates, raw lead time is contracted by 35% compared to Western competitors.
Every industrial unit undergoes dynamic testing inside our in-house factory test chamber. We verify airflow CFM, dew point reduction velocity, and electric/steam heat consumption curves before dispatch, preventing commissioning delays.
Selecting appropriate dehumidification technology prevents massive lifecycle energy waste. Compare operational parameters across distinct industrial topologies below:
| Industrial Application | Target Humidity / Metric | Core Dehumidification Topology | System Reference |
|---|---|---|---|
| Lithium Battery Cell Assembly & Electrolyte Injection | -40°C to -60°C DP | Turnkey Double-Rotor Desiccant System + Sealed Enclosure | Turnkey Dry Room System |
| Next-Gen Solid State & Lithium-Metal R&D | -65°C to -70°C DP | Ultra-Low Dew Point Molecular Sieve Rotor + Deep Subcooling | Desiccant Dehumidifier |
| Electrode Slurry Coating & Solvent Evaporation | ≥99% Solvent Capture | Multistage Closed-Circuit Chilled Condensation Loop | NMP Recovery System |
| Active Pharmaceutical Ingredients (API) & Gelatin | 10% to 25% RH | Silica Honeycomb Rotor with Hygienic Stainless AHU Casework | Desiccant Dehumidifier |
| Defense & Munitions Long-Term Preservation | ≤35% to 40% RH | Mil-Standard Desiccant Unit with Integrated Desorption | Industrial Defense Unit |
| Raw Material Bulk Storage & Preliminary Chilling | 45% to 60% RH | Direct Expansion (DX) Refrigerative Condensation | Refrigerative Dehumidifier |
| Volatile Chemical Loading & Stack Emissions | <20 mg/Nm³ VOC | Cryogenic Condensation + Regenerative Thermal Oxidation (RTO) | VOC Abatement System |
Hangzhou DryAir’s technological stability is proven not merely in test labs, but across hundreds of gigawatt-hours of cell production lines globally.
Long-term environmental engineering partner to global market drivers including CATL, BYD, ATL, EVE Energy, SVOLT, Farasis, and Envision AESC. Our systems sustain continuous automated uptime during mass assembly.
Direct supply contracts completed for global advanced manufacturing giants including Tesla, Northvolt, and TTI, fulfilling rigorous site acceptance tests (SAT) and local trade compliance protocols.
All exported machinery can be tailored with full CE marking, UL 1995/60335 compliance, CSA Canadian safety validation, ASME pressure vessel coding, and EAC customs certification for frictionless international installation.
The industrial dehumidification sector is moving rapidly toward intelligent microclimate management. Hangzhou DryAir is pioneering dynamic control architectures to optimize heavy energy profiles.
Traditional systems run at static full-load reactivation. Our next-generation controllers integrate predictive algorithms correlating external weather forecasts with internal personnel occupancy patterns, modulating regeneration fan speeds and thermal input to trim parasitic power loads by 18-24%.
Collaborating with tier-1 materials laboratories, DryAir is deploying metal-organic framework (MOF) impregnated honeycomb rotors. These advanced media achieve desorption temperatures below 85°C (compared to 130°C+ for conventional silica gel), facilitating full operation on industrial low-grade waste steam.
Direct edge-gateway connections stream rotor pressure drop (ΔP), seal degradation velocity, and compressor thermal dynamics to our global cloud, triggering preventive maintenance alerts well before a rotor failure compromises dry room dew points.
From initial moisture load modeling to overseas cleanroom validation, Hangzhou DryAir retains single-source accountability.
Exhaustive evaluation of process envelope: air-infiltration rates, doorway cycling, internal operator count, latent personnel moisture emissions, and target operational dew point tolerances.
CAD/BIM airflow layout, selection of primary and secondary rotor sizes, face velocity tuning, piping schematics, duct pressure calculation, and comprehensive energy balance modeling.
In-house CNC machining, insulation panel assembly, sealing gasket installation, PLC integration, and mandatory testing inside the climatic chamber prior to overseas shipping containers.
DryAir field engineers supervise enclosure erection, duct sealing, electrical terminations, sensor calibrations, leak-tight smoke tests, and final dew point pull-down validation.
Lifetime access to direct technical teams, guaranteed factory spare parts supply, remote IoT monitoring, and optional 2-year overseas warranty extensions for peace of mind.
Direct engineering responses to key queries submitted by procurement teams, MEP consultants, and plant engineering heads.
Shortlist systems engineered directly by Hangzhou DryAir. Direct factory technical support and turnkey EPC project pricing available.
DHU Series
High-efficiency honeycomb runner system offering multi-zone reactivation and automated constant dew point regulation.
View Specifications
Full EPC
Airtight cleanroom envelopes with integrated deep dehumidifiers designed to sustain -50°C to -70°C dew point zones.
Explore Turnkey Dry Rooms
ZJRH Series
Proven solvent recovery architecture exceeding 99% efficiency for industrial battery electrode drying ovens.
Inquire NMP System
JEN Series
Deep chilling condensation paired with RTO equipment for ultra-clean exhaust compliance in chemical processing.
Review VOC System
Standard DX
Cost-effective mechanical moisture removal for warehouses, seed preservation, and pharmaceutical primary areas.
Check Refrigerative Units GJB Standard
Reinforced environmental systems designed to prevent corrosion of critical avionics and sensitive defense stores.
Defense Specifications cGMP Grade
Hygienic double-skin stainless-steel casings providing sterile, low-humidity air streams for sensitive drug compounding.
Review GMP Models Petro Recovery
Safe condensation and vapor capture technology deployed for terminal storage tanks and hydrocarbon transport racks.
Vapor Recovery DetailsSubmit your process square footage, target dew point requirements, and ambient baseline. Our senior thermodynamic engineers respond within 24 business hours with preliminary psychrometric load curves.