
Top VOC Abatement & Environmental Systems (Direct Factory Export)
Explore our heavy-duty industrial emission mitigation and solvent extraction lines. Built with high-purity zeolite concentration rotors, multi-bed regenerative thermal oxidizers (RTO), and closed-loop condensation modules.
 Cooling + RTO
VOC Abatement System (JEN Series)
Integrated deep-cooling condensation combined with regenerative thermal oxidizers to scrub toxic solvent exhaust down to strict local baseline limits.
Learn More ≥99% Recovery
NMP Solvent Recovery System (ZJRH)
Captures concentrated N-Methyl-2-pyrrolidone from lithium battery electrode drying lines, achieving pristine feedstock recycling and emissions elimination.
Learn More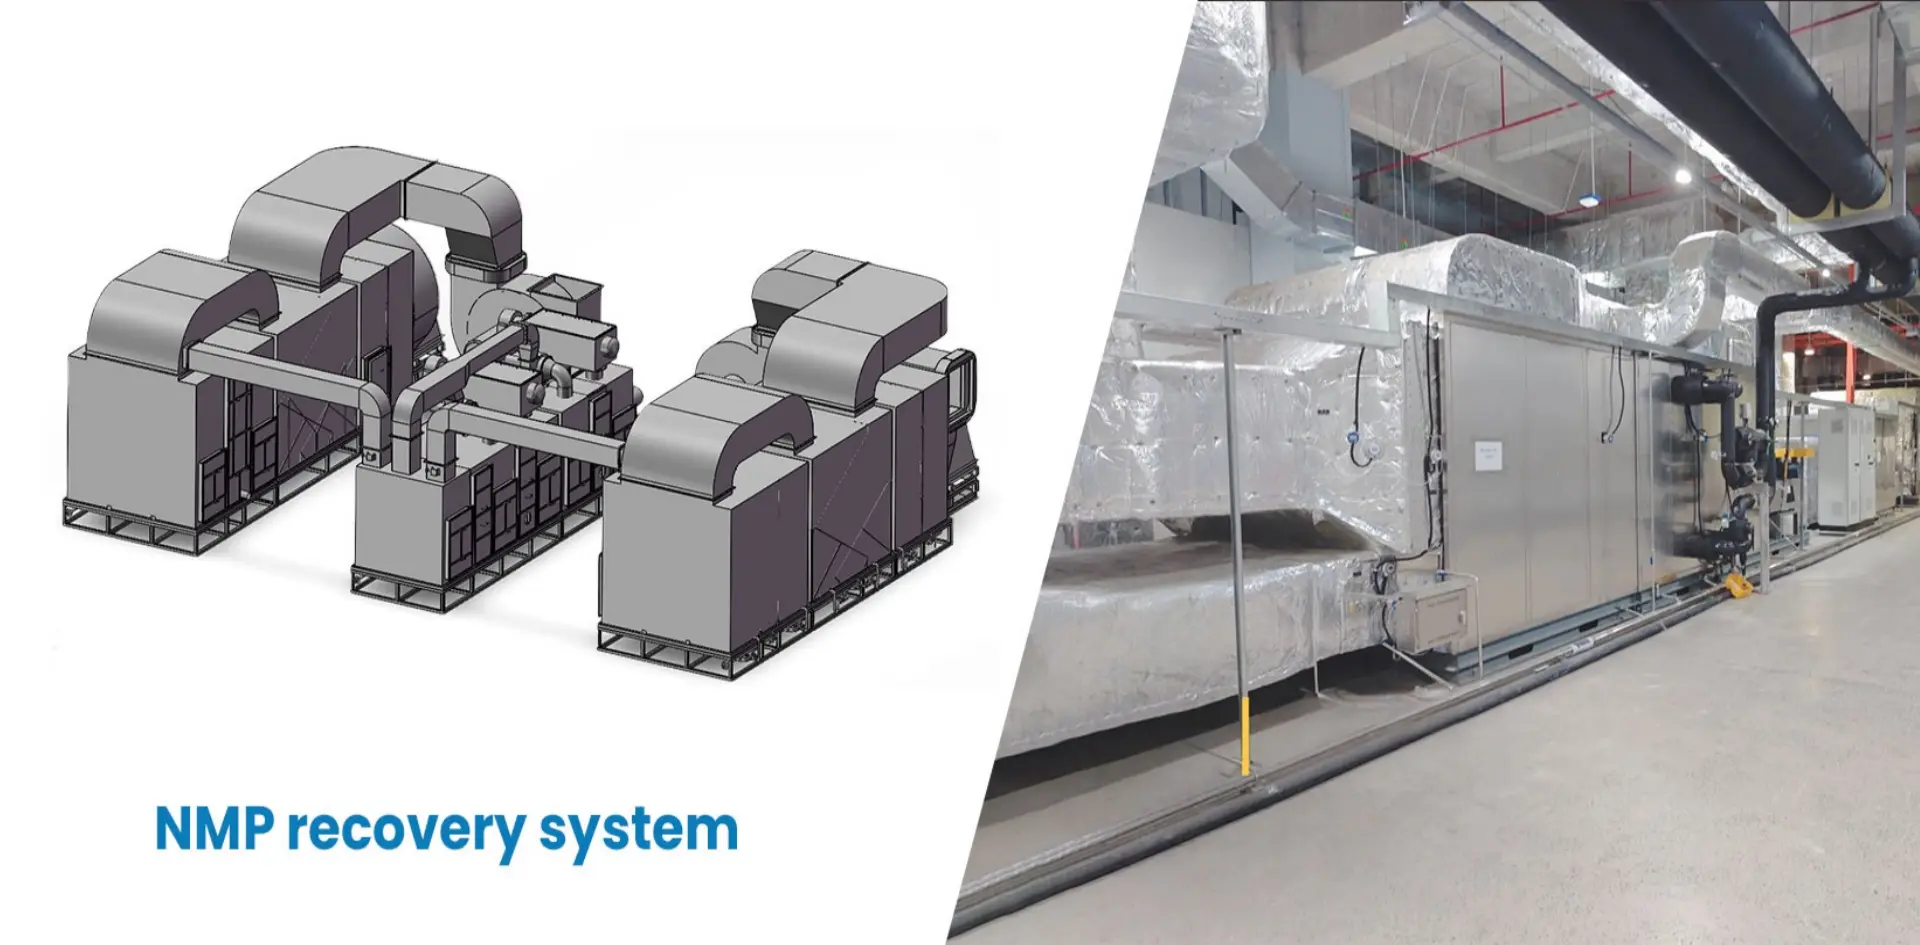 High Airflow
Zeolite Rotor + RTO System
Concentrates high-volume, low-concentration volatile exhausts by up to 25:1 prior to self-sustained oxidation, slashing plant operating fuel spend.
Learn More Petrochemical
Oil & Gas Vapor Condensation Unit
Specialized refrigerated separation system recovering hydrocarbons during volatile liquid transfers, tank terminal storage, and rail loadout points.
Learn More DP -70°C
Rotary Desiccant Dehumidifier (DHU)
High-efficiency desiccant wheel conditioning systems operating in tandem with VOC abatement to guarantee ultra-dry, contaminant-free process air.
Learn More EPC Turnkey
Turnkey Cleanroom & Dry Room
Integrated envelope enclosures and HVAC scrubbing systems designed to maintain positive pressure, zero air leakage, and complete volatile control.
Learn More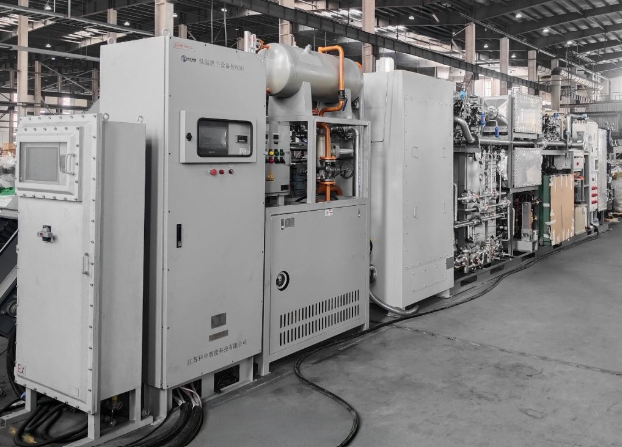 Coating Line
Continuous Coating Line NMP Unit
Equipped with dual cascade chillers and dynamic condensation scrubbing to preserve up to 99% recovered solvent for in-house distillation re-use.
Learn More Pre-Cooling
Industrial Refrigerative Pre-Chiller
Pre-treatment moisture removal modules that stabilize incoming gas temperature and moisture content before volatile concentration stages.
Learn MoreThe Global Industrial Reality: Decarbonization Meets Stringent VOC Control
Industrial manufacturing landscapes across North America, Europe, and Asia-Pacific face an unprecedented regulatory pinch: volatile organic compound emission limits have tightened below 20 mg/Nm³ while corporate net-zero commitments require drastically lower thermal energy consumption.
Escalating Operational Expenditures (OPEX)
Traditional direct thermal oxidizers (TO) and legacy non-regenerative carbon adsorption beds incur staggering recurring costs. Natural gas consumption for raw oxidizer burners can account for 35% of an industrial plant's thermal budget. Modern engineering demands self-sustaining autothermal VOC oxidation and solvent monetization.
- Thermal efficiency requirement ≥ 95% across regenerators
- Adsorption-concentration ratios exceeding 20:1
- Secondary heat recovery for steam and central hot water
Severe Environmental Enforcement Regimes
Enforcement bodies—such as the US EPA (under 40 CFR Part 60 and 63 NESHAP), the European Union (under the Industrial Emissions Directive 2010/75/EU), and China's Ministry of Ecology and Environment—have imposed strict continuous emission monitoring (CEMS) protocols with zero tolerance for fugitives.
- Total VOC (TVOC) limits routinely mandated below 20 mg/Nm³
- Hazardous Air Pollutant (HAP) destruction standards ≥ 99%
- Continuous automatic recording and direct telemetry to regulators
Gigafactory Solvent Reclamation Demands
The explosive rollout of electric vehicle (EV) battery manufacturing demands tens of thousands of metric tons of N-Methyl-2-pyrrolidone (NMP). Treating NMP simply as waste is commercially unfeasible; plants must implement closed-loop systems that condense and reclaim virgin-grade solvent directly on-site.
- Solvent recovery efficiency benchmarked at ≥ 99.0%
- Closed-loop hot gas recycling back to dry room ovens
- Dramatic reduction of Scope 1 and Scope 3 lifecycle carbon
Localized Heavy-Industry Application Scenarios
DryAir tailors VOC abatement and solvent capture platforms around the physical characteristics of process streams: temperature, latent humidity, solvent flashpoints, Lower Explosive Limits (LEL), and continuous mass flow rates.
| Industrial Sector | Typical Process Off-Gas Profile | Primary VOC Species | Engineered Abatement Architecture | Guaranteed Discharge Performance |
|---|---|---|---|---|
| Lithium-ion Battery Manufacturing | High concentration, elevated temperature (80-120°C), low particulates | N-Methyl-2-pyrrolidone (NMP), residual organic solvents | Dual-stage Deep Cooling Condensation + Polishing Zeolite Wheel + Secondary Heat Recovery | NMP Recovery ≥99%; Exhaust NMP <5 mg/Nm³ |
| Semiconductor & Photolithography | Massive volumetric airflow (50,000–250,000 m³/h), low VOC concentration (<300 ppm) | PGMEA, Isopropanol (IPA), Acetone, Cyclohexanone | High-Hydrophobic Zeolite Concentrator Rotor (20:1 ratio) + 3-Bed Regenerative Thermal Oxidizer | TVOC Destruction ≥99.2%; NMHC <10 mg/Nm³ |
| Pharmaceutical Chemical Synthesis | Variable flow, batch release, high humidity, corrosive acid vapor presence | Dichloromethane (DCM), Methanol, Ethanol, Toluene, Acetone | Hastelloy/SS316 Acid Scrubber + Chilled Condensation + Catalytic/Thermal Oxidation | Removal Efficiency ≥98.5%; Tail-gas compliance with FDA/GMP |
| Automotive OEM & Aerospace Coating | High air volume, fluctuating booth exhaust, presence of mist and overspray | Xylene, Toluene, Ethylbenzene, Butyl Acetate, MEK | Multi-stage Dry Bag Filter + Rotary Zeolite Concentrator + Flameless Thermal Oxidation | Non-methane hydrocarbon (NMHC) <20 mg/Nm³ |
| Petrochemical Terminals & Storage | Intermittent surge loads during tanker loading, high hydrocarbon saturation | Gasoline vapors, Benzene, Toluene, Light fractions (C4–C9) | Explosion-proof Cryogenic Condensation Recovery Unit (CRU) + Adsorption Polishing | Recovery rate ≥97%; Vent concentration <10 g/m³ |
Deep-Dive Technical Roadmap: Matching Chemistry with Thermodynamics
Selecting the correct VOC abatement pathway prevents disastrous catalytic poisoning, bed fires, and excessive utility consumption. DryAir integrates four distinct core architectures into its international turnkey export packages.
Multi-Bed RTO Systems
Utilizes structured honeycomb ceramic beds to absorb and release combustion heat. By alternating flow directions across 3 or 5 ceramic chambers, thermal energy recovery exceeds 95%–97%.
- Combustion chamber: 760°C to 850°C
- Zero gas bypass with pneumatic poppet valves
- Autothermal operation at >1.5 g/Nm³ VOC
Zeolite Rotary Concentrators
Continuous rotary wheel impregnated with high-silica hydrophobic molecular sieves. Adsorbs trace solvents from vast airflow, which are then desorbed using small volumes of hot air.
- Concentration multiplication: 10:1 to 30:1
- Incombustible honeycomb substrate
- Low pressure drop (<1000 Pa)
Deep-Cooling Condensation
Employs cascading refrigeration chillers (-20°C to -75°C) to lower volatile vapor pressure below saturation points, converting VOC vapors directly into high-purity liquid for re-use.
- Primary choice for NMP, DCM, Pentane
- Intrinsic explosion prevention
- Payback through recovered solvent credits
Catalytic Oxidizers (CO/RCO)
Precious metal catalysts (Pt/Pd on ceramic monoliths) allow VOC oxidation at low temperatures (280°C–400°C), drastically curtailing NOx emissions and fuel consumption.
- Ideal for clean solvent streams without sulfur/silicon
- Lower thermal stress on steel structures
- Substantially smaller installation footprint
China Factory Precision: Hangzhou DryAir Supply Chain Dominance
In mega-infrastructure and gigafactory delivery, engineering design is only as good as the execution supply chain. Operating from our advanced facility in Qingshan Industrial Park, Lin'an, Hangzhou, DryAir leverages China's industrial clustering to provide unmatched delivery velocity, quality control, and cost governance.
End-to-End Vertical Integration
Unlike Western equipment integrators who outsource core sheet metal, heat exchanger coils, and piping sub-assemblies to multiple fragmented tiers, DryAir executes laser cutting, structural frame welding, CNC stamping, coil fabrication, and pneumatic valve integration inside our proprietary factory.
- Strict metallurgy verification (SS304, SS316L, 2205 Duplex)
- In-house high-temperature painting and thermal insulation baking
- Independent test stations for rotary wheel sealing leak rates
Accelerated Lead Times & Modular Skids
Western supply chains frequently require 12 to 18 months for multi-bed RTO or solvent recovery skids. DryAir achieves FAT (Factory Acceptance Test) readiness in 12 to 20 weeks through high-density automation, lean inventory of critical blowers, burners, and PLC components, and modular skid packaging.
- Standardized modular block shipping containers
- Pre-wired, pre-piped plug-and-play assembly logic
- On-site commissioning time compressed by up to 50%
Battle-Tested in Mega-Gigafactories
Our solutions have not merely succeeded in laboratory pilots; they have been validated under continuous 24/7 manufacturing loads by industry leaders including CATL, ATL, BYD, EVE Energy, Farasis, Envision, SVOLT, and internationally for Tesla, Northvolt, and TTI.
- Proven zero-downtime reliability over millions of operational hours
- Rugged design resistant to solvent surges and temperature spikes
- Continuous feedback loop from field operational engineers
Localized Support & Compliance Assurance Worldwide
Exporting complex industrial environmental equipment requires meticulous adherence to recipient-state occupational, mechanical, and explosive safety statutes. DryAir provides turnkey regulatory security from engineering sign-off to local field validation.
Explosion Safety (ATEX, NFPA 69, NEC 500)
Treating concentrated volatile streams involves acute explosion hazards. DryAir builds every VOC skid according to rigorous regional safety codes: ATEX Zone 1/Zone 2 for the EU, NFPA 69 / NEC 500 Class I, Div 1/2 for North America.
- Continuous dual LEL sensor loops with automated nitrogen purging
- Explosion venting panels and flame arresters certified to ISO 16852
- Intrinsically safe instrumentation and explosion-proof variable drives
Global Certification Passport
Our plants are qualified under ISO 9001 and China's stringent GJB national military standard quality system. Units leaving our export bays arrive pre-certified for target jurisdictions without requiring expensive field retrofits.
- European Union: CE Marking (Machinery, Low Voltage, EMC, PED)
- North America: UL 508A electrical control panels, CSA, ASME pressure vessels
- Eurasia: EAC conformity for customs union import
Localized Field Service & 2-Year Assurance
Through our dedicated Global Service architecture, DryAir eliminates the operational anxiety of overseas sourcing. We deploy commissioning teams directly to customer job sites across Europe, Southeast Asia, and the Americas.
- Optional comprehensive 2-Year Overseas Service & Parts Warranty
- 24/7 Remote IoT diagnostics, telemetry monitoring, and firmware patching
- Direct local engineering dispatch for scheduled CEMS calibrations
Future Outlook: Next-Generation Smart Abatement (2025–2030)
The convergence of industrial IoT, predictive neural networks, and stringent carbon border adjustment mechanisms (such as EU CBAM) is reshaping industrial emissions infrastructure into an intelligent, energy-positive utility.
Phase 1: AI-Driven Dynamic Predictive LEL Control
Integration of ultra-fast infrared laser absorption sensors with adaptive machine learning algorithms. Instead of reacting to solvent spikes, the PLC anticipates concentration pulses from coater lines, preemptively modulating wheel rotation speeds and dilution dampers to eliminate safety trips while minimizing supplementary natural gas injection.
Phase 2: Ultra-Low NOx & Zero Methane Slip Combustion
Development of flameless porous ceramic matrix burners coupled with hydrogen-enriched fuel compatibility. Modern DryAir RTOs are engineered ready for transition to 20%+ hydrogen co-firing, curtailing stack NOx to below 15 mg/Nm³ while completely preventing methane slip into the upper atmosphere.
Phase 3: Thermal-Dehumidification Energy Cross-Coupling
Directly capturing superheated exhaust energy from RTO oxidation chambers (discharging at 120°C–180°C) and channeling it via high-efficiency thermal oil or plate exchangers into the desiccant rotor regeneration sector of the plant's -70°C dew point dry rooms. This eliminates independent regeneration heaters and slashes overall factory electricity demand by 30%.
Frequently Asked Questions on VOC Abatement Projects
Detailed engineering answers to the real-world operational, safety, and logistical questions raised by global EPC contractors, plant directors, and environmental health & safety (EHS) professionals.
How does DryAir ensure safety when handling high concentrations of explosive solvents?
Every system integrates fail-safe multi-tier interlocks per NFPA 69 and EN 12753 standards. We install dual optical or infrared Lower Explosive Limit (LEL) analyzers upstream. If off-gas concentration rises above 25% LEL, automatic high-speed dilution air dampers open instantly. If levels touch 40% LEL, the process stream is safely diverted to an emergency bypass stack while the oxidizer chamber is automatically flooded with inert nitrogen purging.
What is the minimum VOC concentration required for an RTO to run autothermally?
Due to the high thermal efficiency of our 3-bed structured ceramic media (≥ 95% thermal recovery), an off-gas containing approximately 1.5 g/Nm³ of mixed solvents (equivalent to roughly 3%–4% LEL for typical aliphatic and aromatic hydrocarbons) is sufficient to maintain an 800°C combustion chamber temperature without requiring any auxiliary natural gas burner support after initial warm-up.
How does the zeolite rotor perform in high-humidity ambient environments?
Standard activated carbon adsorbers experience rapid saturation and collapse when relative humidity exceeds 60%. In contrast, DryAir deploys high-silica, hydrophobic crystalline zeolite molecular sieves. The hydrophobic crystal structure selectively bonds with non-polar and polar organic volatile molecules while rejecting water vapor, maintaining steady concentration efficiency even at humidity levels up to 80%–85% RH.
What solvent purity can be recovered from an NMP coating line?
Our ZJRH continuous multi-stage deep-cooling condensation recovery systems condense NMP down from coater gas streams, yielding raw reclaimed liquid with an NMP concentration typically between 80% and 85% (the remainder consisting of extracted moisture). This reclaimed liquor is directly routed into plant distillation columns to produce battery-grade NMP with purity ≥ 99.8%, ready for slurry re-mixing.
How are units packaged to prevent damage during long ocean freight transit?
All international export skids are built on heavy-duty structural channel steel frames with certified container corner castings or lifting lugs. Critical ceramic media beds and zeolite wheels are locked with anti-vibration transit bracing. Electrical panels are vacuum-sealed with silica desiccant bags, wrapped in vapor-barrier foil, and crated in fumigated export-grade plywood certified to ISPM 15 standards.
Can DryAir assist with local environmental permit filings in North America or Europe?
Yes. DryAir provides complete engineering data packages including mass balance sheets, P&ID schematics, stack dispersion calculations, thermal energy consumption curves, and continuous emission profiles stamped by our licensed HVAC and environmental engineers to expedite local Air Quality Management District (AQMD) or European national EPA operating permit approvals.
Full Environmental & Humidity Control Product Lines
Select your equipment configuration below to submit an inquiry or view full engineering specifications directly from Hangzhou DryAir Treatment Co., Ltd.
JEN Line
Industrial VOC Abatement Plants
High-capacity thermal oxidation and condensation skids engineered for demanding industrial solvent emission points.
View System Specifications
ZJRH Series
High-Efficiency NMP Recovery Systems
Closed-loop, continuous electrode solvent condensing skids yielding ≥99% NMP collection efficiency.
View System Specifications
DHU Line
Rotary Desiccant Dehumidifiers
Industrial rotary desiccant systems capable of driving supply air down to -70°C dew point for critical cleanrooms.
View System Specifications
EPC Package
Turnkey Gigafactory Dry Room Systems
Single-source EPC design, structural envelope installation, HVAC dehumidification, and performance validation.
View System Specifications
Refrigeration
Industrial Refrigerative Dehumidifiers
High-efficiency mechanical refrigeration drying units for general warehouses, workshops, and pre-cooling stages.
View System Specifications
Autothermal
Zeolite Concentrator + RTO Packages
Proven large-volume VOC scrubbing solutions with up to 97% heat self-sufficiency and low operating footprint.
View System Specifications
Explosion Proof
Petrochemical Vapor Condensation Skids
Hydrocarbon gas capture units for fuel distribution, refinery loadout gantries, and chemical tank terminals.
View System Specifications
Modular Design
Continuous Coating Line Recovery Modules
Engineered for high throughput electrode coaters with zero volatile leakage and maximum thermal economy.
View System Specifications