
 DP -70°C Control
DHU Desiccant Dehumidifier
Ultra-low dew point dual-rotor engineering delivering continuous atmospheric moisture scavenging for high-precision battery dry rooms.
Continuous industrial-grade dehumidification and closed-loop environmental solutions deployed in high-spec automated manufacturing hubs globally.
DP -70°C Control
Ultra-low dew point dual-rotor engineering delivering continuous atmospheric moisture scavenging for high-precision battery dry rooms.
 Turnkey EPC
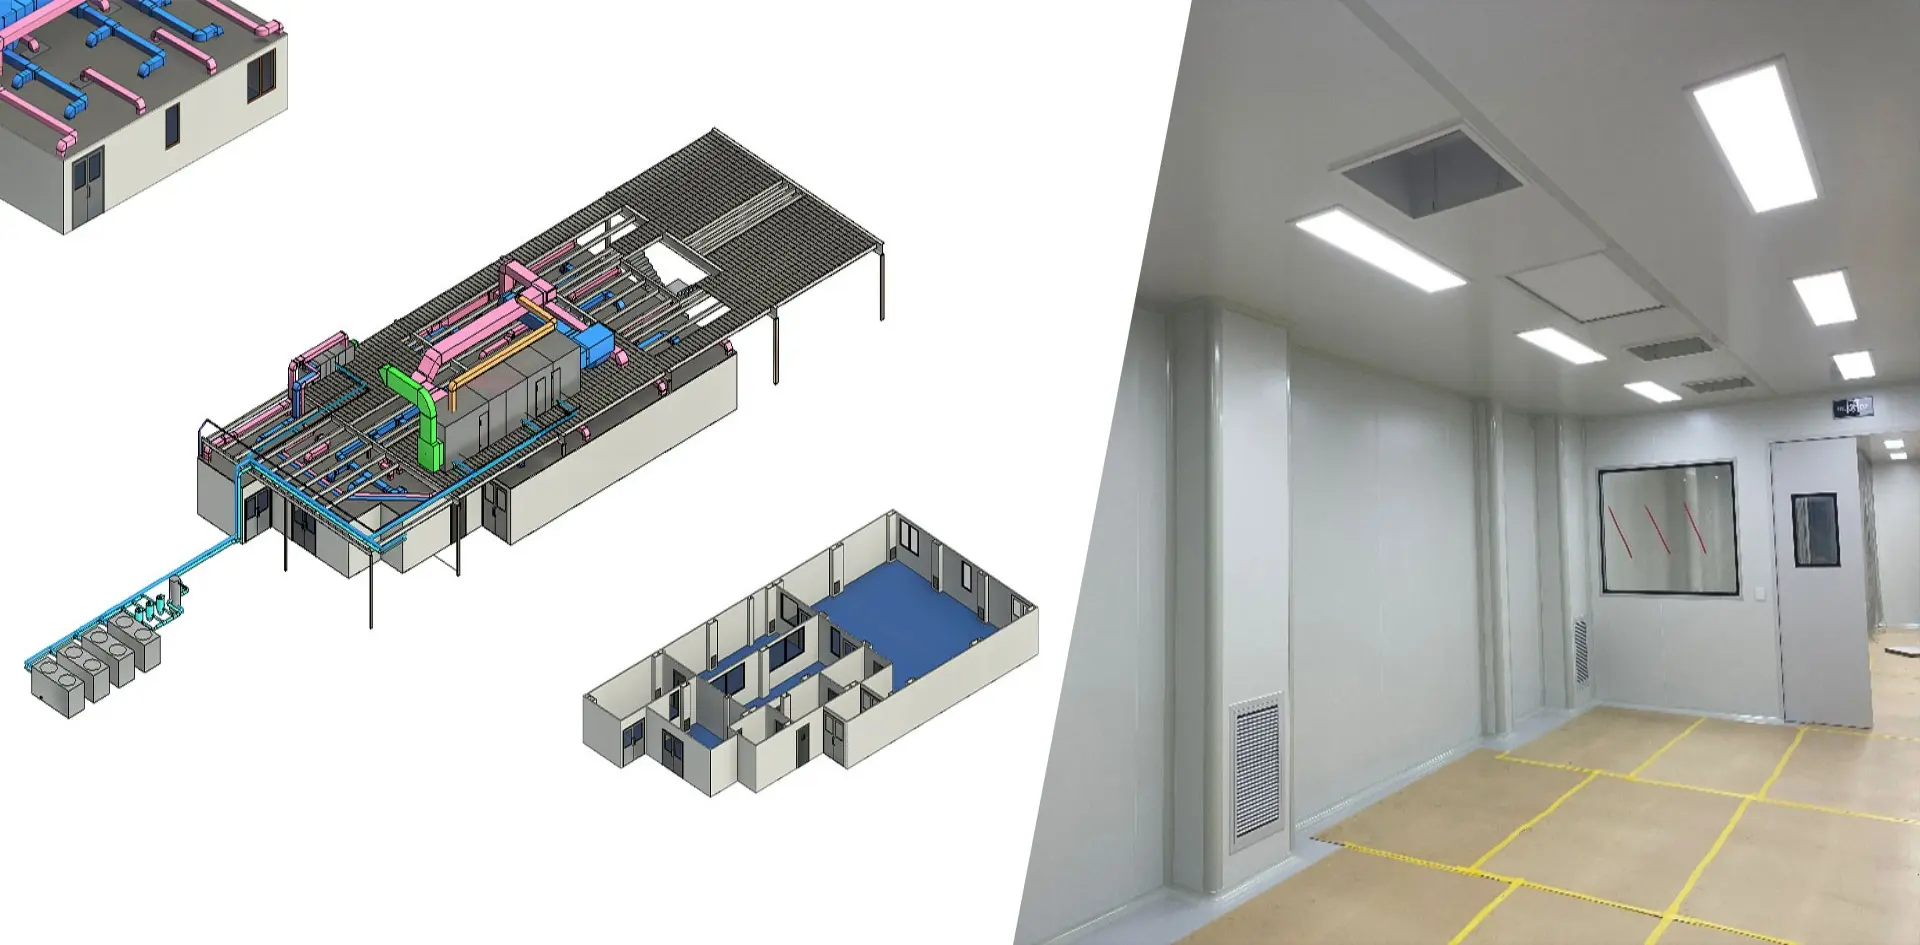
End-to-end controlled atmospheric enclosure with integrated AHU, air filtration, hermetic wall seals, and multi-stage dehumidification validation.
 ≥99% Efficiency
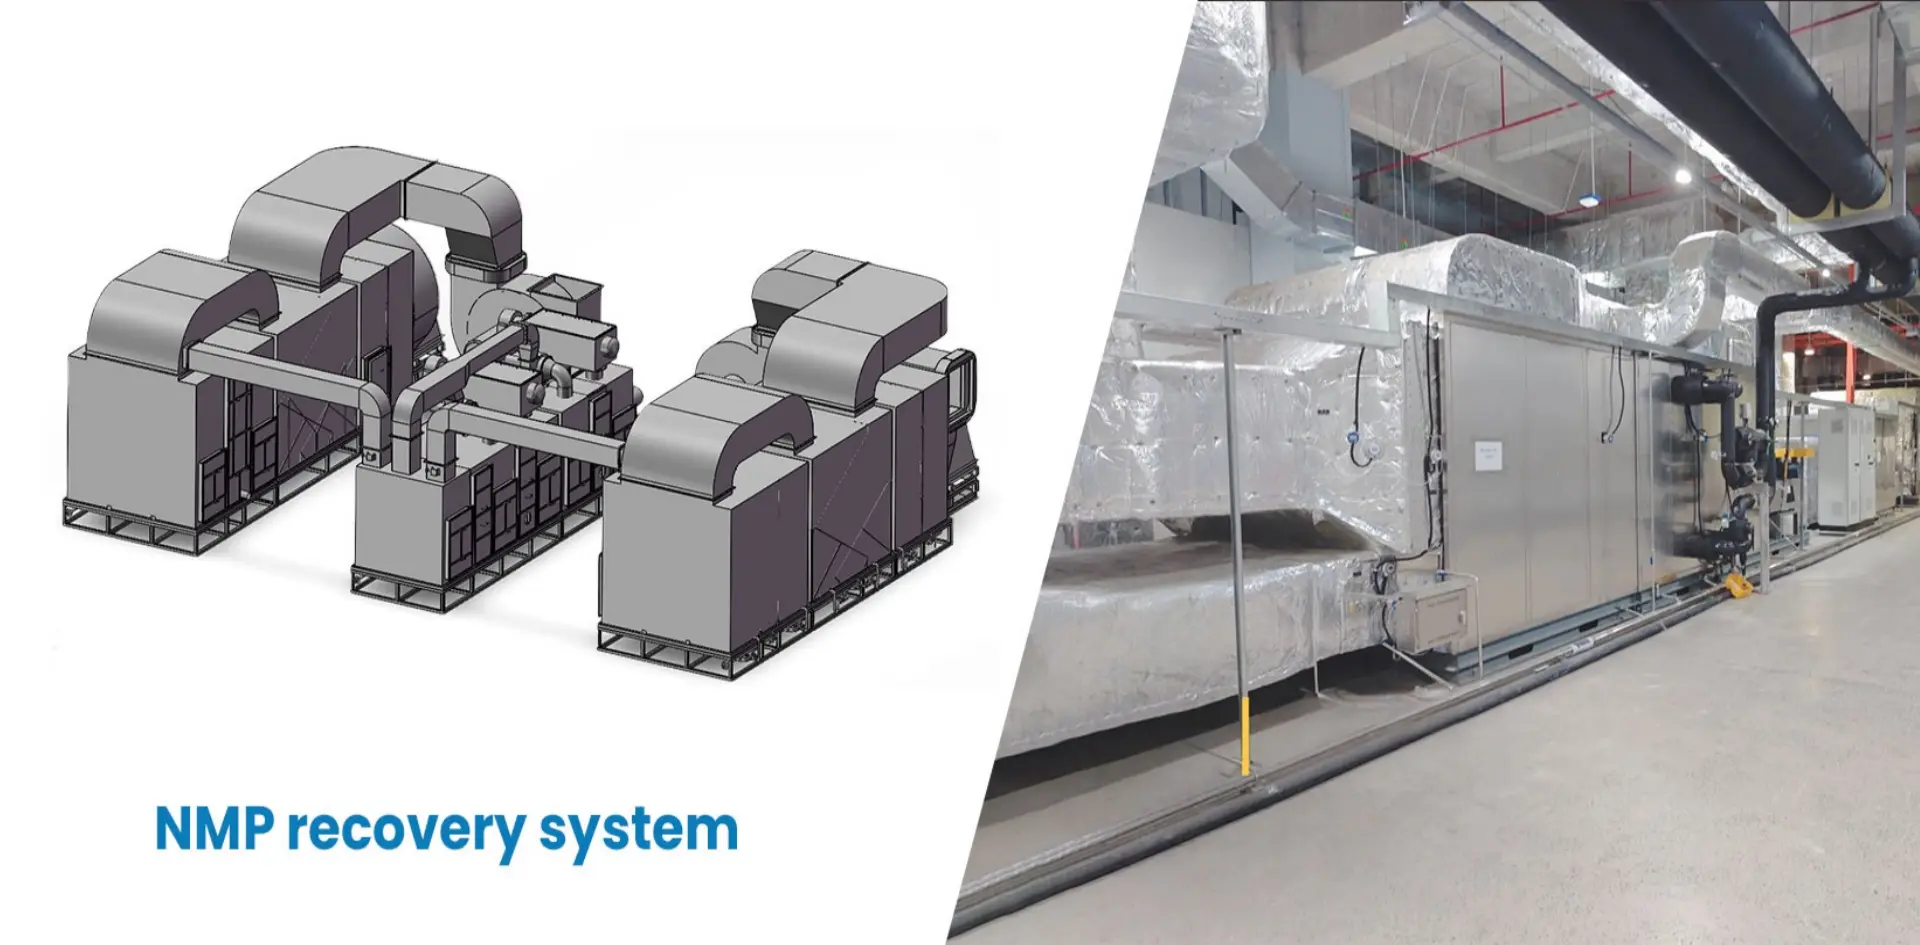
Recovers volatile N-Methyl-2-pyrrolidone solvent from electrode coating ovens, drastically lowering VOC operational liabilities and recycling materials.
 Cooling + RTO
Cryogenic deep-cooling condensation combined with regenerative thermal oxidizer modules to scrub exhaust streams down to stringent limits.
 High COP
High-efficiency mechanical condensation systems optimized for pre-cooling stages, logistics warehousing, and baseline moisture reduction.
 Gigafactory Grade
Engineered for electrolyte filling and sealing zones requiring class 10,000 cleanroom performance matched with continuous dew point stability.
 Purity >99.5%
Thermal condensation units tailored for cathode slurrying lines, yielding reclaimed grade solvent without secondary environmental processing fees.
 Zeolite Rotor
High-volume, low-concentration exhaust gas treatment utilizing hydrophobic synthetic zeolite wheels with thermal catalytic oxidizers.
Hangzhou DryAir Treatment Co., Ltd. analyzes the thermodynamics of moisture capture, solid desiccant sorption matrices, and life-cycle operational expenditure in high-precision processing.
Unlike mechanical refrigeration that reaches saturation limits at ~4°C to prevent coil frost, our synthesized silica gel and molecular sieve corrugated rotors directly adsorb water molecules through microscopic capillary condensation, achieving supply air dew points down to -70°C reliably across 24/7 operating cycles.
Moisture removal is continuous: the rotor rotates slowly between process and reactivation sectors. Low-temperature reactivation air or direct-fired gas modules drive vapor off the desiccant beds. Advanced heat exchangers recycle waste heat from condensation or plant steam, slashing HVAC parasitic power by up to 35%.
Ultra-low dew points fail if air bypasses desiccant wheels. DryAir integrates proprietary high-temperature perimeter and radial seals designed with dynamic self-tensioning springs, eliminating cross-contamination between reactivation air and process supply streams under negative differential static pressures.
Targeted industrial engineering engineered around the material chemistry and yield thresholds of regulated manufacturing.
Exposure of active cathode materials (such as NMC/LFP) and non-aqueous electrolytes to ambient water vapor creates hydrofluoric acid (HF), leading to capacity fading, internal short circuits, and pack fires. DryAir systems maintain electrolyte filling, vacuum sealing, and formation dry rooms between -40°C and -70°C dew point.
Hygroscopic compounds, effervescent tablets, diagnostic test strips, and soft gelatin capsules lose structural stability or degrade chemically under unstable humidity. Our systems safeguard cGMP production suites, tablet coating pans, and fluid bed dryers at precise 10% to 25% RH levels.
Manufactured strictly according to the GJB national military standard, DryAir units control unheated warehouses, missile guidance calibration centers, and radar bays, inhibiting electrochemical corrosion on avionics, explosive charges, and precision alloy armaments below 40% RH indefinitely.
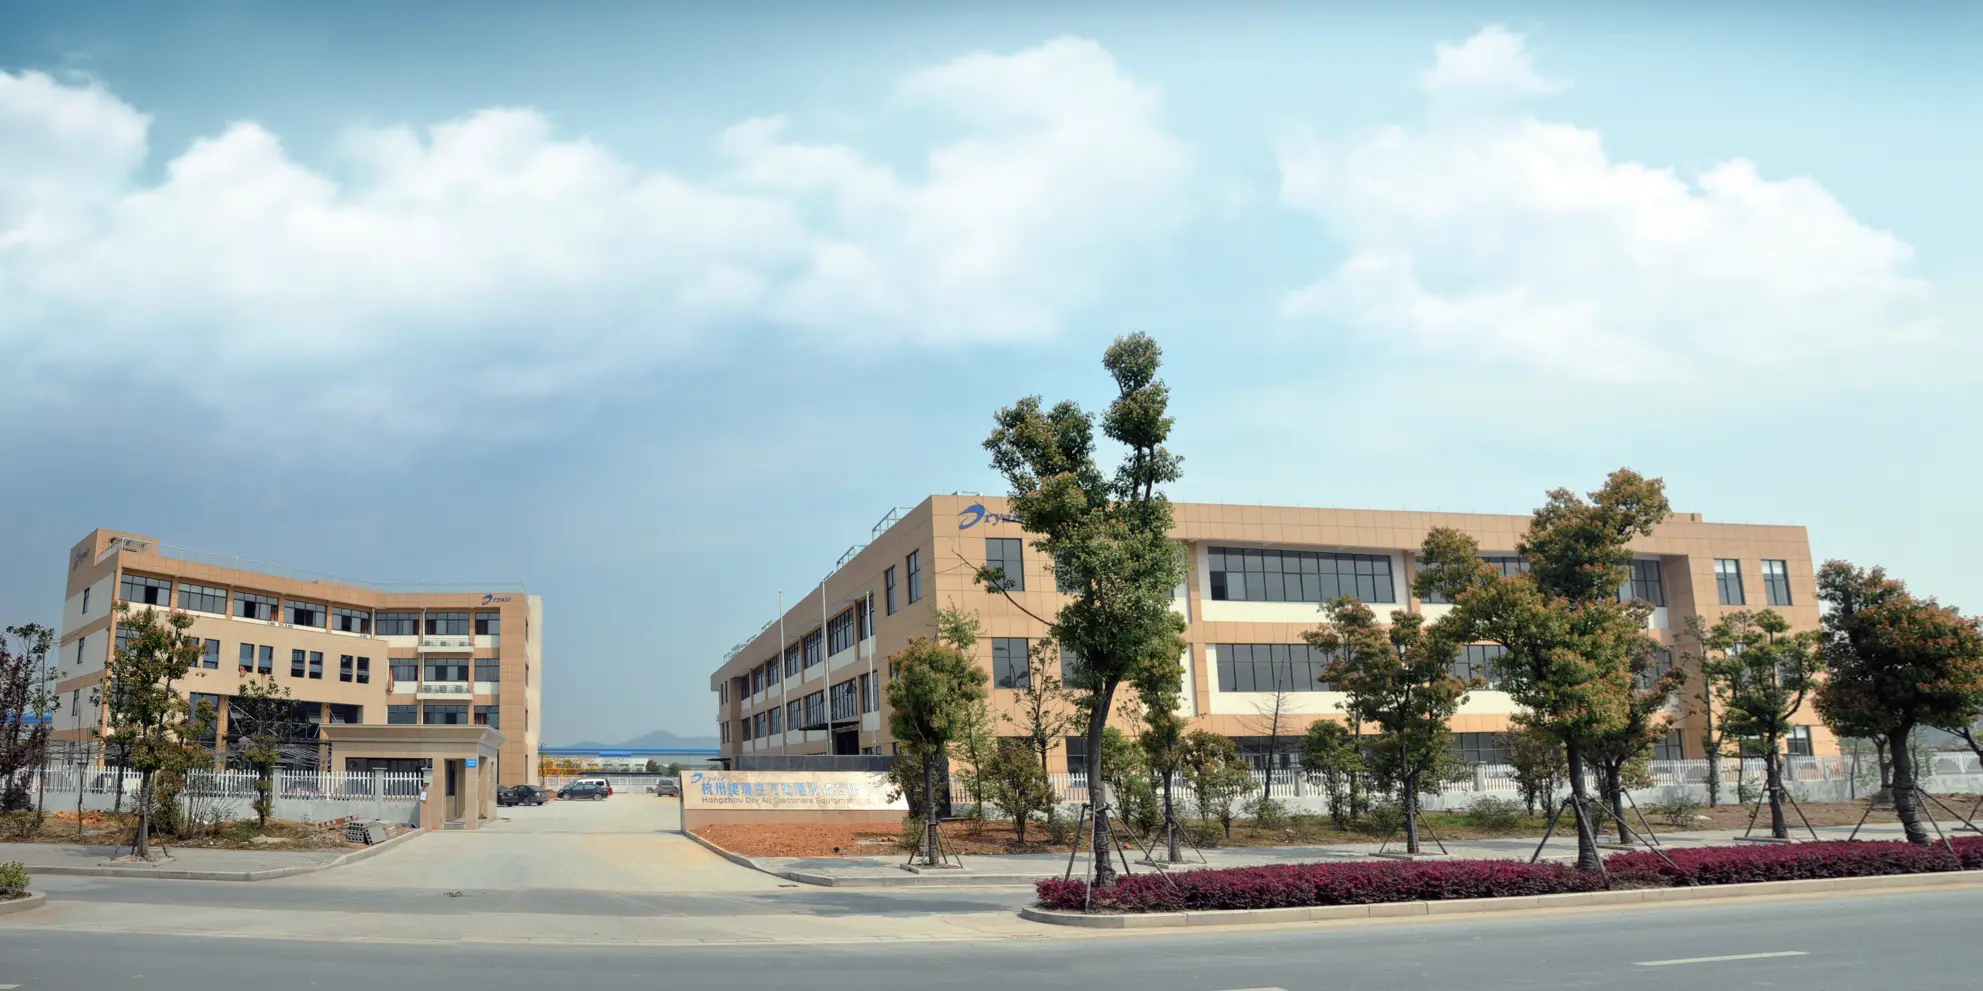
Operating from the Qingshan Industrial Park in Hangzhou, DryAir leverages deep industrial cluster integration to compress project lead times and guarantee high quality.
While European and American suppliers experience extended 24–40 week backlogs, our vertical fabrication facility produces over 200 large-tonnage units monthly, matching rapid gigafactory buildouts.
From high-temperature silicon seals and customized titanium-alloy fans to PLC automation suites (Siemens, Schneider, Allen-Bradley), our multi-sourced supply chain mitigates single-source operational vulnerabilities.
Every unit undergoes strict psychrometric chamber testing before export. We simulate tropical 40°C / 95% RH ambient inlet conditions to guarantee performance at target dew points prior to leaving the facility floor.
Our research and operational footprint includes 6 staff with Master's or PhD degrees, 2 national registered HVAC engineers, 8 senior engineers, and 58 specialized technicians managing quality across all units.
Accurate psychrometric specification prevents over-engineering Capex while eliminating moisture contamination risks during line ramp-up.
| Application & Industrial Process | Target Moisture / Emission Spec | System Architecture Recommendation | Primary Energy / Regeneration Vector |
|---|---|---|---|
| Lithium Battery Cell Assembly & Electrolyte Filling | -40°C to -60°C Dew Point | Turn-key Integrated Dry Room System (DHU + Hermetic Enclosure) | Direct Steam / Electrical / Gas Thermal Regeneration |
| Solid-State & Next-Gen Lithium Metal Cells | Down to -70°C Dew Point | Multi-Stage Dual Rotor Desiccant Dehumidifier Series | High-Temperature Reactivation with Chilled Glycol Pre-cooling |
| Cathode Electrode Coater Dryer Exhaust | ≥99% NMP Recovery Rate | Closed-Loop Condensation + Zeolite Molecular Scrubber | Deep Cryogenic Glycol Heat Recovery Exchangers |
| Hygroscopic Pharma Powders & Gelatin Blistering | 10% – 30% Relative Humidity | Desiccant Dehumidification Unit with High-Grade HEPA Stages | Hot Water / Steam Heat Recovery Regenerative Coils |
| Military Equipment & Guided Ordnance Storage | ≤40% RH (GJB Compliant) | Modular Stationary Desiccant Environmental Air Purge Unit | Low-Wattage Heat Pump Regeneration Modules |
| Raw Material Bulk Storage & Electronics Warehousing | 45% – 60% Relative Humidity | Industrial Refrigerative Condensation Dehumidifier Units | Direct Expansion R410A / R134a Compressor Heat Rejection |
| Bulk Fuel Terminal & Solvent Exhaust Treatment | Strict EPA / VOC Emission Caps | Deep-Cooling Condensation combined with RTO Incineration | Self-Sustaining Regenerative Thermal Combustion |
Single-source technical responsibility mitigates project interface risks between cleanroom installers, HVAC contractors, and controls providers.
Calculation of sensible heat, internal latent loads from personnel, equipment exfiltration, and building envelope vapor permeation using digital airflow modeling.
3D BIM layout design of rotor casing, fan static matching, chilled water/glycol loops, regenerative thermal systems, and PLC control system schematics.
Sheet metal CNC punching, stainless casing fabrication, rotor installation, wiring integration, and pre-shipment dew point validation in performance test cells.
On-site equipment positioning, duct installation, airtight envelope assembly, balancing, and multi-point moisture load testing under full production loads.
Remote telemetry diagnostics, factory-direct spare desiccant rotor delivery, filter replacements, and optional 2-year overseas technical support agreements.
Leading the transition toward decarbonized dry rooms, waste-heat-driven regeneration matrices, and smart adaptive algorithms.
Traditional systems operate on fixed reactivation setpoints. DryAir is integrating neural network-based predictive control algorithms that monitor ambient weather variations and plant production shifts, dynamic modulating regeneration heaters to achieve 18–22% lower average energy consumption.
Our upcoming generation of desiccant matrices utilizes modified Metal-Organic Frameworks (MOFs) and high-density functional zeolites capable of full desorption regeneration using low-grade industrial waste heat (hot water as low as 65°C–80°C), slashing direct fossil-fuel emissions.
In accordance with the Kigali Amendment and EU F-gas regulations, DryAir is redesigning pre-cooling refrigeration units to use low-GWP refrigerants (R454B, R513A) and natural fluids like CO2 (R744), future-proofing plant operational licenses globally.
International project delivery backed by rigorous electrical, mechanical, and safety certifications for European, North American, and Asian gigafactories.
Fully compliant electrical control panels, dual-voltage power integration, and North American safety listings for fast-track permit validation in US and Canadian industrial corridors.
Full CE certification encompassing Machinery Directive 2006/42/EC, Low Voltage Directive (LVD), and EMC compliance for seamless deployment throughout European Union industrial installations.
Condensers, distillation columns, and heat exchangers built to rigorous ASME Section VIII pressure boundary compliance, ensuring safety on high-pressure VOC and solvent lines.
Certified conforming to the Technical Regulations of the Eurasian Customs Union (TR CU), facilitating rapid customs clearance and operation across member states without field modifications.
In-depth technical answers addressing dew point selection, regeneration efficiencies, international commissioning, and system maintenance.
From single standard dehumidification units to large-scale multi-rotor air management setups for high-throughput production lines.
DHU Series
Continuous moisture extraction engineered to maintain sub-zero dew points across mission-critical cleanrooms and automated packaging environments.
Turn-key Cleanroom
Turnkey environmental solutions integrating hermetic insulated enclosures, air handlers, low-leakage dampers, and precision monitoring arrays.
Solvent Recycling
Recovers volatile N-Methyl-2-pyrrolidone solvent from electrode coating exhaust, cutting raw chemical consumption and operational costs.
RTO Emission Control
Advanced regenerative thermal oxidation combined with cryogenic chilling stages for high-volume, continuous industrial exhaust scrubbers.
Pre-Cooling Stage
Mechanical direct-expansion refrigeration units optimized for warehouse humidity balance and pre-treatment ahead of desiccant wheels.
 Factory Direct
Thermal-break aluminum framework enclosures with double-skin PU insulation panels, preventing external casing condensation in humid climates.
 cGMP Class A/B
Sanitary-grade desiccant air handling units built with internal wash-down designs, microbial filters, and integrated BMS automation networks.
 Global Engineering
Comprehensive multi-megawatt moisture abatement infrastructure for multi-gigawatt cell manufacturing projects worldwide.
Provide your layout specifications, latent moisture loads, and supply target dew points. Our senior HVAC engineering team will return a customized psychrometric mass balance assessment within one business day.