
Food-Grade Desiccant Dehumidification Engineering Systems
Engineered for cleanroom processing, high-volume spray drying, and zero-condensation food storage environments. Select your system specifications below.
 DP -70°C Stable
Desiccant Dehumidifier System
Continuous low-dew-point silica gel rotor technology for food processing hygiene and pharmaceutical grade dry towers.
Product Details → Turnkey EPC
Turn-key Dry Room System
Complete modular enclosures with integrated precision HVAC, HEPA filtration, and ultra-dry envelope design.
Explore Turnkey → Recovery ≥99%
NMP Solvent Recovery System
High-efficiency chemical condensing recovery cutting volatile emissions across continuous industrial drying processes.
View NMP Systems → Deep Cooling + RTO
VOC Abatement System
Cryogenic condensation paired with regenerative thermal oxidizers to ensure strict international clean-air compliance.
VOC Solutions → Hygienic Clean
Sanitary Food Dehumidifier
Built with stainless steel contact surfaces and washable silica rotors compliant with 3-A Sanitary and FDA standards.
Request Specs → Thermal Recovery
Spray Drying Dehumidifier
Pre-conditions inlet process air for gelatin, dairy, and infant formula drying towers without weather dependency.
View Drying Units → Energy Saver
Refrigerative Dehumidifier
High-capacity primary bulk dehumidification for food cold storages, pre-cooling air handling, and raw warehouses.
Inquire Models →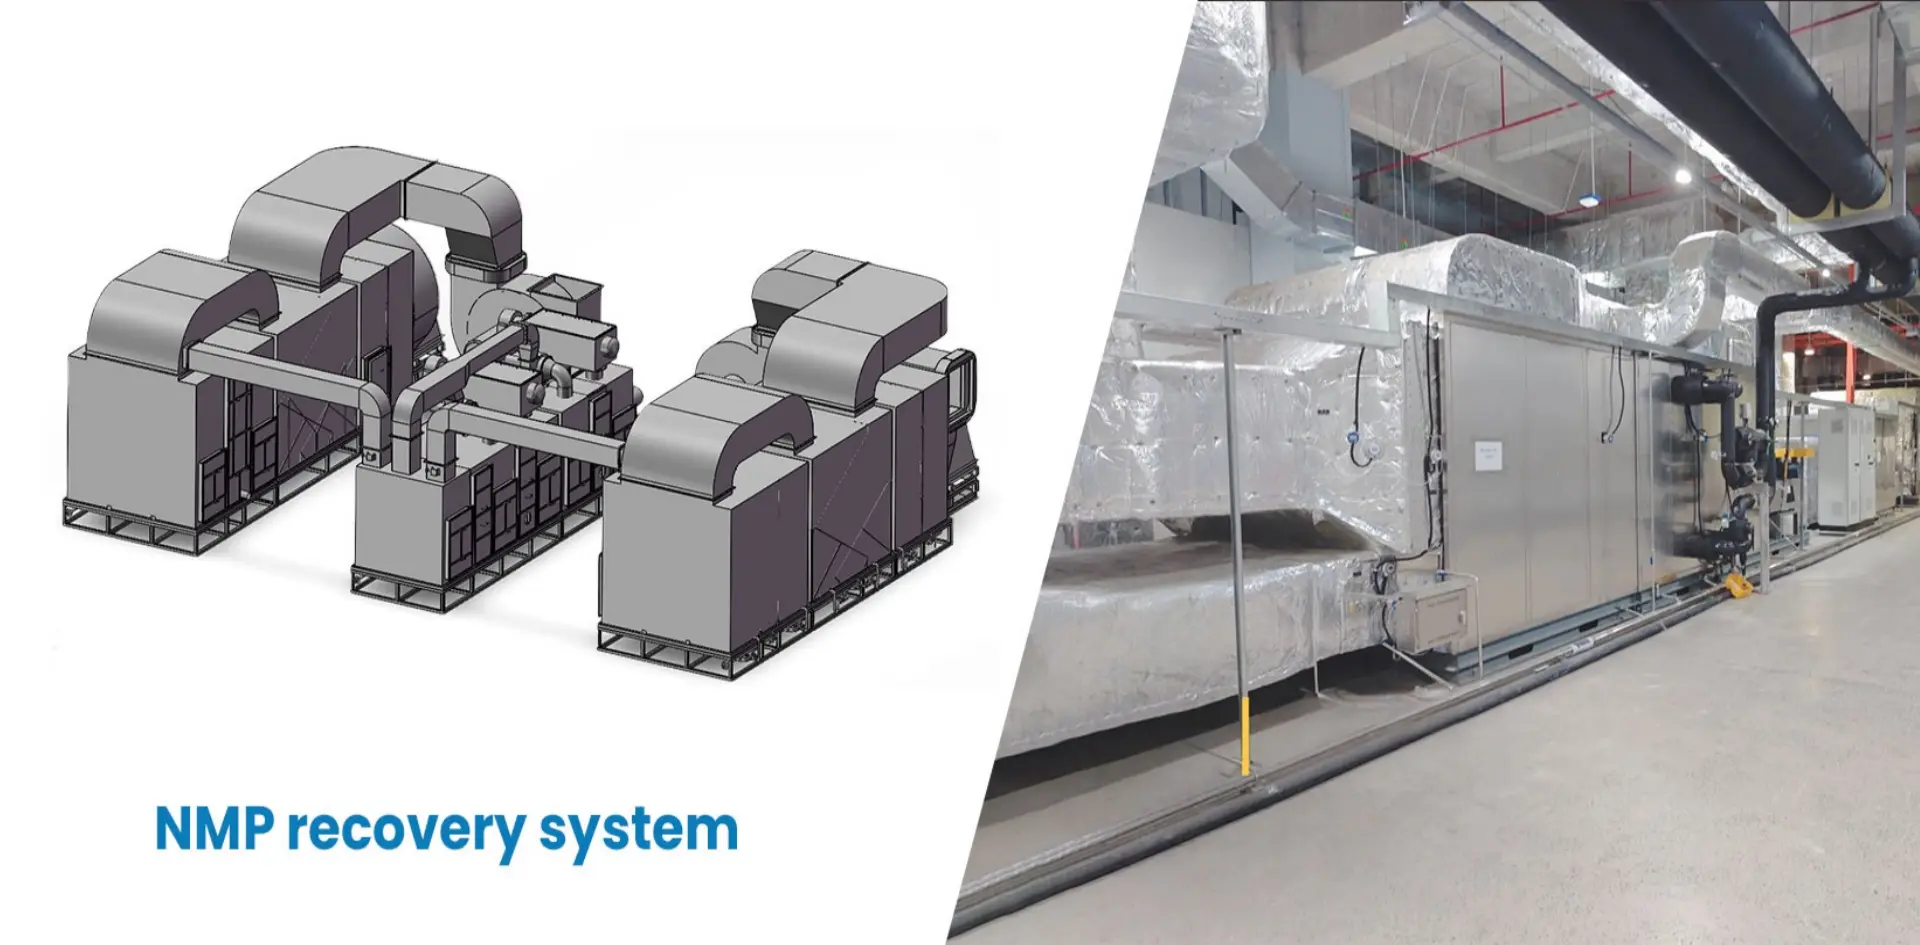 Anti-Caking
Confectionery Dry Systems
Prevents sugar inversion and powder clumping in chocolate cooling tunnels, candy stamping, and pneumatic conveyors.
Custom Engineering →The Macro Environment: Industrial Dehumidification in Modern Food Processing
Across the global food and beverage sector, unregulated relative humidity (RH) is recognized as a critical vector for microbial propagation, hygroscopic powder caking, and packaging seal failures. As international standards like ISO 22000, BRCGS, and FDA FSMA establish stricter sanitary limits, modern food manufacturers are moving beyond standard refrigeration-based condensation coils. Standard cooling coils face freezing limits at lower temperatures and struggle to maintain indoor air quality below 50% RH. This is where high-performance industrial desiccant dehumidifiers play an essential role.
Operating a specialized manufacturing facility in Hangzhou, China, Hangzhou DryAir Treatment Co., Ltd. builds specialized rotary desiccant dehumidifiers engineered specifically for food cleanrooms, baby powder spray drying towers, confectionery packaging, and cold chain distribution hubs. By deploying high-density synthesized honeycomb desiccant wheels infused with active silica gel or metal silicate molecular sieves, our systems continuously extract airborne moisture across sub-zero dew points without frost buildup, achieving supply air down to -70°C dew point.
Localized Application Scenarios in Food Processing
Precision relative humidity parameters tailored to specific microbial, hygroscopic, and thermal sensitivities in industrial food lines.
Confectionery, Candy & Chocolate
Maintains ambient moisture below 35% RH during chocolate cooling, panning, and starch moulding. Prevents sugar bloom, surface stickiness, and microbial contamination while guaranteeing crisp snapping textures.
Dairy, Whey & Infant Formula Spray Drying
Provides steady dehumidification for spray dryer inlet air. Stops powdered milk and nutritional supplements from sticking to exhaust duct walls, maintaining consistency and preventing batch caking.
Pneumatic Powder Conveying & Silo Storage
Pumps clean, dry air into flour, starch, and cocoa powder pneumatic conveyors. Prevents bridging, pipe clogs, and silo moisture pockets without using energy-heavy heating cycles.
Meat Curing, Sausage Drying & Seafood
Delivers consistent low-temperature drying environments for fermented sausages and aged meats. Protects natural casing integrity, optimizes moisture-protein ratios, and eliminates mold risks.
Cold Storage Staging & Loading Docks
Controls humidity at dock doors and transitions to eliminate condensation and floor ice, keeping packaging dry and maintaining slip-free walkways for workers.
Nutraceutical & Effervescent Packaging
Maintains cleanroom air at ≤20% RH for effervescent tablets, vitamin gummies, and functional powders. Stops premature effervescence and preserves active ingredient stability.
Atmospheric Control Parameters Across Processing Nodes
Consult our engineering baseline parameters below when preparing factory HVAC specifications and procurement tenders.
| Food Processing Sector | Target Dew Point / RH Range | Primary Production Hazard | Recommended Machine Architecture |
|---|---|---|---|
| Infant Nutrition & Dairy Powders | -15°C to -30°C DP (10–20% RH) | Powder agglomeration, tower wall adhesion | Rotary Desiccant with High-Efficiency Pre-Cooling |
| Sugar & Gummy Confectionery | -10°C to -20°C DP (20–35% RH) | Surface tackiness, starch inversion | Silica Gel Rotary Dehumidifier + HEPA Stage |
| Effervescent Tablets & Supplements | -40°C to -60°C DP (≤10% RH) | Premature reaction, blister pack seal failure | Double-Rotor Deep Low Dew Point Dehumidifier |
| Meat Fermentation & Curing | +2°C to +8°C DP (55–70% RH controlled) | Case hardening, surface mold propagation | Sanitary Industrial Refrigerative + Desiccant Hybrid |
| Freezer Entry Vestibules & Staging | -25°C to -45°C DP (≤15% RH) | Ice accumulation, evaporative coil frosting | Direct Expansion Desiccant Air Handling Unit |
China Supply Chain Resilience, Scalability & Cost Efficiency
Why international Tier-1 food brands source their core HVAC engineering from Hangzhou DryAir.
Complete Vertical Integration
From precision CNC metal sheet enclosures to proprietary desiccant honeycomb coating, DryAir maintains total in-house fabrication. This cuts sub-vendor delays and ensures reliable build quality.
High-Capacity Factory Output
With a production run exceeding 200 high-capacity industrial units every month, our Hangzhou manufacturing complex accommodates large-scale multi-facility food processing installations on time.
Lifecycle Cost Leadership
Chinese engineering clusters provide strong component sourcing benefits. Combined with DryAir's sensible waste-heat regeneration designs, operating OPEX drops by up to 35% compared to European alternatives.
74+ HVAC R&D Specialists
Our engineering team includes doctoral candidates, master HVAC technicians, and registered consultants who review every food processing psychrometric balance and load calculation before manufacturing begins.
Rigorous Performance Testing
Every single custom food desiccant unit undergoes factory sign-off testing inside our in-house climate validation chamber to confirm CFM airflow, dew point accuracy, and thermal loads before export dispatch.
International Export Track Record
We have delivered mission-critical environmental systems to global brands like Tesla, Northvolt, CATL, and TTI, providing the baseline quality required by multinational food conglomerates.
Technology Roadmap & Sustainable Future Outlook
Advancing next-generation food plant dehumidification through cleaner thermodynamics and intelligent machine monitoring.
Low-Temperature Desorption
Next-gen metal-organic frameworks (MOFs) engineered to regenerate at only 50°C–65°C, using waste hot water from food boiler loops and refrigeration condensers to run desiccant reactivation for minimal energy.
AI Predictive Humidity Control
Dynamic algorithms process localized weather forecasts, real-time factory worker shifts, and processing line loads to continuously adjust rotor rotation and heater wattage, keeping dew points stable with zero energy waste.
Antimicrobial Rotor Matrix
Food-safe nano-silver and zinc-doped composite rotor flutes that stop bacterial colonies, fungi, and biofilm accumulation on desiccant surfaces, complying with clean-in-place (CIP) and cleanroom sanitation standards.
Low-GWP Hybrid Circuits
Pre-cooling and after-cooling refrigeration stages built around low-GWP refrigerants (R290, R1234ze, R513A) to align with EU F-Gas regulations and US EPA SNAP requirements for clean sustainability.
Localized Support, Engineering Standards & Quality Approvals
Ensuring full compliance with international electrical, pressure, hygiene, and mechanical safety codes.
CE & Machinery Directive
Certified to European Union Directives: Machinery (2006/42/EC), Low Voltage (2014/35/EU), and EMC (2014/30/EU) for hassle-free customs clearance and industrial commissioning across the EU.
UL, CSA & ASME Verification
Control panels built to UL 508A specs and pressure vessels certified under ASME Section VIII, matching electrical and mechanical compliance requirements across the United States and Canada.
ISO 9001 & GJB Defense Standards
Operating with ISO 9001 quality management alongside strict GJB military manufacturing standards, ensuring our units deliver dependable structural stability and leak-proof air balance.
Global Technical Dispatch & Support
Supported by cloud remote telemetry, fast spare parts shipments, and specialized service technicians ready to handle on-site installation, commissioning, and training worldwide.
Q&A: Food Desiccant Dehumidification Engineering
Technical responses from our engineering team on cleanroom moisture control, food safety, and system commissioning.
Why is desiccant dehumidification preferred over cooling condensation in food production?
Refrigeration-based dehumidifiers lose effectiveness below 10°C, and their cooling coils frost up when targeting air below 40% RH. Rotary desiccant wheels absorb moisture directly from the air regardless of ambient temperatures. This makes them ideal for maintaining dry environments (down to -70°C dew point) without freezing or dripping water into clean zones.
How do DryAir dehumidifiers stop microbiological growth inside the rotor?
The regeneration sector of our rotary dehumidifiers regularly hits 120°C to 140°C during desorption. This thermal cycle pasteurizes the desiccant rotor with every rotation, neutralizing vegetative bacteria, spores, and fungi before air is reintroduced to food processing lines.
What is the typical lead time for custom engineered OEM food dehumidification systems?
Standard configured desiccant modules typically ship within 3 to 4 weeks. Custom hygienic systems featuring stainless steel construction, explosion-proof components, or specialized HEPA filtration generally ship within 6 to 8 weeks, backed by complete factory validation.
Can waste process heat from factory boilers be used to power desiccant regeneration?
Yes. DryAir builds hybrid reactivation coils that tap into waste steam, thermal oil, hot water loops, or gas burners. Utilizing waste heat significantly lowers electrical loads and cuts ongoing utility costs.
Explore Our Core Engineering Solutions
Browse our complete lineup of desiccant systems, solvent recovery units, and turnkey cleanroom solutions.
DHU Series
Rotary Desiccant Unit
Continuous low-dew-point environmental control for food processing, cleanrooms, and moisture-sensitive storage.
Product Catalog →
Complete Turnkey
Modular Dry Cleanrooms
Turnkey food ingredient packaging enclosures with strict ISO-classified air filtration and temperature controls.
View Cleanrooms →
≥99% Efficiency
ZJRH Solvent Recovery
Recovers expensive organic processing vapors, reducing industrial exhaust emissions and chemical procurement expenses.
Explore Recovery →
JEN Systems
JEN Series VOC Unit
Regenerative thermal oxidation and deep condensation systems ensuring compliance with clean-air industrial exhaust regulations.
View VOC Units →
ISO 9001
Heavy Industrial Rotor AHU
Custom-sized high-CFM air handlers built for continuous round-the-clock operation in high-humidity climates.
View AHU Models →
GJB Defense Tested
Precision Processing Enclosures
Built with airtight sandwich panels, airlocks, and integrated desiccant loops for sensitive manufacturing processes.
Project Details →
High Efficiency
Condensation Dehumidifier
High-capacity primary stage air dryers for production workshops, packaging lines, and warehouse storage facilities.
Explore Chillers →
Custom Built
Turnkey Environmental Air Plant
End-to-end dehumidification systems covering project engineering, manufacturing, on-site commissioning, and lifecycle service.
Request Proposal →