
 DP -70°C
DHU Series Desiccant Dehumidifier
Engineered with patented runner honeycomb seals and energy-optimized desiccant rotors for mission-critical low dew point applications.
View SpecificationsVerified solutions built to eliminate environmental humidity risks, optimize cycle times, and safeguard cathode/anode production yields.
DP -70°C
Engineered with patented runner honeycomb seals and energy-optimized desiccant rotors for mission-critical low dew point applications.
View Specifications Turnkey EPC
Complete clean-dry envelope integration: airtight enclosure, ductwork, HVAC refrigeration balance, and continuous Dew Point validation.
Explore Dry Rooms Recovery ≥99%
Advanced condensation cooling capturing N-Methyl-2-pyrrolidone from coater exhausts, reducing solvent purchasing overhead substantially.
Learn More RTO Integrated
Deep-cooling condensation coupled with Regenerative Thermal Oxidizers (RTO) for extreme volatile organic waste air purification.
Explore Abatement High Airflow
Dual-rotor cascade moisture removal delivering constant dew points under heavy latent load spikes in mass manufacturing plants.
Get Technical Data Class 1 ISO
Airtight cleanroom construction guaranteed to prevent HF generation during delicate electrolyte filling and pouch encapsulation.
Request Layout Hazardous Zone
Specialized explosion-proof recovery systems intercepting hydrocarbon vapor streams across loading racks and chemical tank farms.
View Certifications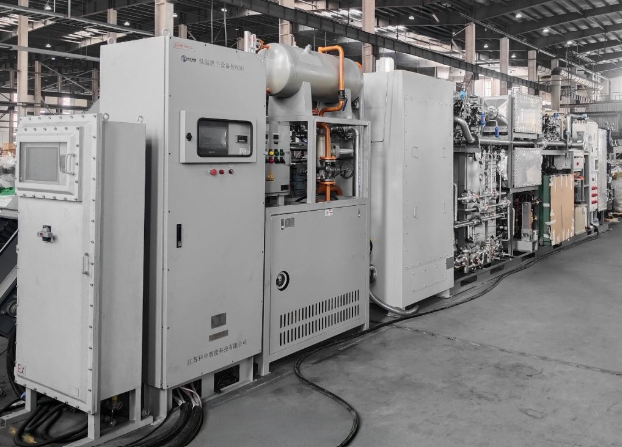 Energy Efficient
Cost-effective moisture extraction for warehouses, staging rooms, and energy-conserving pre-cooling ahead of rotary desiccant wheels.
Inquire EquipmentFounded in 2010, Hangzhou DryAir Treatment Co., Ltd. has evolved into an authoritative force in low-dew-point environmental engineering. Operating from our certified facilities in Lin'an, Hangzhou, our engineering division solves complex industrial moisture migration challenges.
Unlike commodity HVAC manufacturers, DryAir designs tailor-made rotary adsorption systems capable of sustaining -70°C pressure dew point conditions under intense industrial throughput. Our systems are verified across multi-gigawatt battery cell production, solid-state battery R&D laboratories, GMP active pharmaceutical ingredient (API) isolation lines, and aerospace defense depots.
Moisture control is not generic HVAC; it is an unforgiving process baseline. Our systems mitigate microscopic vapor migration across strict operational tolerances.
During cathode mixing, vacuum drying, and electrolyte injection, free ambient humidity triggers exothermic formation of toxic Hydrofluoric Acid (HF). DryAir dry rooms maintain continuous -40°C to -70°C dew point barriers, ensuring maximum cell energy density, cycle lifetime, and fire-safe assembly.
Hygroscopic compounds, effervescent tablets, soft gelatin encapsulation, and dry powder inhalers (DPI) suffer clumped agglomeration and microbial degradation when relative humidity fluctuates. Our units guarantee precise 1% to 15% RH thresholds across Class A/B cleanroom zones.
Capturing volatile N-Methyl-2-pyrrolidone vapors from high-speed coating ovens is critical for operational compliance and resource savings. DryAir condensation recovery loops yield over 99% pure condensed solvent, directly cutting factory raw-material re-procurement overhead.
Built strictly to national GJB standards, our dehumidification systems preserve radar components, ammunition magazines, guided missile enclosures, and naval vessels against internal oxidation, fungal contamination, and electrical harness short-circuits during storage.
Micro-lithography and wafer manufacturing require zero condensed micro-droplets on sensitive optics and substrates. We isolate latent load fluctuations caused by personnel transition doors, preventing costly process line stoppages.
Combining deep mechanical chilling, regenerative carbon adsorption, and RTO thermal incineration, DryAir strips hazardous VOC emissions during crude offloading and tank vent cycles, meeting stringent environmental stack regulations.
Why tier-one gigafactories across Europe, North America, and Asia partner with Hangzhou DryAir to overcome stringent delivery deadlines.
Unlike Western equipment aggregators that outsource core sheet-metal bending, heat exchangers, and electrical panels to disparate subcontractors, DryAir maintains end-to-end manufacturing under one roof at our Qingshan Industrial Park complex. This includes full structural frame welding, anti-corrosion coating, desiccant rotor assembly, and proprietary control cabinet assembly.
Our monthly production run exceeds 200 large-tonnage units, guaranteeing parallel delivery schedules for multi-phase gigawatt plants without extended procurement backlogs.
Leveraging the deep Chinese manufacturing cluster for precision industrial valves, specialized fans, and titanium coils, DryAir delivers capital expenditure (CAPEX) advantages of 25% to 40% compared to legacy North American or European equivalents, with equal or superior thermal efficiency metrics.
Every unit undergoes dynamic testing inside our in-house full-scale psychrometric verification test room before ocean or air shipping, eliminating costly rework during on-site commissioning.
Continuous thermal efficiency gains and artificial intelligence-driven control algorithms driving down industrial lifecycle OPEX.
Transitioning from static PID loop controls to adaptive machine-learning models that forecast exterior humidity spikes and production door-opening cycles, pre-modulating regeneration energy and cutting auxiliary heater draw by up to 22%.
R&D trials in Metal-Organic Framework (MOF) and composite silica-gel honeycomb matrices allow moisture desorption at lower regeneration temperatures (under 80°C vs legacy 130°C), unlocking the practical use of industrial low-grade waste steam.
Proprietary high-elastic airtight wall panel jointing and double-magnetic airlock interlocks engineered to maintain positive enclosure pressure (+30 Pa to +50 Pa), stopping moisture back-migration in high-throughput gigafactories.
Cross-reference dew point thresholds, target airflow kinetics, and engineered system selections to accelerate your design and procurement lifecycle.
| Industrial Application Area | Required Environmental Target | Key Process Hazard Avoided | Recommended DryAir Solution |
|---|---|---|---|
| Lithium-Ion Pouch/Prismatic Winding & Filling | -40°C to -60°C DP | Electrolyte hydrolysis into hydrofluoric acid (HF) | Turn-key Dry Room System |
| Next-Gen Solid-State & Lithium Metal Cells | Down to -70°C DP | Spontaneous oxidation of lithium foil interfaces | Cascade DHU Dehumidifier |
| Electrode Cathode Oven Exhaust Lines | ≥99% NMP Recovery | High raw solvent loss & stack VOC non-compliance | ZJRH Series NMP Unit |
| Hygroscopic Active Pharma API & Blister Packaging | 10% – 25% Relative Humidity | Powder caking, tableting sticking & active loss | Industrial Desiccant Wheel |
| Strategic Defense Munitions & Avionics Storage | ≤35% RH (Constant) | Propellant degradation and corrosion pitting | GJB-Spec Defense DHU Series |
| Bulk Raw Material Warehouses & Pre-Cooling | 45% – 60% RH | Condensation condensation mold and package rot | Refrigerative Dehumidifier |
| Chemical Tank Racks & Hydrocarbon Terminals | <20 mg/m³ Clean Stack | Atmospheric vapor pollution and explosion risks | JEN Deep-Cooling Condensation |
Proven support infrastructure across Europe, the Americas, and Southeast Asia to guarantee reliable deployment and minimal downtime.
DryAir dispatches experienced bilingual commissioning specialists worldwide to oversee structural erection, duct static-pressure balancing, electrical interfacing, and dew point sensor calibration on site.
Verified audit credentials with prestigious multi-national brands including Tesla, Northvolt, TTI, CATL, BYD, and Envision, confirming our operational transparency, factory safety, and rigorous material traceability.
Full technical dossiers provided for international customs and electrical regulatory compliance: UL/CSA field evaluations, CE Declarations of Conformity, ASME boiler stamps, and third-party witnessed test reports.
Clear, direct technical responses addressing international procurement, psychrometric performance, certification, and lifetime warranty.
Select any category below to inspect complete technical datasheets, dimension diagrams, and field performance metrics.
Adsorption Wheel
Compact, highly reliable rotary dehumidifier units ideal for pharmaceutical processing suites, seed storage, and defense depots.
View Product Details
Large Scale
Tailored envelope designs handling human latent moisture loads and extreme automated handling airflow dynamics reliably.
Explore Solutions
Heat Recovery
Multistage chill-water condensers with integrated exhaust heat exchangers ensuring high thermal coefficient of performance (COP).
Request Flowsheet
EPA Compliant
Destroys 99.2%+ of volatile compounds via high-temperature ceramic bed regeneration, meeting the most rigorous emission caps.
Technical Inquiry
Dual Rotor
Two-wheel adsorption cascade maximizing deep drying power for electrolyte filling stations without requiring cryogenic freezing.
Get System Quote
GMP / Clean
Rapidly assembled cleanroom envelopes designed specifically for university, automotive, and military prototyping battery labs.
Download Layouts
Vapor Capture
Skid-mounted modular units for petroleum marine loading terminals and pipeline storage facilities, engineered for Class 1 Div 1 safety.
Review Engineering
Refrigeration
Robust commercial and manufacturing dehumidifiers removing high moisture loads economically during seasonal humidity shifts.
Inspect ModelsProvide your room layout dimensions, required dew point, internal sensible/latent loads, and factory utilities. DryAir's HVAC engineering group will return a comprehensive psychrometric model and design within 24 hours.