Rotary Desiccant Dehumidifier
DHU series rotary desiccant units delivering sustained ultra-low dew points for spray drying towers, dairy powders, and moisture-sensitive nutrient encapsulation.
View SpecificationsArchitected for critical moisture removal in large-scale food manufacturing, ingredient formulation, powder pneumatic conveyance, and precision thermal stabilization.

DHU series rotary desiccant units delivering sustained ultra-low dew points for spray drying towers, dairy powders, and moisture-sensitive nutrient encapsulation.
View Specifications

Total humidity-controlled enclosures with integrated HEPA air handling, low-vapor pressure envelopes, and automated balance for hygroscopic confection and probiotic handling.
Explore Dry Rooms
High-efficiency closed-cycle condensative capture of solvent and organic aromas from food ingredient extraction, pharmaceutical precursors, and specialty drying lines.
View System Details
Deep-cooling condensation coupled with Regenerative Thermal Oxidation (RTO) to eliminate odor, oil vapor, and volatile organic exhaust in large frying, roasting, and extract lines.
View Abatement Units
High-capacity thermodynamic pre-cooling and moisture extractors designed for raw produce warehouses, cold storage dew-point buffering, and meat-curing atmospheric control.
View Refrigerative Units
Specialized dehumidification integration for dairy, starch, and flavoring spray towers preventing hygroscopic wall-sticking and enhancing drying yield.
View Powder Solutions
Engineered sanitary desiccant systems fabricated with 304/316L stainless steel contact areas, clean-in-place (CIP) accessibility, and positive pressure air seals.
View Sanitary Dryers
Cryogenic deep-cooling condensation stations engineered to condense and recapture premium aromatic hydrocarbons and moisture vapor during food essence de-hydration.
View Recovery UnitsA critical evaluation of moisture control engineering, food quality preservation, operational expenditure reductions, and international manufacturing supply chains.
Modern food drying has evolved past crude heat application. International conglomerates face stringent microbiological standards (FDA, EFSA, HACCP) requiring low-temperature dehumidified drying. Conventional thermal drying causes caramelization, enzymatic degradation, and nutritional dissipation. By implementing desiccant dehumidifiers capable of sub-zero dew point air supply, processors maintain product bioactivity, preserve crisp cellular integrity, and drastically minimize oxidative reactions during continuous dehydrating cycles.
As the premier global manufacturing nexus, Chinese industrial dryer engineering merges comprehensive supply-chain verticality with unmatched manufacturing velocity. China's top tier drying equipment builders, such as Hangzhou DryAir Treatment Co., Ltd., integrate custom rotor desiccant synthesis, sheet metal fabrication, ASME certified pressure vessel construction, and PLC software development within in-house smart factories. This integrated verticality eliminates tiered supply-chain markups, shortening lead times by 40% compared to Western counterparts.
Hangzhou DryAir applies rigorous engineering oversight verified through ISO 9001 and national military grade (GJB) quality frameworks. Every drying unit undergoes psychrometric validation within an environmental calibration chamber before dispatch. By leveraging our deep expertise gained through mission-critical battery dry room installations for CATL, BYD, and Tesla, our food industry drying machinery delivers deterministic relative humidity (RH) control without industrial drift.
Auditable manufacturing bandwidth, research depth, and thermodynamic leadership verified across global processing plants.
Engineering customized thermodynamic envelopes around exact biochemical ingredients.
Infant formulas, maltodextrins, and whey protein isolate readily aggregate during fluid bed cooling. Supplying deep dry air (dew point < -20°C) prevents caking, pipeline clogging, and microbial proliferation during post-spray processing and bagging.
Active bacterial strains die rapidly under elevated thermal conditions. Low-temperature dehumidification strips bound surface water at ambient temperatures (15°C to 25°C), ensuring maximum colony forming unit (CFU) preservation.
Gelatin gummies, hard candies, and chocolate polishing rooms require constant dry air curtains to set crystallizing surfaces. Preventing dew point inversion eliminates sticky finished goods and accelerates packaging line speeds by 30%.
Fermented sausages, biltong, and dry marine delicacies demand controlled vapor-pressure equilibrium to prevent surface case hardening while extracting deep internal moisture without rancidifying lipid fractions.
Precise psychrometric target matching is crucial. Consult our target reference chart before issuing requests for proposal (RFPs).
| Food & Bio-Chemical Processing Phase | Target Moisture / Dew Point | Thermodynamic Challenge | Recommended Machine Specification |
|---|---|---|---|
| Probiotic & Enzyme Low-Temp Fluidization | -40°C to -60°C DP | Denaturation of live microorganisms at >30°C | Dual-Rotor Desiccant Dehumidifier System |
| Infant Milk Powder Spray Tower Conveyance | -20°C to -35°C DP | Hygroscopic crusting, pipeline fouling, agglomeration | Turnkey Pneumatic Injection Dry Air Plant |
| Sugar Panning & Confectionery Curing | 20% to 30% RH (18°C) | Latent heat blooms, surface softening, mold growth | Integrated DHU Desiccant Dehumidifier |
| Flavor Essence & Aroma Solvent Recovery | ≥99% Recapture Rate | Emission compliance, volatile aromatic losses | Cryogenic Condensation Recovery Unit |
| Vegetable & Herb Dehydration Clean Exhaust | Emission Threshold Compliant | Particulate dust, pungent steam, organic emissions | Regenerative Thermal Oxidizer (RTO) + Filter |
| Cold Storage Staging & Produce Warehouse | 45% to 55% RH | Frost buildup on evaporator coils, cardboard collapse | Industrial High-Efficiency Refrigerative Dryer |
How corporate net-zero pledges, intelligent SCADA controls, and international compliance define modern dryer procurement.
Steam and fossil burner dryers are being replaced by high-performance heat-pump desiccant systems. By utilizing exhaust condensation enthalpy to regenerate drying rotors, our advanced systems cut operational energy consumption by up to 38%, lowering the carbon footprint per ton of dried foodstuff.
Modern food conglomerates reject static timers. DryAir integrates intelligent PLC systems equipped with self-tuning PID algorithms that monitor incoming ambient humidity in real time, automatically modulating rotor speed and regeneration heaters to deliver uninterrupted supply air at minimum kWh load.
Global enterprise tenders from North America and Europe demand strict regulatory compatibility. DryAir manufactures systems configured to meet UL/cUL standards, CE machinery and electromagnetic directives, ASME boiler and pressure vessel codes, and EAC standards for the Eurasian Economic Union.
Clear answers to critical questions regarding design, delivery timelines, and international field commissioning.
DryAir rotary desiccant dehumidifiers can control supply air down to a minimum of -70°C dew point. This level of extreme dry air engineering is vital for advanced lithium battery cell assembly, precision freeze-drying lines, and hygroscopic powder processing.
Yes. DryAir delivers turnkey clean dry room projects globally. Our scope encompasses pre-sales psychrometric consulting, mechanical engineering, cleanroom partition manufacturing, system delivery, on-site installation, and final dew point validation for clients such as Tesla, Northvolt, and TTI.
Depending on the destination country, systems are delivered with CE mark compliance, UL/cUL certification, CSA approval, ASME boiler stamps, and EAC certification. We operate under ISO 9001 quality management and GJB military precision verification.
DryAir solvent recovery systems routinely achieve recovery efficiencies greater than 99% on industrial coating and drying lines. This substantially lowers expensive chemical solvent repurchase overheads while ensuring compliance with stringent local stack emission thresholds.
International procurement packages include an optional comprehensive 2-year service agreement. This contains 24/7 remote telemetry diagnostic monitoring, fast-track overseas spare parts fulfillment, and on-site field engineering deployment for scheduled maintenance and calibration.
Water activity (aw) dictates microbial propagation. By utilizing desiccant dehumidifiers capable of reducing relative humidity below 10%, moisture is evacuated from products without high-heat cell wall damage, resulting in shelf life extensions without requiring excessive chemical preservatives.
Select from our field-tested equipment configurations engineered to address specific latent heat and moisture extraction demands.
Built with silica gel or molecular sieve rotors to handle high volumetric airflow up to 50,000 m³/h, ensuring positive pressure cleanroom defense.
Get Machine Datasheet
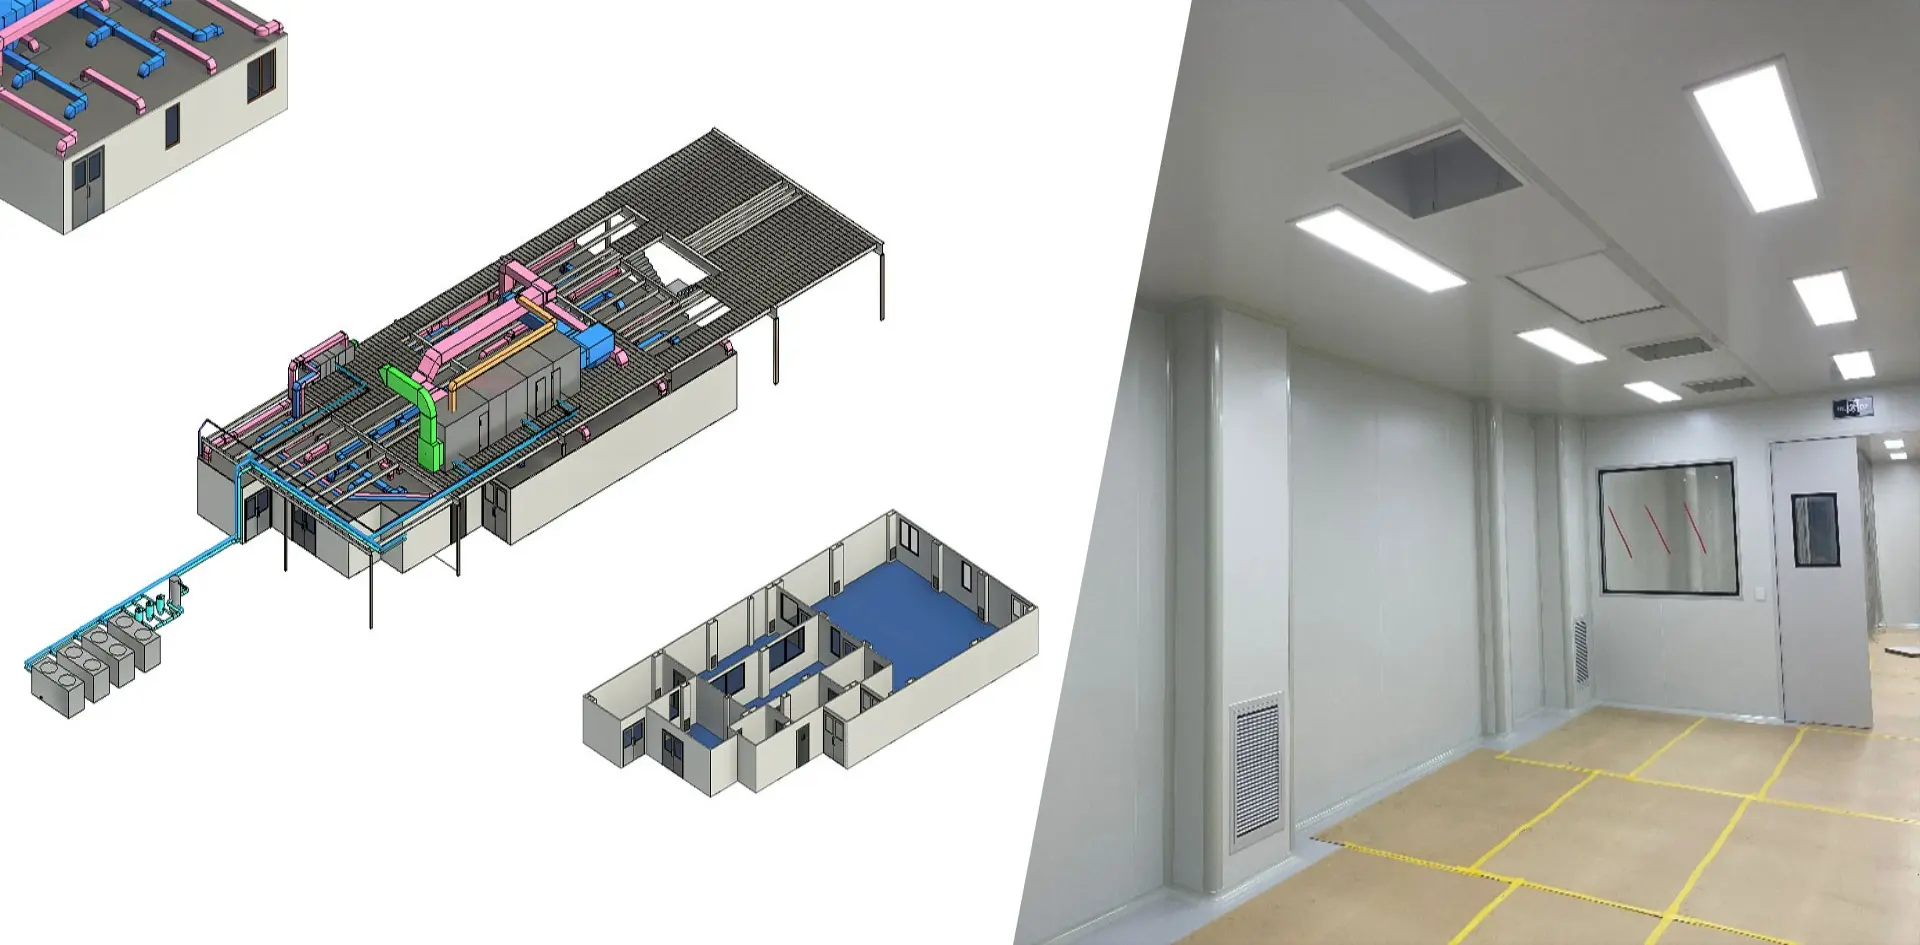
Pre-insulated panels, airtight interlocks, and low-leak dampers delivered as a turn-key suite for food packaging and pharmaceutical production lines.
View Project Specs
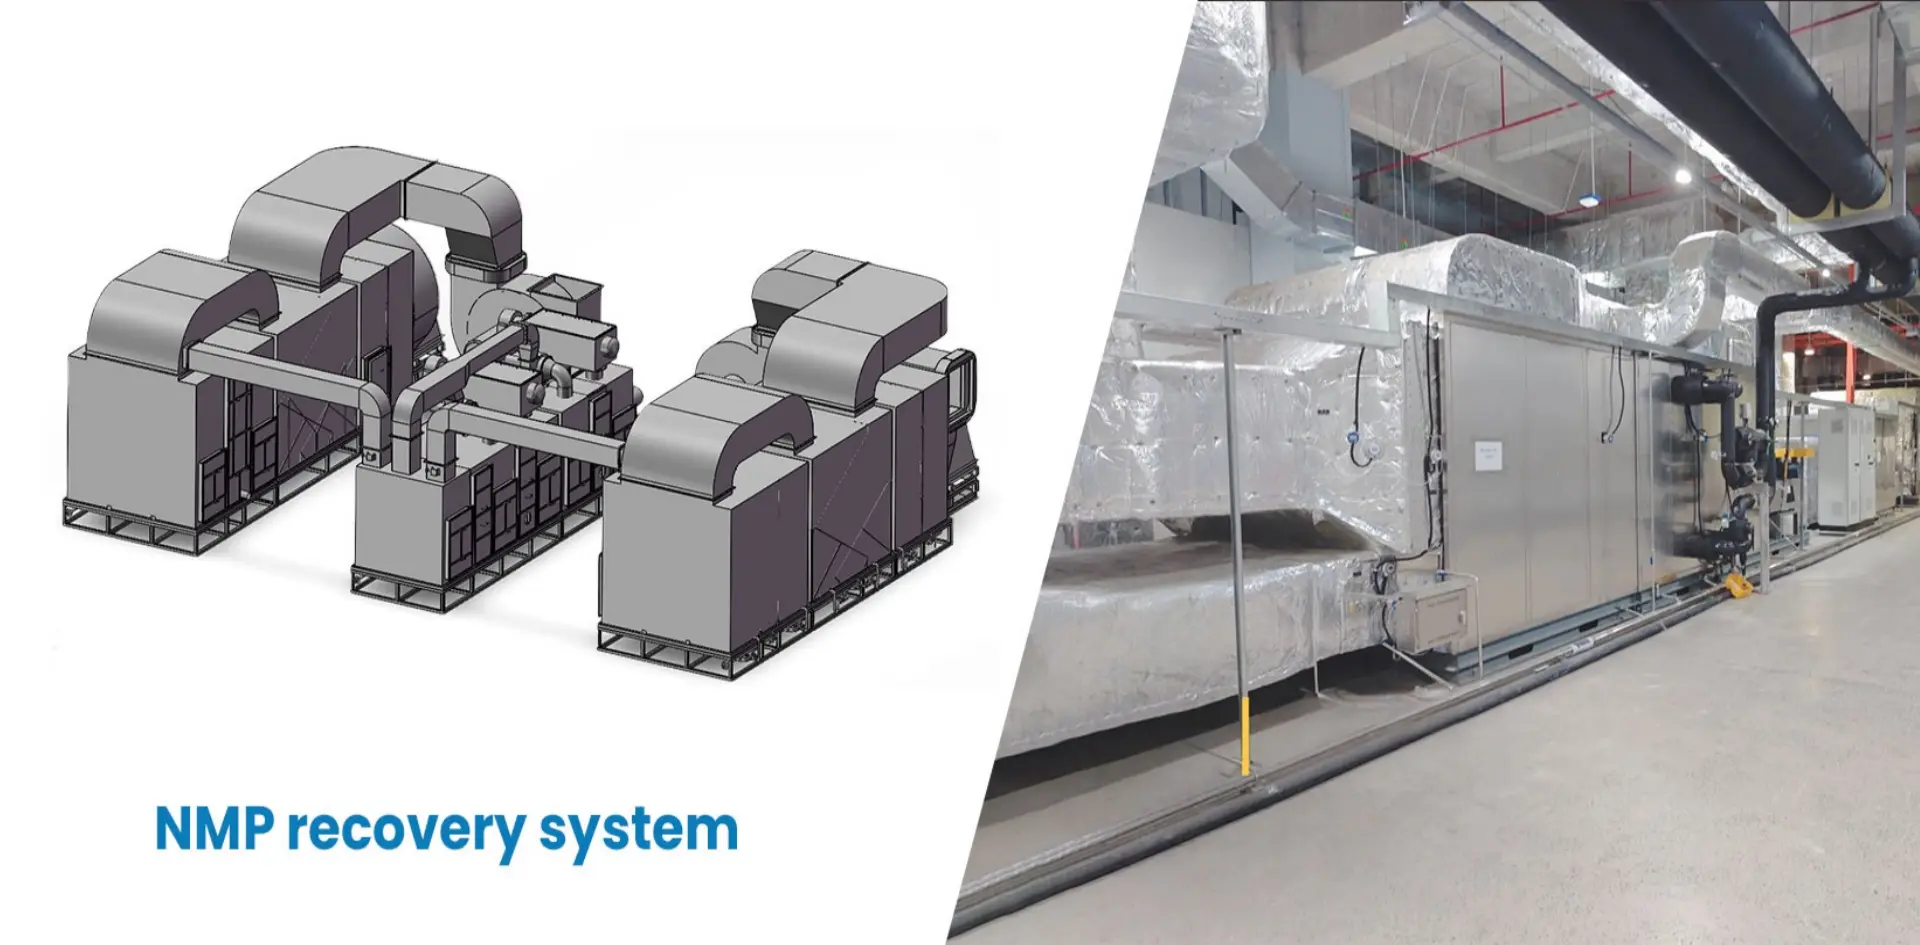
Closed-circuit condensation cooling capturing volatile solvents from food extractors and industrial chemical coating lines with minimal loss.
Download Case Studies
Multi-stage purification linking deep condensation to regenerative thermal oxidation, rendering high-odor food roasting exhaust compliant with environmental standards.
Inspect Air Systems
Reliable thermodynamic moisture removal designed for processing workshops, cold preparation zones, and pre-drying stages ahead of desiccant rotors.
View Refrigerative Models
Custom sanitary design with internal antimicrobial surfaces, double-wall stainless steel insulation, and integrated chilling and desiccant wheels.
Request Custom Build
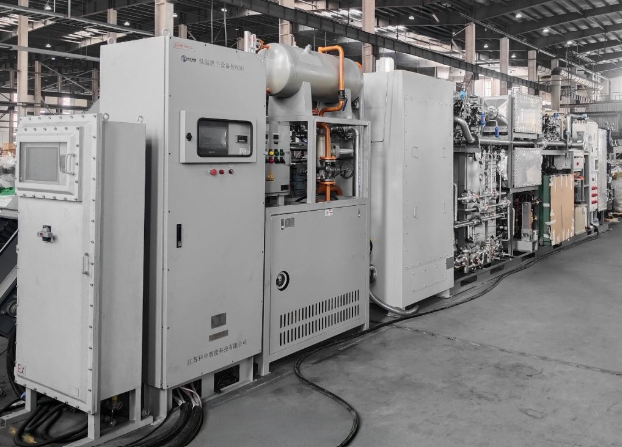
Specialized capture system preventing valuable aromatic compounds from escaping through food drying exhausts, recycling essential fractions.
Review Technical Data
Engineered for round-the-clock confectionery production, effervescent tablet packing, and continuous powder transport at zero moisture accumulation.
Inquire for ProjectsConnect with our senior HVAC thermodynamics team. We analyze your product's moisture load, target relative humidity, and facility footprint to deliver an optimized psychrometric solution.