
 -70°C DP Ready
DHU Desiccant Dehumidifier
Advanced dual-rotor adsorption systems providing stable ultra-low dew points beyond standard mechanical refrigeration limits.
View Specifications →Continuous -70°C dew point performance engineered for gigafactory cell lines, cleanrooms, and moisture-critical chemical production.
-70°C DP Ready
Advanced dual-rotor adsorption systems providing stable ultra-low dew points beyond standard mechanical refrigeration limits.
View Specifications → Turn-Key EPC
Complete envelope enclosure, HVAC ducting, dew-point automation, and airtight airlock validation for battery assembly lines.
Explore Dry Rooms → ≥99% Efficiency
Captures volatile N-Methyl-2-pyrrolidone from lithium electrode coating exhaust, cutting solvent purchase costs significantly.
Examine Technology → Cryogenic + RTO
Deep-cooling condensation paired with regenerative thermal oxidizer (RTO) engineering for clean industrial exhausts.
View VOC Scrubbers →High-capacity condensed water extraction for raw materials storage, production warehouses, and initial pre-cooling air intake.
Discover Refrigeration → Vapor Recovery
Engineered cryogenic condensators for fuel terminals and chemical loading ports preventing hydrocarbon atmosphere discharge.
View Vapor Systems → GMP Compliant
Sanitary stainless-steel construction with integrated HEPA filtration to maintain 10%-20% RH in drug compounding and tableting.
Explore Pharma DHU →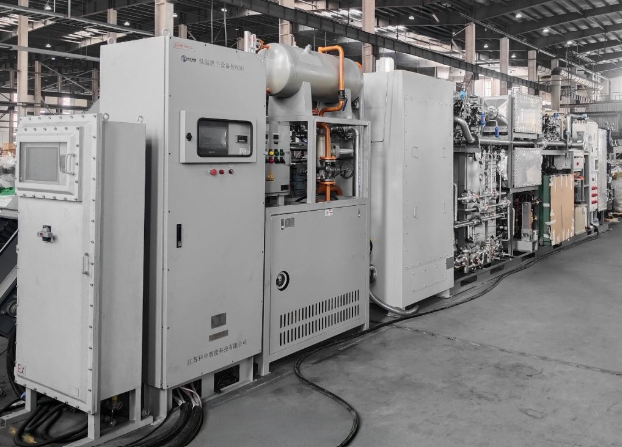 24/7 Run-Time
Specialized closed-loop solvent recovery units matching twin-coater continuous output line-speeds in large battery sites.
Audit Recycler Specs →A macroeconomic and thermodynamic review of why lithium-ion gigafactories, biopharma, and aerospace demand specialized Chinese rotary dehumidifier engineering.
Lithium hexafluorophosphate (LiPF6) within battery electrolytes reacts irreversibly with ambient moisture (H2O) to form corrosive Hydrofluoric Acid (HF). This degradation reduces battery energy density and causes dendrite short-circuits. Standard mechanical chillers freeze at 0°C; hence, solid desiccant silica-gel or zeolite honeycomb rotors operating to -50°C and -70°C dew point are the baseline requirement for modern energy storage production.
Global procurement teams across Europe and North America often face 40 to 60-week lead times for legacy Western desiccant systems. Furthermore, high custom EPC engineering fees dramatically elevate upfront capital expenditures. Chinese rotary desiccant exporters solve these throughput roadblocks with rapid design iteration, scaled modularity, and tight manufacturing lead-times within 8 to 14 weeks.
Rotary desiccant systems consume significant thermal energy to regenerate the moisture-laden silica or molecular sieve wheels. With industrial electricity costs surging worldwide, modern facilities demand integrated heat recovery circuits, waste steam integration, and dual-wheel cascade designs that reduce regeneration thermal loads by 25% to 35% without drifting supply dew point.
How Hangzhou DryAir’s vertically integrated campus delivers 200+ precision units per month with certified global compliance.
From automated CNC sheet-metal laser cutting and PU insulated double-skin panel foaming to electrical control wiring, all DHU assembly happens in-house. This cuts dependency on external sub-contractors and guarantees airtight thermal-break cabinetry (leakage rate < 0.5%).
Every single rotary unit undergoes full-load performance simulation in DryAir's national-standard testing chamber before factory exit. Airflow volume, static pressure, rotor rpm, and -70°C dew point stability are fully documented with digital inspection logs.
With an ongoing output capacity of 200+ units monthly and over 30% domestic market dominance, our Lin'an, Hangzhou plant easily matches multi-gigawatt rollouts without delaying parallel construction phases across global delivery sites.
Units are engineered using synthesized high-hydrophilic silica/zeolite rotors, Ziehl-Abegg EC plug fans, Siemens PLC logic controllers, and Schneider electrical architectures for plug-and-play global servicing and software integration.
Engineered dew point architectures tailored to the stringent environmental vulnerabilities of modern industries.
Electrode slitting, pouch/can stacking, tab welding, and liquid electrolyte injection require continuous dew points between -40°C and -60°C. For emerging solid-state sulfide electrolytes, DryAir delivers custom dry rooms achieving a consistent -70°C dew point to prevent lethal H2S gas evolution.
Built under China's GJB national military standard, our environmental systems prevent structural micro-oxidation and propellant breakdown in ammunition depots, radar domes, optical housings, and missile silo bays, holding stable conditions at ≤40% RH year-round.
Delivering sterile, laminar dry air for hygroscopic powder synthesis, effervescent tableting, and softgel drying tunnels. Eliminates pill clumping, accelerates gelatin drying cycles, and fully complies with GMP hygiene validations.
Use this engineered matrix to assess process air targets, typical tolerance brackets, and core machine configurations.
| Industrial Process / Application | Air Supply Target | Permissible Moisture Load | Primary DryAir Solution | Recommended Configuration |
|---|---|---|---|---|
| Lithium Battery Cell Assembly & Filling | -40°C to -60°C DP | < 0.12 g/kg dry air | Turn-key Dry Room System | Dual-wheel series cascade with chilled water pre-cooling |
| Next-Gen Lithium Metal & Solid State | Down to -70°C DP | < 0.0033 g/kg dry air | DHU Desiccant Dehumidifier | Low-leakage molecular sieve rotor + deep chilled fluid loop |
| Cathode Electrode Coater Exhaust | ≥99% Solvent Yield | High NMP gas conc. | NMP Recovery System | Multi-stage chilled condensation + honeycomb adsorption |
| Pharmaceutical Powder Handling & Gelatin | 10% to 25% RH | Controlled low ambient | DHU Series Rotary Unit | Hygienic stainless internal casing with HEPA terminal banks |
| Defense, Avionics & Missile Silo Storage | ≤35% to 40% RH | Non-condensing ambient | Military-Grade DHU | GJB-compliant anti-vibration casing with remote SCADA telemetry |
| Raw Materials Warehousing & Pre-Cooling | 45% to 60% RH | Bulk condensation removal | Refrigerative Dehumidifier | High-efficiency scroll compressor with direct air expansion |
The industrial roadmap toward zero-carbon manufacturing, artificial intelligence telemetry, and composite adsorption.
Legacy systems run reactivation blowers and heaters at static maximum capacity. Modern DryAir units integrate edge AI algorithms calculating real-time personnel loading, outside seasonal wet-bulb fluctuations, and airlock breaches to modulate reactivation temperatures by inverter drives, saving up to 22% in annualized power.
As corporate carbon border tariffs (CBAM) take effect, factories must lower natural gas and direct electric heating reliance. Next-generation desiccant systems utilize heat pumps, compressor waste-heat recovery loops, and low-pressure plant steam (80°C to 120°C) to regenerate high-performance composite silica wheels.
The industry is transitioning from classic silica matrices to nanostructured MOF and specialized zeolite composite rotors. These materials present steep water adsorption isotherms, allowing ultra-low desorption temperatures, higher equilibrium moisture uptake, and significantly longer rotor lifespans in aggressive solvent-laden air.
Key risk mitigations and auditing guidelines when selecting a Chinese desiccant dehumidification equipment partner.
Exported machinery must fulfill destination-specific directives without field rework. DryAir provides native CE (Machinery & Pressure Equipment), UL-508A (North America), CSA (Canada), ASME Section VIII pressure vessel stamps, and EAC customs certification for Euro-Asian union countries.
Avoid untested suppliers. DryAir's systems are validated across tier-1 cell companies including CATL, BYD, EVE Energy, SVOLT, and transatlantic projects for Tesla, Northvolt, and TTI, providing bankable proof of capability for international investor diligence.
Split responsibilities between enclosure builders, dehumidifier vendors, and balance-of-plant installers create legal and technical handoff voids. We handle entire dry room packages from pre-sales heat-load calculations through commissioning and dew-point sign-off.
We supply complete documentation in English, 24/7 bilingual remote telemetry assistance, local spare parts consignment, and an optional 2-year overseas warranty plan encompassing on-site field engineer commissioning anywhere in the world.
Expert answers addressing the technical, contractual, and environmental details international purchasers ask first.
Choose from our standardized and bespoke dehumidifier portfolio, certified to ISO 9001 and delivered worldwide.
DHU Model
High-capacity rotary desiccant units built with honeycomb silica/molecular sieve wheels for deep ambient moisture stripping.
Select Dehumidifiers →
EPC Delivery
Turnkey moisture-free production suites engineered with airtight rockwool panel walls, airlocks, and integrated -70°C air supply.
View Turn-Key System →
Solvent Recycler
Continuous closed-loop condensation recovery capturing 99%+ N-Methylpyrrolidone vapors from high-speed battery coater lines.
Audit NMP Plant →
Emissions Compliant
Deep-cooling condensers coupled with regenerative thermal oxidation to decompose chemical plant off-gases into benign CO2 and water.
Examine VOC Solutions →Robust mechanical DX cooling systems engineered for broad humidity control across raw chemical materials warehouses and pre-treatment.
Select Refrigeration →
Hydrocarbon Capture
Packaged condensation recovery equipment designed to catch fugitive petroleum and solvent fumes during road tanker and marine loading.
Inspect Vapor Skids → Military Spec
Ruggedized, GJB-standard environmental systems preserving aircraft avionics, artillery caches, and aerospace optical modules from corrosion.
View Defense Systems → Sterile Class
Precision sterile air handlers providing exact relative humidity control for moisture-sensitive active pharmaceutical ingredients (APIs).
Browse GMP Units →