
 Dew Point -70°C
Industrial Desiccant Dehumidifier
Dual-rotor sorption unit featuring low-temp silica gel and molecular sieve matrices for deep moisture extraction in clean environments.
View SpecificationsEngineered for extreme psychrometric duties where ambient moisture and airborne contaminants compromise structural yield, chemical safety, or thermal integrity.
Dew Point -70°C
Dual-rotor sorption unit featuring low-temp silica gel and molecular sieve matrices for deep moisture extraction in clean environments.
View Specifications Turnkey EPC
End-to-end design, envelope sealing, HVAC purification, and validation for gigafactory battery and sterile pharmaceutical manufacturing.
Explore Dry Rooms ≥99% Efficiency
High-efficiency closed-circuit condensation and absorption trains designed for lithium battery electrode coating exhaust recapture.
NMP Recovery Details RTO + Cooling
Integrates cryogenic condensation with regenerative thermal oxidation (RTO) for chemical, coating, and polymer exhaust purification.
VOC Abatement Tech Pre-Cooling HVAC
High-capacity sensible and latent heat removal units, serving as primary stages before deep-sorption desiccant processing.
Refrigerative Catalog ISO Class 5-7
Equipped with HEPA/ULPA filtration, gas-phase chemical filters, and strict airtight casings (leakage <0.5%) for sensitive cell assembly.
Clean AHU Specs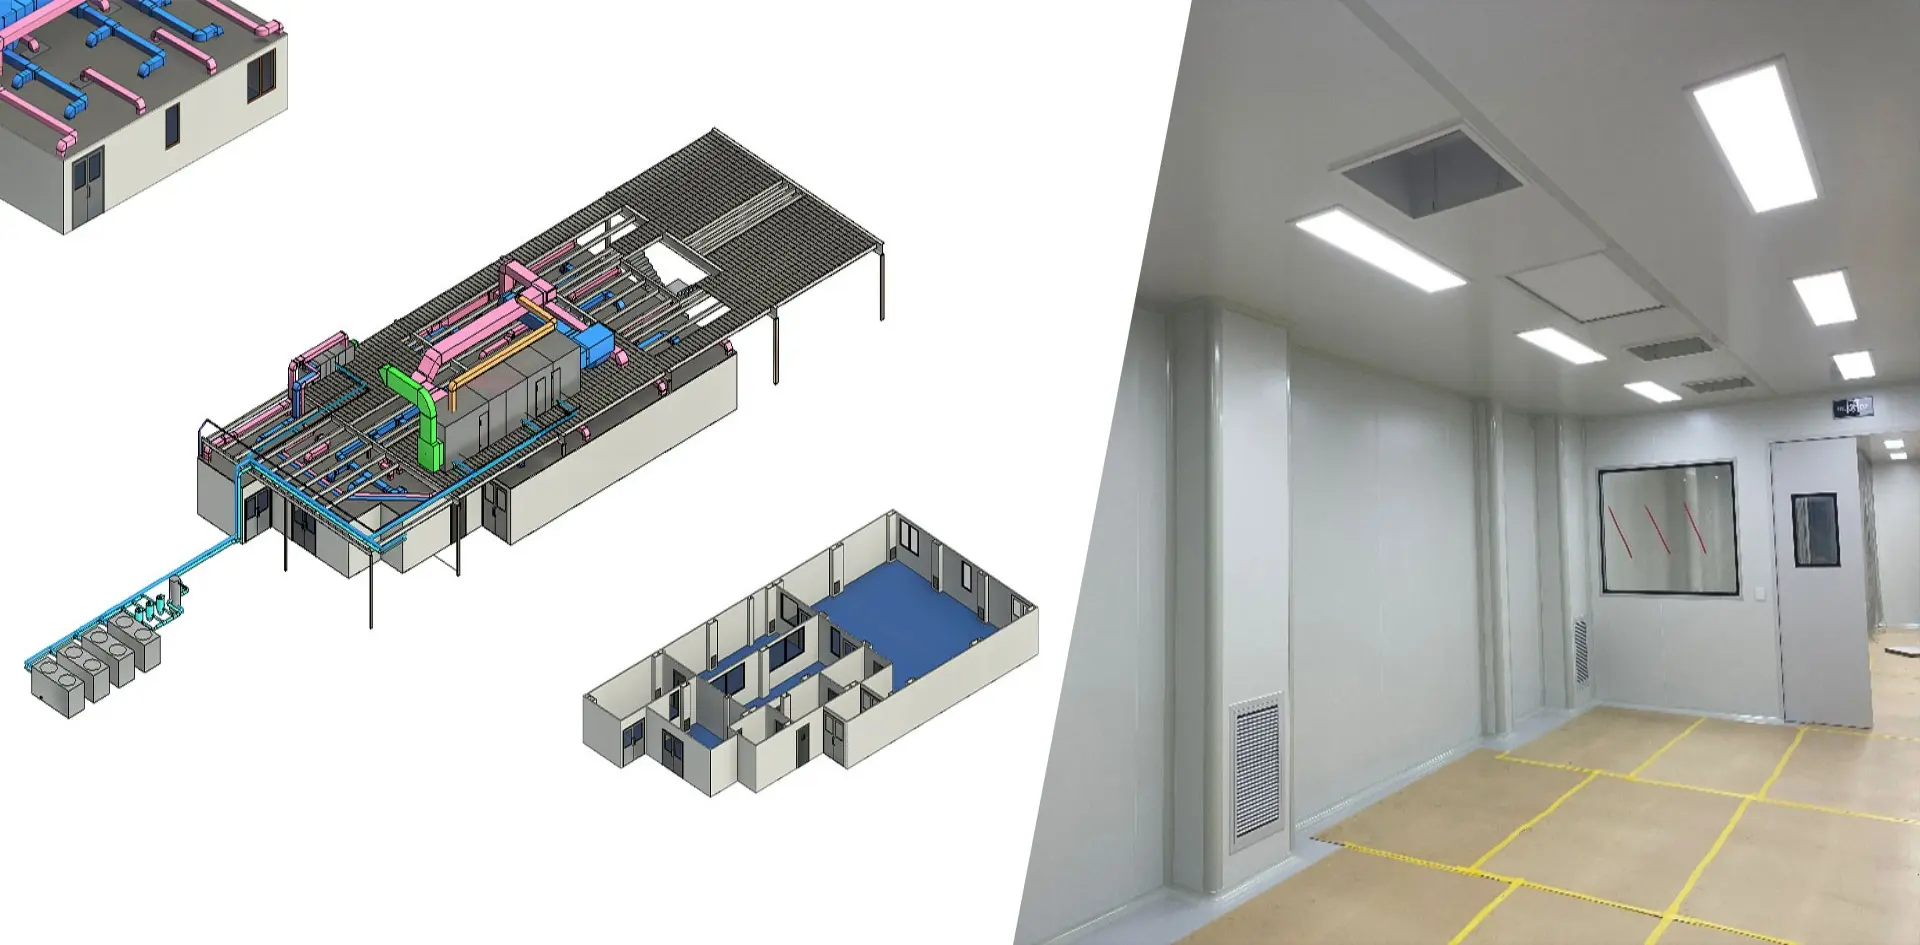 Waste Heat Reuse
Utilizes process thermal waste, steam, or heat pumps for desiccant wheel reactivation, slashing total plant OPEX by up to 35%.
Energy Audit Sheet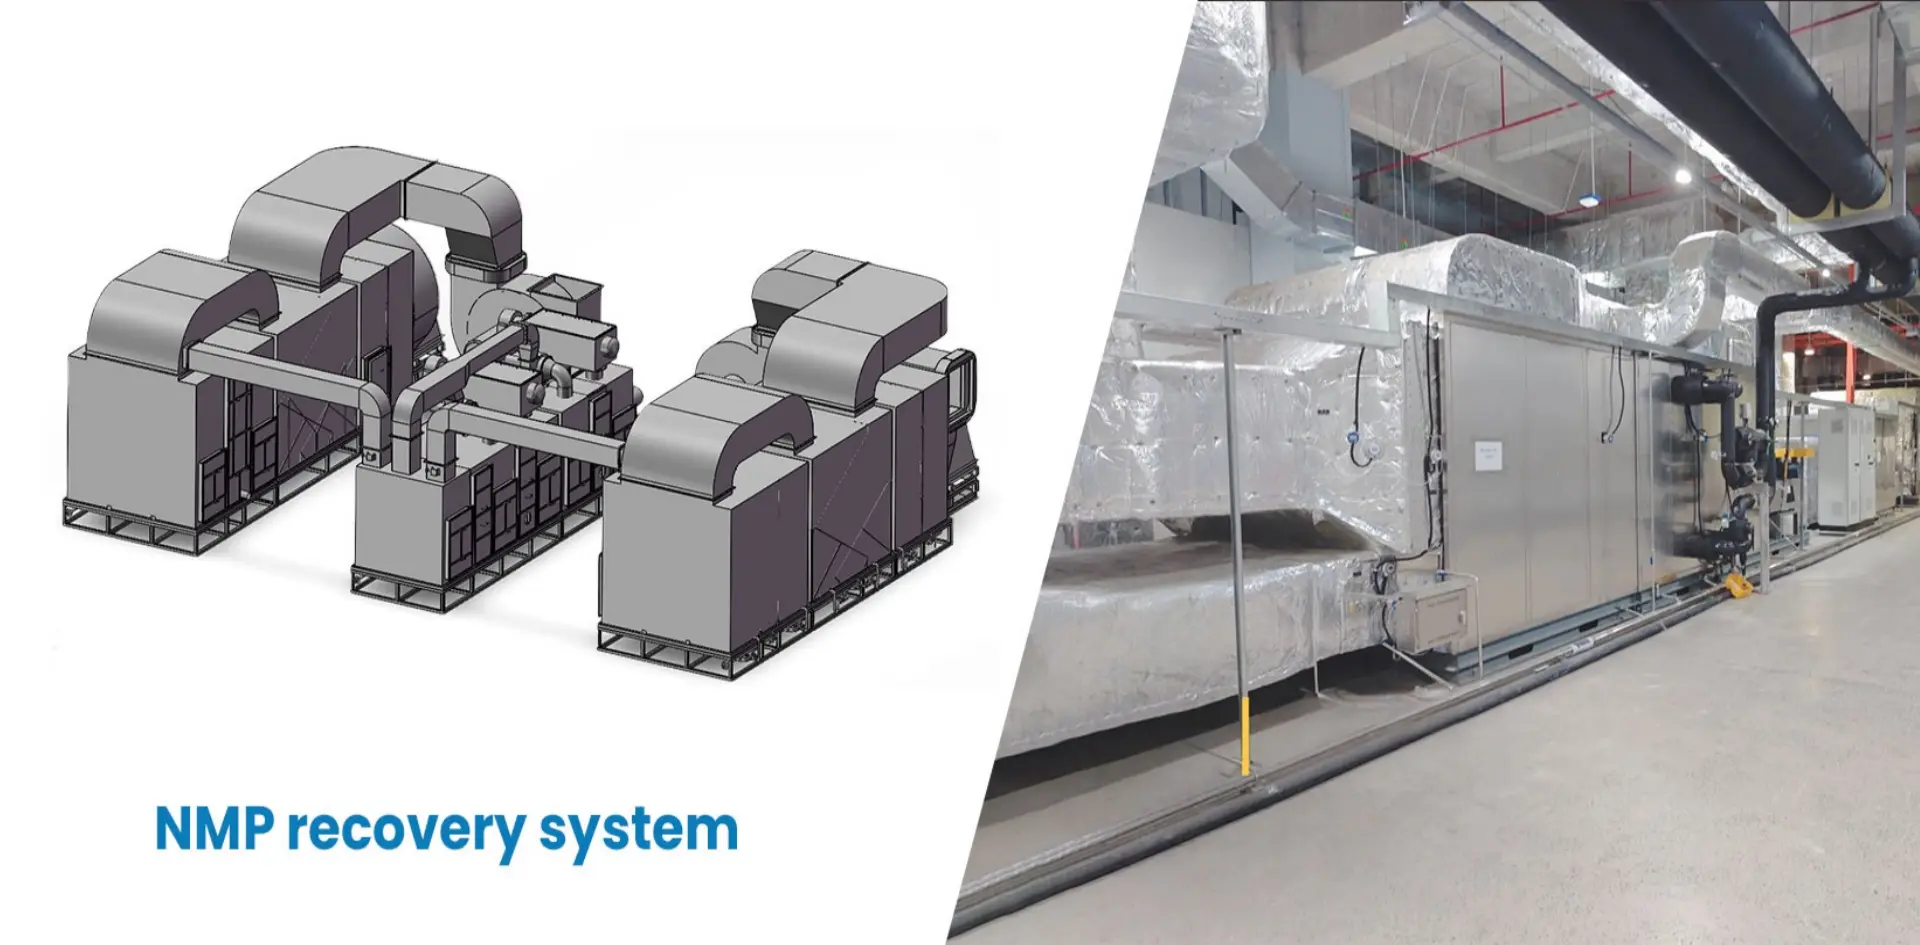 GMP Compliant
Antimicrobial rotor substrate with automated CIP washdown compatibility and sanitary duct interfaces complying with FDA and GMP Annex 1.
Validation MatrixIn modern advanced manufacturing, ambient air is no longer treated as a passive environmental background; it is an active reactant. Controlling moisture and contaminants dictates product reliability, electrochemical density, and batch yields.
Lithium hexafluorophosphate (LiPF6) in electrolyte reacts instantaneously with atmospheric moisture to form hydrofluoric acid (HF), causing irreversible cell degradation, micro-shorting, and thermal runaway risks. We engineer multi-rotor HVAC purification trains that maintain stable, validated -40°C to -70°C dew point conditions across electrode slitting, winding, and filling rooms.
Hygroscopic active pharmaceutical ingredients (APIs), effervescent oral solids, and biological freeze-drying loading require low relative humidity (<15% RH) while preventing cross-contamination. Our HVAC air purify dehumidifiers incorporate sanitizable antimicrobial synthetic rotor matrices, closed-loop condensation, and HEPA H14 terminal filtration adhering to cGMP standards.
Manufactured strictly under China's GJB national military standard, our climate control enclosures prevent galvanic oxidation, fungus development, and optical delamination in radar housings, missile propellant storage, and aerospace avionics maintenance bays, surviving external ambient shocks from -45°C to +55°C.
International EPC contractors, cleanroom builders, and battery consortiums face mounting pressures: compressed commissioning timelines, surging operational power costs, and strict ESG compliance. China’s supply chain delivers unique engineering and cost advantages.
Traditional European and North American industrial dehumidifiers carry high markups and rigid 32-40 week fabrication queues. As a leading manufacturer based in Hangzhou, China, Hangzhou DryAir Treatment Co., Ltd. delivers vertically integrated production from rotor silification to structural casing insulation.
Our solutions reduce initial capital expenditure by 25% to 40% while matching or exceeding Western performance parameters. Integrated heat recovery regenerators directly capture exhaust heat from chillers and compressors, drastically lowering running OPEX.
Scaling a multi-gigawatt battery plant or expansive semiconductor fab leaves zero margin for delivery bottlenecks. DryAir operates a monthly manufacturing throughput exceeding 200 large-tonnage units within automated production facilities.
We have supported rapid capacity rollouts for CATL, ATL, BYD, EVE Energy, Farasis, Envision, and SVOLT, and matched accelerated schedules internationally for Tesla, Northvolt, and TTI across Europe, the Americas, and Southeast Asia.
Equipment arriving at an overseas facility must satisfy domestic safety codes, electrical guidelines, and pressure vessel directives. DryAir systems are engineered for cross-border integration from the blueprint stage.
Built with UL 1995 compliance for custom HVAC, CSA C22.2 electrical distribution, and ASME Section VIII certified refrigeration/steam pressure vessels.
Full conformance to Machinery Directive 2006/42/EC, Low Voltage 2014/35/EU, EMC 2014/30/EU, and ATEX explosion-proof compliance for VOC exhaust zones.
TR CU 010/2011 (Machinery Safety) and TR CU 004/2011 certified for continuous sub-zero Arctic ambient installation across CIS and Eurasian mining facilities.
Turnkey commissioning teams deployed globally with an optional 2-year full-service warranty, remote telemetry monitoring, and local spare parts caches.
Under-sizing dehumidification leads to product spoilage and costly downtime; over-sizing inflates initial CAPEX and continuous power draw. Match your process requirements with verified field parameters.
| Target Application | Air Purity (ISO 14644) | Moisture Target (DP / RH) | Air Handling & Purification Architecture | Recommended System |
|---|---|---|---|---|
| Lithium-Ion Electrolyte Filling | Class 5 (Fed Std Class 100) | -50°C to -65°C Dew Point | Dual-rotor desiccant, HEPA terminal, casing leakage <0.3% | Turnkey Dry Room |
| Solid-State / Lithium-Metal Cells | Class 5 to 6 | -65°C to -70°C Dew Point | Cascaded 3-stage sorption, molecular sieve, hermetic sealing | DHU Desiccant |
| Electrode Drying & Slurry Prep | Class 7 to 8 | ≥99% Solvent Recovery | Multi-stage closed chiller condensation, gas scrubber, carbon bed | NMP Recovery |
| Active Pharma Capsule & Tablet Compression | Class 7 (Grade C / cGMP) | 15% - 25% RH @ 21°C | Antimicrobial rotor, chemical F7+H14 filtration, positive pressure | Pharma DHU |
| Aerospace Composites & Avionics Storage | Class 8 | ≤35% RH (Non-condensing) | Standard silica desiccant, variable air volume (VAV), economizer | Refrigerative / DHU |
| Industrial Paint & Petrochem Exhaust | Standard Exhaust / ATEX | <20 mg/Nm³ VOC Emission | Deep-cooling condenser, continuous zeolite rotor concentrator, RTO | VOC Abatement |
Desiccant reactivation historically ranks among the most energy-intensive thermal loads in industrial cleanrooms. Our Hangzhou research facility is addressing this challenge through three core technological initiatives.
Traditional desiccant wheels require regeneration air temperatures between 120°C and 140°C, usually driven by electric heating coils or high-pressure steam. DryAir’s new composite metal-organic framework (MOF) rotor matrices desorb moisture at just 60°C to 75°C.
This allows industrial facilities to power regeneration using low-grade waste hot water from cleanroom chillers and compressed air cooling circuits, eliminating electric heater spikes.
Traditional cleanrooms operate with static supply safety margins, wasting energy when ambient conditions are mild or personnel occupancy drops. Our integrated AI edge controllers analyze outdoor wet-bulb trends, room enthalpy loads, and real-time personnel traffic.
The system dynamically shifts wheel RPM, face-and-bypass dampers, and heat pump modulation to maintain pinpoint -70°C dew point stability while lowering annualized utility draw by 18% to 26%.
Combining the moisture extraction cycle with near-zero VOC/NMP emissions. Modern electrode plants no longer treat air handling and exhaust cleanup as disconnected systems.
Our integrated loop recycles ≥99% of solvent vapor, captures the latent heat of condensation, and redirects that thermal energy into primary dry room pre-heating, establishing a true circular industrial microclimate.
With 74 in-house engineers, registered HVAC specialists, and technicians, DryAir manages projects from initial psychrometric modeling through to on-site validation.
We analyze process enthalpy, calculate infiltration through airlocks, quantify operator latent moisture loads, and establish supply air mass flow requirements.
Casings are built with heavy-gauge aluminum profiles, thermal breaks, and rockwool insulation, preventing casing condensation in tropical conditions.
Every industrial unit runs in our certified performance testing chamber, measuring full airflow, static pressure, rotor delta-T, and sub-zero dew points prior to crating.
Our field engineering team handles on-site placement, duct integration, sensor calibration, and IQ/OQ validation across your facility.
Clear, engineering-backed answers addressing the operational, financial, and mechanical considerations of international clients.
Choose from standardized platforms or configure custom equipment matching your project's psychrometric and footprint requirements.
Ultra-Low DP
Silica and molecular rotor unit maintaining continuous sub-zero dew point operations for advanced manufacturing.
View Product Specs
Full EPC Turnkey
Integrated envelope panels, air distribution ducts, dehumidification units, and automatic control architecture.
Explore Dry Rooms
Solvent Capture
Captures volatile N-Methyl-2-pyrrolidone vapors with over 99% recovery efficiency on coating lines.
NMP System Specs
Clean Exhaust
Combines deep-cooling condensation and regenerative thermal oxidation to ensure emission limits compliance.
VOC Abatement Data GMP Compliant
Custom sanitary casing construction with zero bacterial retention, HEPA filtration, and strict low RH control.
Pharma Solutions GJB Certified
Engineered for mission-critical defense hardware, ammunition storage, and radar shelters against corrosion.
Defense Dehumidifiers Oil Gas Recovery
Captures hydrocarbon vapors during tank filling, storage transfers, and terminal loading in refineries.
Download Catalog Clean Process
Maintains strict temperature, humidity, and particle levels for optical assembly, SMT lines, and clean storage.
Contact Engineers