
Primary Industrial Dehumidification & Dehydration Machine Fleet
Engineered to handle extreme latent thermal loads, prevent hygroscopic agglomeration, and deliver continuous drying performance across tomato powder, agro-industrial, and high-spec cleanroom facilities.
 DP -70°C CONTROL
Desiccant Dehumidifier
DHU series rotary desiccant dehumidifiers deliver stable low-dew-point air where refrigeration alone cannot reach, mitigating hygroscopic caking in tomato powder processing.
- Minimum -70°C dew point control
- Heat-recovery regeneration cycle
 TURNKEY EPC
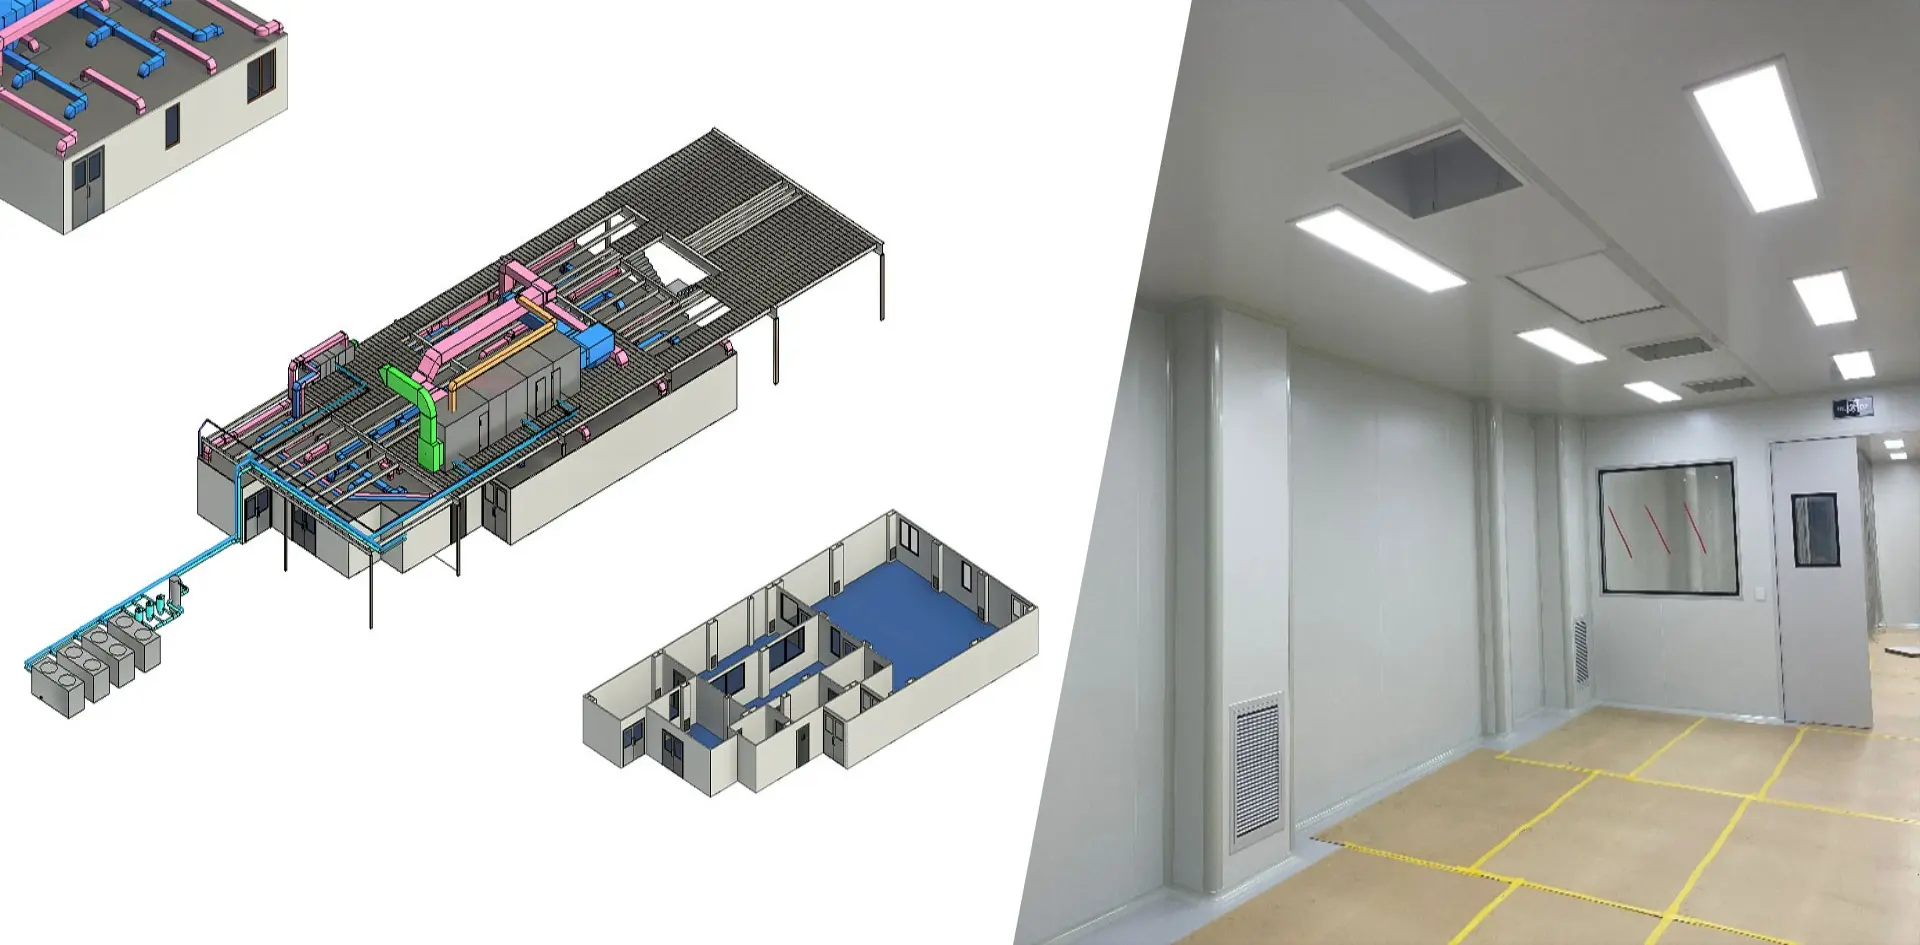
Turn-key Dry Room System
Complete humidity-controlled rooms—enclosure, air handling, dehumidification, controls, and validation—delivered under single-source engineering accountability.
- Pre-sales consulting to commissioning
- Proven in high-capacity dry plants
 EFFICIENCY ≥99%
NMP Recovery System
High-efficiency solvent condensation and secondary purification systems engineered to recapture industrial solvents and reduce operational carbon expenditure.
- ≥99% solvent recovery yield
- Closed-loop emission management
 DEEP COOLING + RTO
VOC Abatement System
Deep-cooling condensation combined with regenerative thermal oxidizers to treat complex exhaust matrices, eliminating volatile organic off-gassing.
- Destroys 99.5% of process VOCs
- Compliant with global clean air norms
Refrigerative Dehumidifier
Cost-effective primary stage moisture removal for food dehydration facilities, preprocessing plants, and low-humidity buffer warehouses.
- High COP refrigeration compressors
- Ideal primary dehumidification tier
 HYBRID AIR FLOW
Industrial Multi-Rotor Dry System
Dual-cascade silica gel and molecular sieve dehumidification arrays built specifically to preserve flavor compounds during tomato spray drying.
- Lycopene protection thermodynamics
- Zero-moisture crystallization feed
 CONTINUOUS FLOW
Continuous Agro-Powder Enclosure
Hermetically sealed environmental packaging cells that maintain RH < 15% to safeguard high-sugar tomato powder from clumping upon cooling.
- Positive pressure enclosure design
- Clean-in-place (CIP) compatibility
 HEAT RECOVERY
Thermal Exhaust Energy Recovery
Secondary heat exchange equipment capturing latent sensible exhaust enthalpy from dry towers, slashing drying energy consumption by up to 34%.
- High corrosion-resistant metallurgy
- Direct ROI via utility conservation
Industrial Evolution: The Dry-Type Tomato Powder Machine Paradigm
A technological analysis on how low-dew-point environmental control and advanced dry-type machinery are revolutionizing fruit and vegetable dehydration worldwide.
Thermally Sensitive Lycopene Integrity
Traditional high-heat dehydrators incinerate heat-labile lycopene and volatile aromatics. The modern shift in China dry-type machinery relies on low-temperature dehydration assisted by continuous rotary desiccant dehumidification down to negative dew points. By lowering atmospheric vapor pressure, moisture sublimates and evaporates without exceeding the 55°C caramelization and nutrient degradation threshold.
Combating High Fructose Hygroscopicity
Tomato solids possess an extreme glass transition temperature (Tg) vulnerability due to concentrated glucose and fructose. Standard exhaust air results in immediate wall-sticking, cyclone clumping, and piping blockages. Integrating dry air dehumidification into cyclone separation and post-cooling pneumatic delivery solves powder caking at the root level, ensuring free-flowing granularity.
Net-Zero Energy Reconfiguration
Drying is intrinsically energy-intensive. Modern dry-type systems deploy advanced thermal regeneration matrixes—similar to NMP solvent condensation and VOC heat recovery units—where sensible enthalpy from desiccant wheel regeneration is returned to the intake preheater, reducing overall electrical and steam expenditure by up to 38% compared to legacy plants.
Global Enterprise Procurement Matrix & Performance Benchmarks
Clear thermodynamic selection standards used by tier-one multinational food ingredient conglomerates and pharmaceutical manufacturing engineers.
| Subsystem / Parameter | Legacy Open-Loop Standard | Advanced Dry-Type Machine Specification | Production Impact & Financial Yield |
|---|---|---|---|
| Process Air Dew Point | Ambient (+12°C to +25°C DP) | -20°C to -70°C DP (Continuous) | Zero wall sticking; preserves 94%+ lycopene content without scorching. |
| Powder Moisture Retention | 4.5% - 7.0% (Inconsistent) | < 2.5% Controlled Moisture | Extends non-caking shelf life from 6 months to 24+ months under vacuum seal. |
| Thermal Exposure Duration | High Temp (180°C - 220°C) | Low-Temp Dehydration (45°C - 75°C) | Preserves natural red color index (a/b ratio > 2.1) without artificial pigments. |
| Energy Recovery Factor | None (Total Loss Stack) | Condensation & Sensible Regenerative Recovery | Utility cost reduction of $18–$35 per ton of finished high-grade tomato powder. |
| CIP Cleanability & Material | SS304 Non-Passivated | Mirror-Polished SS316L (Ra < 0.4 µm) | Meets global FDA, cGMP, and 3-A Sanitary standards; halts microbial proliferation. |
Hangzhou DryAir: Precision Engineering & Proven Scale
Pioneering low-dew-point environmental control since 2010. Ranked among China's top 3 rotary desiccant dehumidifier manufacturers, operating at gigafactory-scale reliability.
Direct Clean-Room Proven Heritage
Serving global titans such as Tesla, Northvolt, CATL, BYD, and TTI, Hangzhou DryAir brings the world's most unforgiving clean-environment tolerance—down to -70°C dew point—into high-efficiency industrial food and chemical drying equipment.
Comprehensive Turnkey Execution
From psychrometric load calculation and thermodynamic CFD air modeling to fabrication, automated PLC integration, on-site commissioning, and continuous global support, one team guarantees operational KPIs.
Stringent Defense & Export Certifications
Operating under ISO 9001 and China's GJB national military standard systems. Machine units are built to meet CE, UL, CSA, ASME, and EAC standards for seamless deployment worldwide.
Holistic Macro-Industry Drying & Environmental Solutions
How low dew-point engineering addresses critical operational failure points across food processing, pharmaceutical, and high-tech manufacturing.
Agro-Food Powder Processing
Tomatoes, berries, and high-sugar vegetable purees exhibit rapid hygroscopic lump formation under ambient cooling. Our dry air circulation guarantees high solubility, uniform particle mesh (80–120 mesh), and long-term shelf stability without anticaking additives.
Pharmaceutical & Active Excipients
Effervescent tablets, gelatin capsules, and active botanical extracts require strict low RH (10–25%) cleanrooms. Controlled supply air prevents moisture-induced chemical hydrolytic degradation and preserves medicinal bio-potency.
Lithium & Advanced Materials
Gigafactory cell assembly and solid-state electrolyte synthesis require continuous -40°C to -70°C dew point atmospheres to prevent hydrofluoric acid (HF) reactions, setting the benchmark for industrial environmental control.
Global Compliance & Rapid Localization Support
De-risking international capital expenditure through factory-guaranteed conformance, rigorous testing protocols, and lifecycle engineering agreements.
Multi-Jurisdictional Certification
Equipment is pre-engineered for destination compliance: CE (Machinery & Low Voltage Directives), UL 508A electrical panels for North America, CSA conformity for Canada, ASME pressure vessel codes, and EAC certification across Eurasian territories.
Full Factory Acceptance Testing (FAT)
Every dry-type system undergoes rigorous multi-point validation inside our in-house environmental test lab. Psychrometric, thermal, air velocity, and leakage tests are witnessed virtually or on-site prior to ocean shipment.
Optional 2-Year Overseas Service
International clients can secure an extended 24-month lifecycle partnership including remote telemetry diagnostics, rapid spare parts fulfillment, scheduled maintenance, and on-site engineering commissioning.
Technology Roadmap: Next-Gen Industrial Dehydration
Continuous investment in thermodynamic efficiency, predictive IoT control, and green desiccant matrix research.
Hybrid Rotary-Refrigeration
Integration of heat-pump condensing pre-coolers with high-density titanium silicate rotor modules, yielding stable sub-zero dew points at minimal parasitic power draw.
AI Psychrometric Optimization
Predictive load algorithms balancing ambient seasonal humidity fluctuations, dynamically dialing rotor speed and regeneration temperatures to maintain exact residual moisture targets.
Waste-Heat Regeneration Integration
Zero-electric regeneration using waste steam, industrial flue gas, or solar thermal concentrators, slashing operational drying cost per dry kilogram down to historic lows.
Total Solute & Clean Air Recirculation
Complete hermetic closed-loop loop drying, recirculating 98% of inert process air while recovering organic essences, clean water, and pure agro-solids.
Technical & Commercial Procurement FAQ
Comprehensive engineering clarifications addressing operational parameters, delivery scopes, and international standards.
How does low dew point dry-type machinery improve tomato powder quality over conventional spray drying?
What is the minimum dew point Hangzhou DryAir equipment can reliably maintain in round-the-clock operations?
Can DryAir deliver complete turnkey agro-drying cleanrooms and processing plants outside of China?
What certifications are provided for European and North American customs clearance and industrial permits?
How does the NMP recovery and VOC abatement integration relate to food-grade and agricultural powder systems?
What support protocols are available for overseas plants in case of unexpected downtime?
Secondary Deployment: Specialty Dryers, Heat Recovery & Support Units
Complete your production architecture with specialized environmental conditioning, solvent reclaimers, and high-efficiency pre-cooling systems.
DEHUMIDIFICATION
Desiccant Dehumidifier Unit
High-capacity industrial rotor unit engineered for uninterrupted air conditioning in low-humidity food drying and packing zones.
- Sub-zero moisture elimination
- Micro-flute rotor structural stability
CLEAN ENVIRONMENT
Turn-key Dry Room System
Comprehensive environmental enclosure with fully integrated mechanical air handlers, sealing systems, and monitoring controls.
- Air-tight wall panel engineering
- Zero micro-condensation guarantees
SOLVENT YIELD 99%
NMP Recovery System
Engineered for high-volume condensation, absorption, and purification of exhaust solvents with complete automated telemetry.
- Closed-circuit distillation loops
- Strict emissions standard adherence
THERMAL OXIDIZER
VOC Abatement System
High-efficiency regenerative thermal oxidizer and deep-chilling unit eliminating hazardous industrial air pollutants.
- Thermal recovery ceramic beds
- High efficiency odor oxidation
Refrigerative Dehumidifier
Economical bulk moisture extraction for preprocessing facilities, raw agricultural stock rooms, and packing areas.
- Low maintenance compressor cycles
- Rapid sensible cooling balance
 CONDENSATION TECH
Hydrocarbon Vapor Recovery
Deep-refrigeration multi-stage condensation units engineered to intercept high-pressure vapors during chemical loading and storage.
- Explosion-proof ATEX design
- Continuous automatic purge cycles
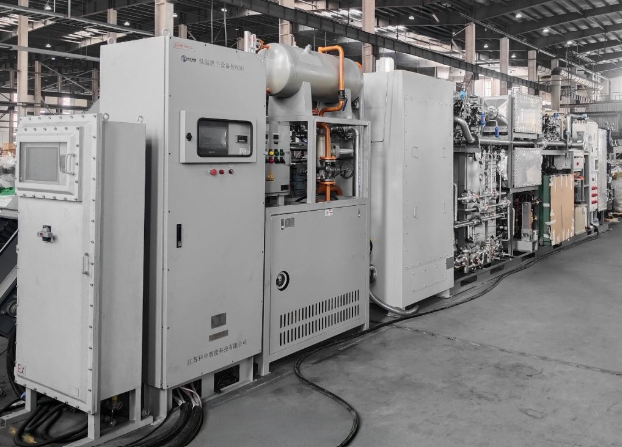 CONTINUOUS FLOW
Continuous Coating Exhaust Plant
Engineered for high-volume automated processing lines requiring constant volumetric exhaust management and dew point stability.
- Real-time concentration sensing
- High operational safety margins
 GMP VALIDATED
Pharma Cleanroom Conditioning
Sanitary stainless-steel dehumidification air systems built to avoid bacterial growth and eliminate hygroscopic sticking.
- Sanitary internal washdown zones
- HEPA terminal filter integration
Connect with Hangzhou DryAir Application Engineers
Whether calculating psychrometric loads for tomato powder spray dry towers or engineering turnkey dry rooms, our senior engineering staff provides complete project validation within one business day.