
 DP -70°C
Desiccant Dehumidifier Unit
Controls atmospheric hygroscopicity in tomato paste spray drying towers and packing suites to eliminate caking.
View SpecificationsExplore our heavy-duty industrial machinery engineered specifically for tomato dry powder manufacturing, dry-type extraction, solvent control, and low-dew-point atmospheric containment.
DP -70°C
Controls atmospheric hygroscopicity in tomato paste spray drying towers and packing suites to eliminate caking.
View Specifications Turnkey EPC
End-to-end sealed dry rooms engineered for ultra-hygroscopic tomato powder blending, conveying, and container filling.
Explore Dry Rooms Recovery ≥99%
Recovers critical extraction solvents utilized in refined tomato oleoresin and active lycopene extraction lines.
Learn Recovery Tech Cooling + RTO
Thermal oxidizer and regenerative systems capturing volatile aromas and production exhaust gases from roasting and drying lines.
View Abatement Tech High Efficiency
High-capacity condensation systems for pre-cooling fresh tomato washing zones and preliminary moisture removal phases.
Check Refrigerative Units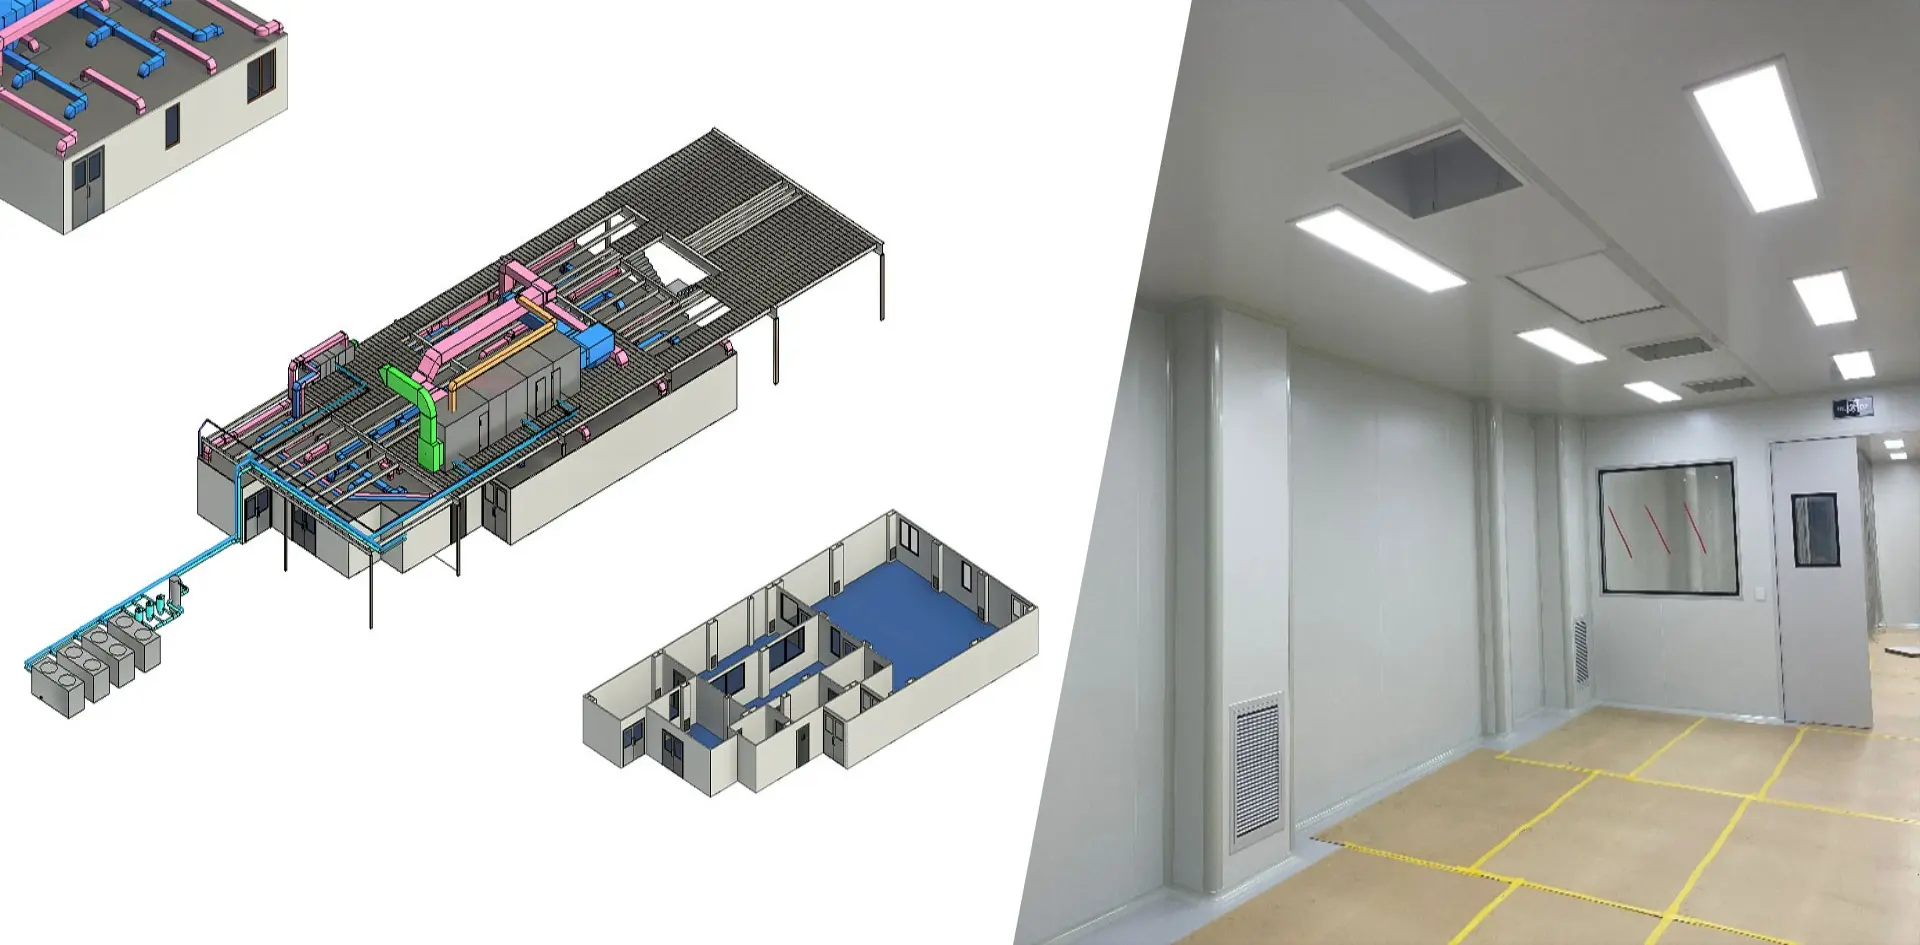 Vacuum Belt Dry
Continuous thermal airflow and desiccant-assisted belt systems drying concentrated tomato paste into instant crystalline flakes.
View Belt Dryers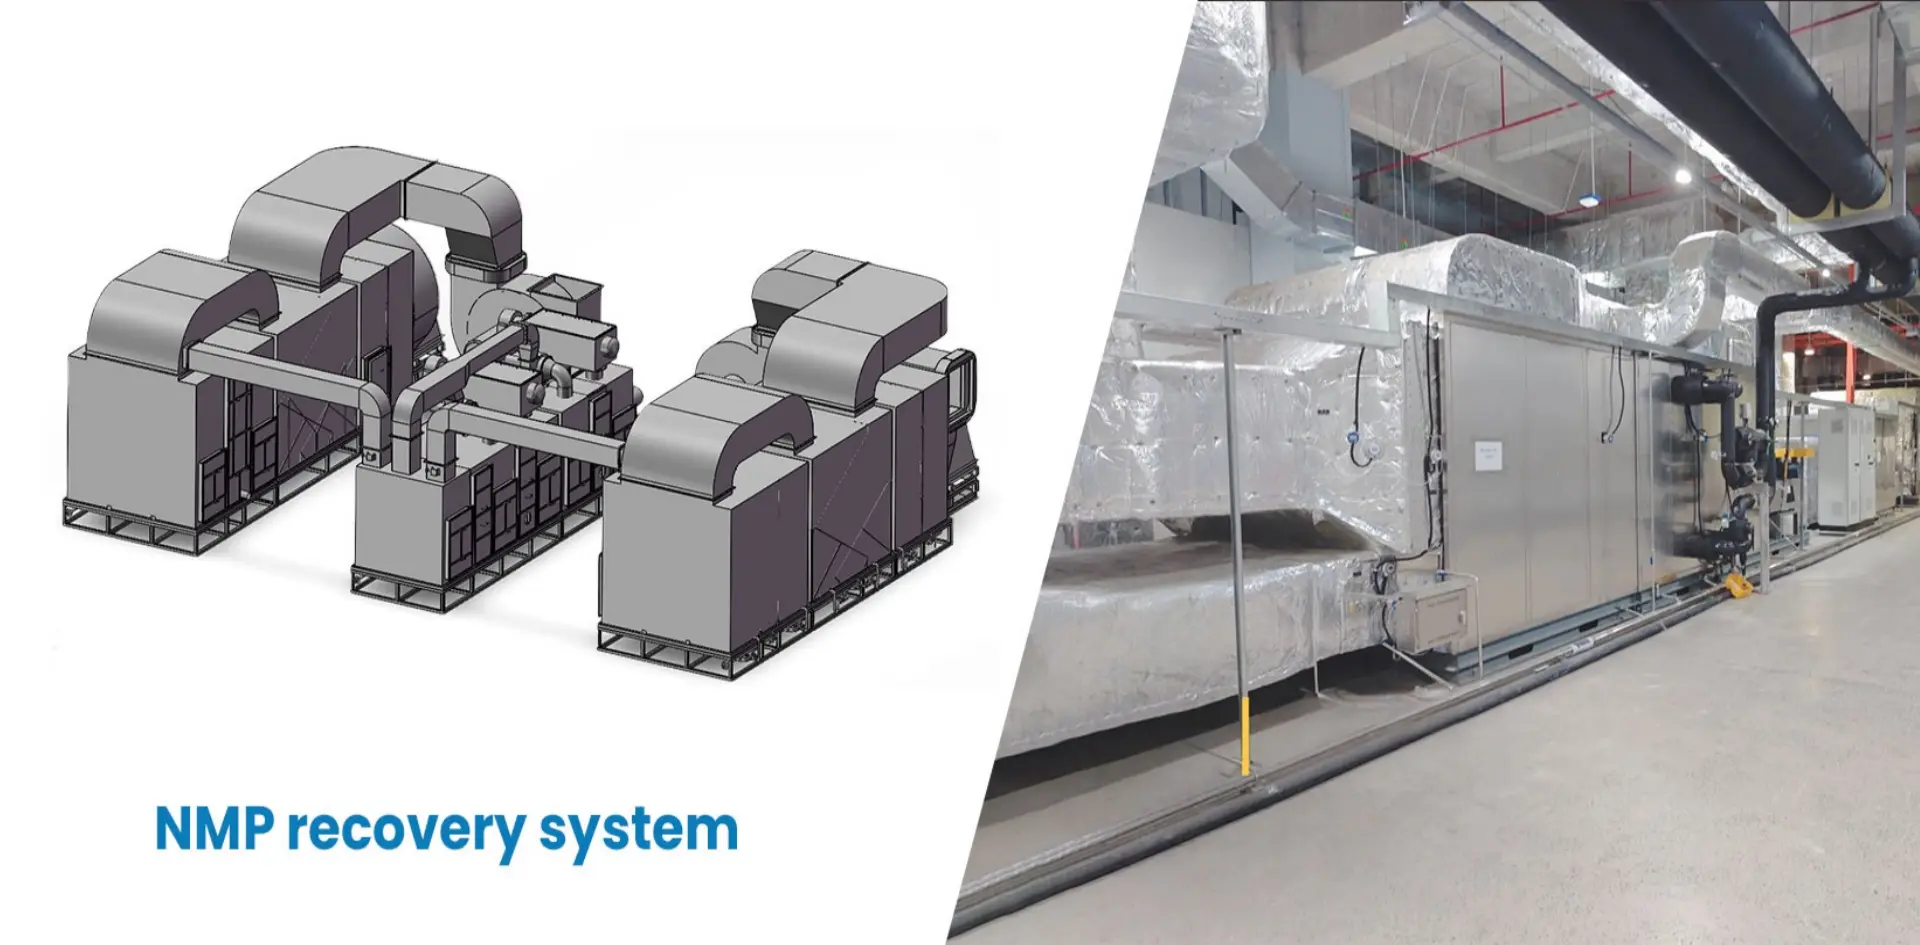 Dehumidified Blast
High-speed centrifugal atomization paired with low-dew-point hot air blasts for producing free-flowing tomato powder.
Get Technical Sheet CIP Integrated
Negative/positive pressure sterile air barriers designed for automated canning and bulk bagging of dehydrated solids.
Request Engineering DataWhy conventional spray and tray dryers fail with high-sugar horticultural commodities, and how dry-type dehumidification systems optimize production yields.
Tomatoes are high in low-molecular-weight sugars (fructose and glucose) and organic acids, which exhibit a remarkably low glass transition temperature (~32°C). In typical drying towers, particles stick instantly to vessel walls as viscous rubbery masses. DryAir dry-type machines feed continuous dehumidified air (-40°C to -70°C dew point) to keep powders below their transition threshold without excessive carrier additives like maltodextrin.
Lycopene, beta-carotene, and natural polyphenols in red tomatoes undergo severe oxidative degradation and isomerization when exposed to prolonged thermal processing (>85°C) in standard dryers. Dry-type continuous vacuum belt dryers and desiccant-enhanced low-temperature towers preserve over 95% of active pigment indices, ensuring natural vibrant coloration and premium nutritional value for demanding buyers.
Dehydrated tomato powder exhibits extreme water vapor sorption isotherms, absorbing moisture within seconds of atmospheric exposure. DryAir supplies complete dry room infrastructure around drying cyclone collectors, vibrating fluid beds, and bagging stations, preventing powder agglomeration, hardening, and package swelling throughout distribution.
Analysis of how top FMCG food conglomerates, condiment manufacturers, and nutraceutical brands assess tomato dry-type equipment suppliers.
International consumers actively avoid starches and artificial anti-caking agents (like silicon dioxide or sodium aluminosilicate). Overseas procurement demands dry-type systems capable of drying 100% pure tomato puree into instant reconstitutable powder without starch carriers. Our precise psychrometric control allows natural purity to command up to a 35% market premium.
Traditional spray towers consume massive thermal loads (up to 4,500 kJ per kg of evaporated water). The latest global buyer tenders demand waste-heat recovery, heat-pump integration, and closed-loop desiccant air regeneration wheels that slash thermal energy consumption by 30% to 45%, qualifying plant owners for green production subsidies.
Automated SCADA controls, AI-driven moisture load compensation, and real-time dew point telemetry are now mandatory specs. Our systems interface seamlessly via Profinet, Modbus, or Ethernet/IP with central plant distributed control systems (DCS), allowing predictive maintenance and continuous process traceability.
Combining tier-one industrial components, robust manufacturing scalability, and rigorous aerospace/military grade standards.
Capturing over 30% market share in critical desiccant drying and low-dew-point environmental systems across China and global industrial parks.
30%+ Market ShareMassive modern manufacturing capacity ensures short lead times even for large agro-industrial expansions and gigafactory-scale cleanrooms.
200+ Sets / MonthLed by 6 Masters & PhDs, 2 National Registered HVAC Engineers, 8 Senior Engineers, and 58 certified industrial technicians.
74 Engineers & TechniciansOperates strict ISO 9001 and Chinese GJB national military defense standards with comprehensive in-house performance test bays.
Military Standard AuditedFrom high-temperature desert cultivation to humid subtropical packaging hubs, our machinery adapts to demanding climatic realities.
Deployment: Xinjiang, Central Asia, Middle East, Southern Europe.
Challenge: Extreme ambient daytime heat with fine abrasive sand loads.
Solution: Dual-stage high-efficiency filtration with integrated heat-pump refrigeration coils to pre-cool air before rotary desiccant processing.
Deployment: Southeast Asia, India, Latin America.
Challenge: Ambient relative humidity exceeding 85% causes instant powder clumping.
Solution: Deep-dew-point DHU desiccant dehumidifiers controlling bagging suites to under 15% RH, ensuring lump-free vacuum hermetic sealing.
Deployment: Industrial paste evaporators converting 28-30° Brix and 36-38° Brix into solids.
Challenge: High viscosity and sticky residue blockage.
Solution: Continuous vacuum belt dryers with precision multi-stage heating zones and automated Clean-In-Place (CIP) fluid circuits.
A benchmark comparison between conventional thermal dryers and DryAir desiccant-enhanced low-temperature systems.
| Performance Parameter | Standard Spray Drying Tower | Conventional Hot-Air Cabinet | DryAir Low-Dew-Point Dry-Type Machine |
|---|---|---|---|
| Operating Inlet Temperature | 160°C – 210°C (High Thermal Stress) | 75°C – 95°C (Long Exposure) | 45°C – 75°C (Low Thermal Degradation) |
| Process Air Dew Point | Uncontrolled Ambient (+15°C to +28°C) | Uncontrolled Ambient (+18°C) | Regulated down to -40°C ~ -70°C DP |
| Wall Caking & Powder Loss | 15% – 25% Loss on chamber walls | Uneven crusting, manual scraping | <1.5% Loss (Chamber Wall Dehumidified) |
| Natural Lycopene Retention | 50% – 65% (Heavy Oxidation) | 40% – 60% (Thermal browning) | 92% – 97% Active Retention |
| Solubility & Dispersion Index | Moderate (Requires Maltodextrin) | Poor (High Insoluble Grain) | Instant Dispersion (Pure Tomato Solids) |
| Operational Energy Recovery | Single pass exhaust (High Loss) | Zero heat recovery | ≥99% Solvent / 35% Heat Wheel Recovery |
How Hangzhou DryAir guarantees full engineering compliance and overseas deployment across international jurisdictions.
All machinery is custom-built and certified to destination standards: CE Machinery Directive & PED for Europe, UL/CSA electrical enclosures for the USA & Canada, ASME pressure vessels, and EAC (CU-TR) certificates for the Eurasian Economic Union.
We deploy senior field service engineers for on-site positioning, piping integration, electrical commissioning, and trial powder runs. Overseas clients can select an optional extended 2-year service agreement with guaranteed rapid-dispatch spare parts.
Our industrial engineering capability is field-tested and audited by elite multinational manufacturing leaders including Tesla, Northvolt, CATL, BYD, EVE Energy, Envision, SVOLT, and TTI, proving process stability where downtime is not tolerated.
Procurement guidance and engineering inquiries answered directly by our chief technical specialists.
Select your required system below to submit your specifications, project layout, and processing capacity requirements directly to our engineering desk.
Supply Air -70°C
Essential for moisture-sensitive tomato powder drying towers and post-process bagging rooms.
View Specifications
Full Turnkey EPC
Full envelope design, insulation panels, dehumidification, and automated balance for food and battery plants.
Explore Dry Rooms
Recovery Rate ≥99%
Captures and purifies process solvent vapors from continuous drying ovens and extraction lines.
Learn More
Thermal Clean
Deep chilling condensation combined with regenerative thermal oxidizers to purify exhaust streams.
Learn More
Pre-Cooling Master
High-efficiency mechanical refrigeration removing bulk moisture ahead of rotary desiccant passes.
Learn More Industrial Scale
Engineered clean environment preventing cross-contamination and moisture pickup for high-purity solids.
Explore Systems GMP Standard
Specifically manufactured for food-contact, pharmaceutical powders, and nutraceutical spray drying lines.
View Specifications Vapor Recovery
Recovers fine volatile organics and aromatics, ensuring strict compliance with local emission thresholds.
Learn MoreProvide your raw material moisture content, hourly output target (kg/h), and local climatic conditions. Our registered HVAC and process engineers deliver comprehensive load calculations and 3D layout proposals within 24 business hours.