
 ≥99% Recovery
Riyadh Industrial NMP Recovery Unit
High-efficiency solvent condensation and Zeolite wheel absorption loops customized for Riyadh battery giga-lines, mitigating toxic N-Methyl-2-pyrrolidone loss.
Learn MoreEngineered for extreme desert ambient conditions up to 55°C, ensuring energy-efficient recovery, zero VOC leaks, and uninterrupted cell electrode production.
≥99% Recovery
High-efficiency solvent condensation and Zeolite wheel absorption loops customized for Riyadh battery giga-lines, mitigating toxic N-Methyl-2-pyrrolidone loss.
Learn More DP -70°C
Dual-rotor desiccant dehumidifiers generating ultra-dry air down to -70°C dew point under heavy Riyadh thermal loads for lithium cell electrolyte filling.
View Specifications Turnkey EPC
End-to-end engineered cleanrooms, structural thermal barriers, low-leak envelope design, and automated HVAC systems for EV manufacturing complexes in KSA.
Explore Dry Rooms Cooling + RTO
Regenerative Thermal Oxidizer (RTO) combined with cryogenic condensation, eliminating VOC emissions across petrochemical hubs in the Riyadh industrial district.
Learn MoreAs Saudi Arabia accelerates towards Vision 2030, Riyadh is rapidly morphing from an oil-dependent metropolis into the Middle East's preeminent high-tech manufacturing, clean energy, and electric vehicle (EV) cluster.
Modern industrial clusters in Riyadh require strict compliance with PME environmental regulations. Implementing an on-site closed-loop NMP recovery system reduces virgin solvent import logistics while lowering production carbon footprints by over 45%.
Summer ambient dry-bulb temperatures in Riyadh frequently surpass 50°C with severe sand particulate storms. DryAir systems integrate advanced sand-filtration and thermodynamic heat recovery circuits that maintain continuous 24/7 condensation stability.
Supporting local manufacturing autonomy in Riyadh. Recovering N-Methyl-2-pyrrolidone solvent at ≥99% purity guarantees supply-chain sovereignty for domestic battery pack assemblers, ESS integrators, and specialty chemical manufacturers in Saudi Arabia.
With global Li-ion battery manufacturing capacity expanding past 3 TWh, solvent management has shifted from a mere emissions requirement to a primary driver of factory EBITDA and operational resilience.
N-Methyl-2-pyrrolidone serves as the universal solvent in lithium-ion cathode slurry processing (specifically PVDF binders). With international petrochemical market fluctuations, the price of virgin NMP presents serious operational cost volatility for gigafactories.
A DryAir recovery system captures and condenses solvent exhaust with a certified ≥99% efficiency rating, drastically diminishing the requirement for continuous virgin raw material procurement and amortizing initial equipment CAPEX in under 14 months.
NMP is categorized as a Substance of Very High Concern (SVHC) under EU REACH and global environmental frameworks due to its reprotoxic properties. Giga-tier battery suppliers entering European, North American, or Gulf Cooperation Council (GCC) markets must demonstrate near-zero atmospheric stack discharge.
Our closed-cycle absorption concentration combined with catalytic polishers guarantees stack emissions drop consistently below ≤1 ppm, far superior to standard global regulatory thresholds.
| Target Application | Key Environmental Constraint | DryAir System Efficiency | Compliance Standards |
|---|---|---|---|
| Battery Cathode Coating | Exhaust NMP concentration 1000–5000 ppm | ≥99.0% Condensation | CE, UL, ASME, GCC-PME |
| Polyimide (PI) Film Plants | High exhaust temperature & solvent loss | ≥99.2% Capture Rate | ISO 14001, ATEX Zone 1 |
| Semiconductor Stripping | Ultra-pure VOC residual management | ≤1 ppm Stack Exhaust | Cleanroom Class 1000, CE |
| Pharma Synthetic Chemistry | Cross-contamination and odors | GMP Closed Loop | FDA, GMP, GJB Certified |
Delivering unmatched engineering rigor, scale, and operational agility to overseas megaprojects across Riyadh, North America, and Europe.
Fully integrated Industry 4.0 digital manufacturing center supports parallel execution for multi-phase gigafactories without delivery schedule slippage.
Ranked among the Top 3 clean-air and solvent recovery manufacturers in China, backed by long-term framework partnerships with CATL, BYD, and EVE.
Proprietary low-dew-point rotor syntheses and thermodynamic recovery algorithms, tested rigorously under demanding ISO 9001 and military-grade GJB regimens.
Multidisciplinary team including HVAC engineers, chemical PhDs, and international EPC project leads with verified gigafactory deployment experience.
End-to-end accountable delivery model eliminating contractor conflicts and ensuring strict dew point and recovery efficiency guarantees.
Evaluating Riyadh ambient temperature profiles, process exhaust flow rates, solvent loading, and ducting schematics.
CFD modeling, psychrometric curve balancing, energy recovery integration, and ATEX/hazardous zone isolation planning.
Modular manufacturing at our Hangzhou center with pre-shipment performance testing inside certified climate test chambers.
On-site assembly, piping hookup, cleanroom envelope sealing, and factory integration overseen by DryAir project engineers.
System fine-tuning, recovery validation (≥99%), SASO documentation signoff, and continuous 2-year overseas technical care.
Versatile atmospheric control and solvent recovery technologies built to protect yield, worker safety, and profitability.
Cathode coating drying ovens vent massive volumes of hot air rich in NMP. Our recovery chillers condense pure liquid solvent while returning cleaned, pre-heated air back into drying chambers, slashing heating energy bills by up to 60%.
Precise moisture-sensitive chemical synthesis requires tight GMP low-humidity envelopes (10%–20% RH). Prevents powder hydration, microbial growth, and active tablet degradation during packaging lines.
Certified environmental protection for avionics, solid-propellant manufacturing, and military munitions depots against high humidity and salt-laden corrosion across Middle Eastern coastal and desert terrains.
Vapor recovery units (VRU) for tank farms and loading terminals in Riyadh and Jubail, combining refrigeration condensation with activated carbon polishing to prevent hazardous hydrocarbon venting.
Sub-ppb airborne molecular contamination control and zero-moisture cleanrooms enabling defect-free wafer fabrication, precision sensor assembly, and optical lens coating.
Preventing frost formation on cooling coils, eliminating slippery floor icing hazards, and preserving dry air integrity in automated deep-freeze logistics hubs.
Determine standard performance parameters and recommended system architectures for your specific process requirements.
| Industrial Process | Moisture / Solvent Threshold | Recommended Technology | Expected ROI Cycle |
|---|---|---|---|
| Li-ion Cell Assembly & Electrolyte Injection | -40°C to -60°C DP | Turnkey Dry Room + DHU Dehumidifier | 12–18 Months |
| Next-Gen Solid State & Lithium Metal | Down to -70°C DP | Ultra-Low Dew Point Rotary System | 8–14 Months |
| Electrode Slurry Coating & Drying | ≥99% Recovery | ZJRH Integrated NMP Recovery Plant | 10–14 Months |
| Hygroscopic Pharmaceutical Packaging | 10%–30% RH | GMP Pharma-Grade Desiccant Unit | 15–20 Months |
| Defense Avionics & Ordnance Depots | ≤40% RH | GJB Standard Environmental Dehumidifiers | Strategic Asset Life |
| Industrial Warehousing & Cold Chain | 45%–60% RH | Refrigerative Commercial Dehumidifiers | 6–12 Months |
Explore our full line of industrial humidity control, solvent condensation, and VOC destruction systems trusted by Fortune 500 manufacturers worldwide.
-70°C DP
DHU series rotary desiccant dehumidifiers deliver stable low-dew-point air where refrigeration alone cannot reach.
View Specifications
≥99% Efficiency
Captures N-Methyl-2-pyrrolidone from electrode coater exhaust for high-purity recycling, slashing VOC spend.
Learn More
Turnkey EPC
Complete humidity-controlled cleanrooms — enclosure, air handlers, filtration, controls, and commissioning.
Explore Dry Rooms
Cooling + RTO
Deep-cooling condensation combined with regenerative thermal oxidation to treat VOC waste gas streams.
Learn More Energy Efficient
Cost-effective moisture removal for industrial warehouses, workshops, and pre-cooling stages ahead of dry rooms.
Learn More Vapor Recovery
Heavy vapor extraction and solvent recovery for fuel terminals, petrochemical handling, and tank storage.
Learn More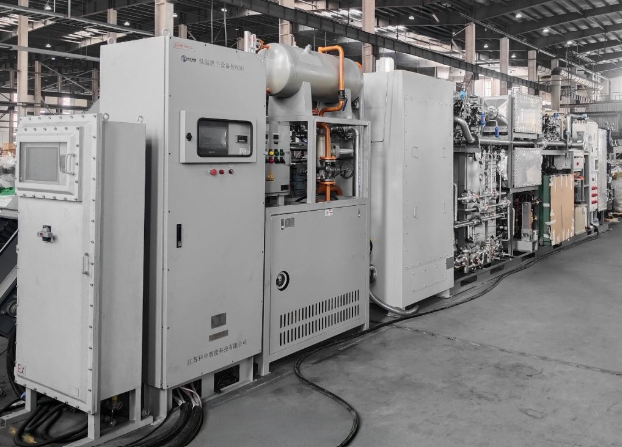 Clean Air
High-efficiency closed air recirculation system specifically built for round-the-clock roll-to-roll electrode coaters.
Learn More Gigafactory Spec
Engineered, pre-tested, and rapid-deployment dry room units designed for fast-track battery expansion phases.
Explore Dry RoomsClear technical, logistical, and commercial answers for EPC consultants, factory owners, and procurement directors.
Submit your process exhaust volume, target dew points, and site parameters. Our HVAC & chemical engineering team returns a customized system design and ROI calculation within 24 hours.