
 DP -70°C Control
Desiccant Dehumidifier (Oman Project Ready)
Rotary desiccant systems engineered to maintain extreme low dew points down to -70°C for sensitive lithium battery cell assembly lines and specialized chemical laboratories.
Engineered for Oman's Vision 2040 industrial decarbonization and Middle Eastern battery cathode & synthetic resin infrastructure. Delivering verified ≥99% NMP solvent recovery rates, minimal lifecycle carbon footprints, and robust operation in high-salinity desert environments.
Pre-engineered, modular process installations deployed globally for advanced battery manufacturing, specialty polymer condensation, and clean energy storage.
DP -70°C Control
Rotary desiccant systems engineered to maintain extreme low dew points down to -70°C for sensitive lithium battery cell assembly lines and specialized chemical laboratories.
 EPC Turnkey
End-to-end industrial clean dry room execution combining structural envelope design, precision HVAC zoning, dew point verification, and smart microclimate automation.
 Efficiency ≥99%
Multi-stage condensation, chilled water scrubbers, and zeolite wheel concentration reclaiming over 99% pure N-Methyl-2-pyrrolidone from coater exhausts.
 Cooling + RTO
Deep-cooling cryo-condensation integrated with regenerative thermal oxidizers (RTO) for rigorous emission control in industrial zones and chemical refining complexes.
As Oman vigorously accelerates its Vision 2040 roadmap toward non-oil revenue growth and industrial sustainability, industrial economic hubs such as the Special Economic Zone at Duqm (SEZAD), the Sohar Port and Freezone, and the Salalah Free Zone are actively expanding into downstream petrochemicals, advanced membranes, specialty coatings, and clean-tech energy storage components.
N-Methyl-2-pyrrolidone (NMP, C₅H₉NO) is an essential, high-boiling polar aprotic solvent extensively utilized across lithium-ion battery electrode slurry production, aromatic extraction, membrane spinning, and electronic insulator coatings. However, due to strict international chemical classifications concerning reproductive toxicity and Oman’s tightening Ministry of Energy and Minerals environmental mandates, unmitigated emissions represent both a profound compliance hazard and heavy financial waste.
Given the escalating cost of virgin NMP solvent on the international commodity exchange ($2,800 to $4,500/MT depending on purity), an electrode coating line operating in Oman without high-efficiency solvent recovery incurs enormous recurring OPEX.
A standard 20,000 m³/h air exhaust volume carrying 1,200 ppm NMP yields over 1.8 tons of recoverable solvent per 24 hours, guaranteeing complete equipment CAPEX amortization in less than 9 to 14 months of steady-state operation.
Combining 15+ years of specialized low dew point desiccant and VOC recovery engineering with unmatched scale, tier-1 gigafactory experience, and rigorous international certification.
We are validated supplier partners to CATL, BYD, EVE Energy, SVOLT, ATL, and international tier-1 gigafactories including Tesla, Northvolt, and TTI. We understand the stringent zero-downtime tolerance of round-the-clock lines.
By employing proprietary multi-stage chiller economizers combined with continuous-adsorption VOC rotor concentrators, our closed-loop units capture ≥99% NMP while maintaining exhaust VOC stack concentrations below 10 mg/m³.
Full compliance with ASME pressure vessel directives, CE Machinery / ATEX explosion-proof certification, UL508A electrical safety codes, CSA, and EAC guarantees risk-free integration into multinational industrial operations.
Our patent-engineered thermal integration systems redirect waste heat from coater exhausts directly into desiccant regeneration and distillation columns, slashing overall plant electricity consumption by up to 35%.
From process simulations and CFD aerodynamic layout design to automated PLC controls and on-site validation by our 74+ dedicated research and field engineers, we own project execution without subcontractors.
Overseas project support with available two-year on-site service warranties, rapid air-freight spare parts distribution, and secure 24/7 cloud-based IoT remote performance monitoring for our Middle East partners.
Review the comparative advantages of DryAir closed-loop multi-stage condensation vs traditional single-stage wet scrubbing systems in hot arid climates.
| Performance Metrics | DryAir Integrated Multi-Stage Condensation + Zeolite Wheel | Conventional Wet Water Scrubber Systems | Direct Incineration / Thermal RTO Only |
|---|---|---|---|
| Solvent Recovery Efficiency | ≥ 99.0% (Liquid NMP Reclaimed) | 80% – 88% (Dilute Wastewater) | 0% (Completely Destroyed) |
| Clean Air Recirculation | Yes (Up to 80% heated dry air return to coater) | No (Full ambient fresh air make-up required) | No (Exhausted to atmosphere) |
| Fresh Water Consumption | Near Zero (Closed circuit chilling) | Very High (Heavy continuous water makeup) | None |
| Middle East Desert Suitability | Optimized with anti-corrosion condenser fin coats | High scaling risks under hard Omani water | Extreme fuel consumption in ambient heat |
| Net Operating Cost (OPEX) | Negative Net OPEX (Major profits from solvent reuse) | High (Massive distillation & wastewater disposal cost) | Severe (High ongoing natural gas/diesel usage) |
Send our process team your coater exhaust airflow rates (m³/h), solvent loading (g/m³), and cooling utility constraints.
Comprehensive engineering insights into system design, installation reliability, and international after-sales support.
Explore our validated product series for precision moisture extraction, solvent condensation, and volatile organic compound abatement.
DHU Series
High-efficiency honeycomb rotor moisture removal delivering continuous ultra-dry supply air down to -70°C dew point for critical production cells.
Custom Cleanroom
Comprehensive turnkey humidity-sealed cleanroom envelopes with integrated multi-zone AHUs and precision dew point stability.
ZJRH Series
Dual-stage condensing scrubbers and zeolite rotors delivering ≥99% solvent reclamation with closed-loop energy-recovery air reheating.
JEN Series
Deep-cooling condensation coupled with multi-chamber regenerative thermal oxidizers to scrub toxic vapors in full environmental compliance.
Robust mechanical DX cooling systems engineered for preliminary air dehumidification in warehouses, logistics centers, and prep rooms.
 Hazardous Area
Vapor recovery units (VRU) capturing volatile hydrocarbon emissions during fuel terminal offloading, tankers, and bulk storage transfers.
 Battery Line OEM
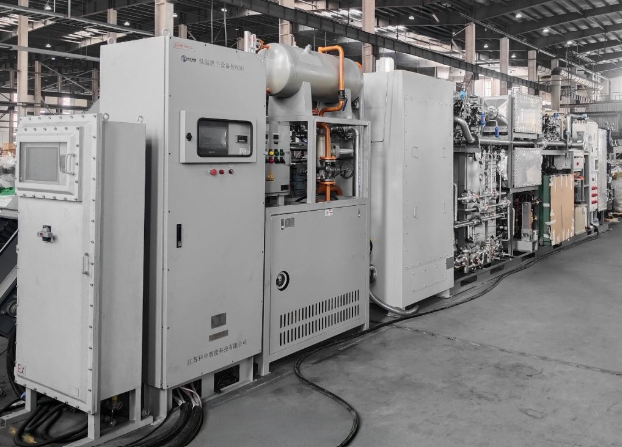
Specialized coater-integrated condensation modules designed to recycle hot solvent-laden air while maintaining oven pressure equilibrium.
 GMP / Pharma Spec
Strict sanitary design dehumidification packages controlling hygiene, micro-particles, and precise humidity for gelatin capsule and effervescent tablet lines.
Partner with Hangzhou DryAir to secure guaranteed recovery benchmarks (≥99%), cut virgin chemical expenditures, and ensure full compliance with regional emission standards.