
 DRE ≥ 99.2%
VOC Abatement System
JEN series deep-cooling condensation and regenerative thermal oxidizers (RTO) for extreme emission compliance.
- Dual-bed & Rotary RTO topologies
- Low operating fuel penalty
Fully compliant with international and local NEMA Kenya emission guidelines, certified under CE, UL, CSA, ASME, and EAC standards.
DRE ≥ 99.2%
JEN series deep-cooling condensation and regenerative thermal oxidizers (RTO) for extreme emission compliance.
 DP -70°C
Rotary sorption dehumidification systems for sensitive pharmaceutical and industrial manufacturing processes.
 Full EPC
End-to-end climate controlled enclosures designed for cleanrooms and battery pack assembly lines.
 Recovery ≥99%
ZJRH series organic solvent recovery unit reclaiming expensive process chemicals from gas streams.
Accelerating environmental monitoring by the National Environment Management Authority (NEMA) requires scalable, energy-lean emission control infrastructure.
Kenya is rapidly positioning itself as East Africa’s industrial hub, underpinned by special economic zones (SEZs) in Dongo Kundu (Mombasa) and Naivasha. Key drivers—including printing, flexible packaging, chemical blending, agrochemical synthesis, and pharmaceutical compounding—generate substantial volatile organic compounds such as toluene, ethyl acetate, MEK, and benzene derivatives.
As standard regulatory pressures escalate, manufacturing facilities situated near residential perimeters in Nairobi’s Industrial Area and Athi River face stringent air quality standards under the Environmental Management and Co-ordination (Air Quality) Regulations.
Industrial electricity and LPG costs in Kenya demand that environmental equipment operate with extreme thermal efficiency. Hangzhou DryAir engineers our Regenerative Thermal Oxidizers (RTO) with specialized ceramic heat exchangers achieving thermal energy recovery (TER) efficiencies greater than 95%. When VOC concentrations exceed 1.5–2.0 g/Nm³, the system enters a self-sustaining autothermal state, eliminating fossil fuel consumption during ongoing production.
Deployments in coastal Mombasa require specialized material selections due to aggressive chloride-laden maritime atmospheric conditions, which can quickly degrade conventional carbon steel ductwork. We offer 316L stainless steel linings, C5-M grade marine protective coatings, and hermetically sealed valve actuators designed to ensure uninterrupted 24/7 duty cycles in humid tropical settings.
Historically, Kenyan operations relied on single-use granular activated carbon (GAC) beds. However, surging hazardous disposal tariffs, freight costs for imported virgin media, and low humidity-dependent capture rates have made operational expenditures unsustainable. Thermal oxidation directly destroys hazardous emissions at the exhaust stack, creating clean CO₂ and H₂O without solid waste generation.
Configured specifically to match volatile load compositions, process flow rates, and plant-level thermal integration constraints.
Operates at 760°C to 850°C, utilizing multi-bed structured ceramic media beds to deliver >99.2% VOC destruction removal efficiency (DRE). Designed with zero-leakage hydraulic poppet valves to prevent fugitive bypassing.
Engineered for high-concentration, single-solvent streams. Progressively lowers exhaust temperature below dew-point thresholds via multi-stage refrigeration circuits, yielding reclaimed liquid solvents with minimal residual emissions.
Transforms high-volume, low-concentration exhaust into a compact, high-concentration stream. Compresses volume by up to 20:1, allowing operators to run a substantially smaller oxidizer, slashing electrical and fuel footprints.
Engineered to resolve exact VOC compositions across divergent production processes.
| Target Sector in Kenya | Primary VOC Species | System Architecture | Observed Emission Performance |
|---|---|---|---|
| Flexible Packaging & Rotogravure Printing | Ethyl Acetate, Isopropanol, MEK, Ethanol | Zeolite Concentration Concentrator + Rotary RTO | Exhaust < 20 mg/Nm³ Total Organic Carbon (TOC) |
| Paints, Resins & Industrial Coatings | Xylene, Toluene, Styrene, Mineral Spirits | 3-Bed Ceramic Matrix RTO + Thermal Waste Heat Boiler | Zero visible odor threshold at boundary lines |
| Pharmaceutical Chemical Synthesis | Dichloromethane, Methanol, Acetone, Hexane | Cryogenic Condensation + Scrubber Integration | ≥99.5% solvent recovery on saturated process lines |
| Fuel Terminals & Bitumen Storage (Mombasa) | Aliphatic Hydrocarbons, BTEX Compounds | Vapor Recovery Unit (VRU) + Refrigerated Condensation | Emission containment matching IFC / World Bank EHS standards |
Hangzhou DryAir delivers heavy-duty environmental and climate control hardware engineered under verified quality architectures.
Certified under ISO 9001 and the demanding GJB national military standard system. Export equipment matches European CE directives, UL standards, CSA guidelines, EAC documentation, and ASME boiler/pressure vessel requirements.
Each unit features integrated Edge computing controllers capable of streaming pressure drop, chamber temperature, and combustion status to our operations dashboard, allowing seamless remote diagnostic oversight for teams in Kenya.
Our Lin'an facility features a fully instrumented testing laboratory. Every thermal oxidizer valve assembly, PLC burner sequence, and desiccant rotor undergoes complete aerodynamic and functional firing trials before crating.
Bridging global equipment precision with localized installation workflows across the East African Community.
We manage direct sea freight logistics routed through the Kilindini Harbour in Mombasa. Systems are engineered using modular skid layouts, fitting standard flat-rack and high-cube shipping containers to prevent oversize freight tariffs and simplify inland haulage via the Standard Gauge Railway (SGR) to Nairobi Inland Container Depot (ICD).
Our engineering support services deliver thorough air dispersion modeling datasets, stack exhaust calculations, and emission balance sheets. We provide all the necessary documentation required by lead environmental experts during Environmental and Social Impact Assessment (ESIA) filings with NEMA.
DryAir dispatches experienced field engineers to direct civil coordination, mechanical hookup, refractory curing, and cold/hot commissioning on-site in Kenya. We run structured training modules for your internal facility maintenance personnel.
International clients can secure our optional comprehensive two-year service warranty plan. This includes scheduled preventative audit visits, prioritized regional spares stock, and direct hotline access to our senior automation engineers.
Explore our complete export line engineered for extreme thermal efficiency, cleanroom consistency, and environmental compliance.
High Efficiency
Industrial rotary desiccant units built for extreme process moisture control in varied industrial manufacturing setups.
View Dehumidifier Specs
Modular Enclosure
Integrated low-dew-point environmental dry rooms for pharmaceutical packaging and precision manufacturing.
View Dry Room Specs
Clean Stream
Solvent recovery setups operating at exceptional recovery performance on continuous processing lines.
View Recovery Specs
RTO Oxidizer
Regenerative thermal oxidizers that break down challenging industrial volatile compounds cleanly.
View Abatement Specs Mechanical Chill
Cost-effective moisture extraction for seed storage, agrochemical facilities, and pre-cooling cycles.
View Chiller Specs Dew Point -50°C
Scalable clean-air environments designed for advanced energy-storage component production lines.
View Battery Spec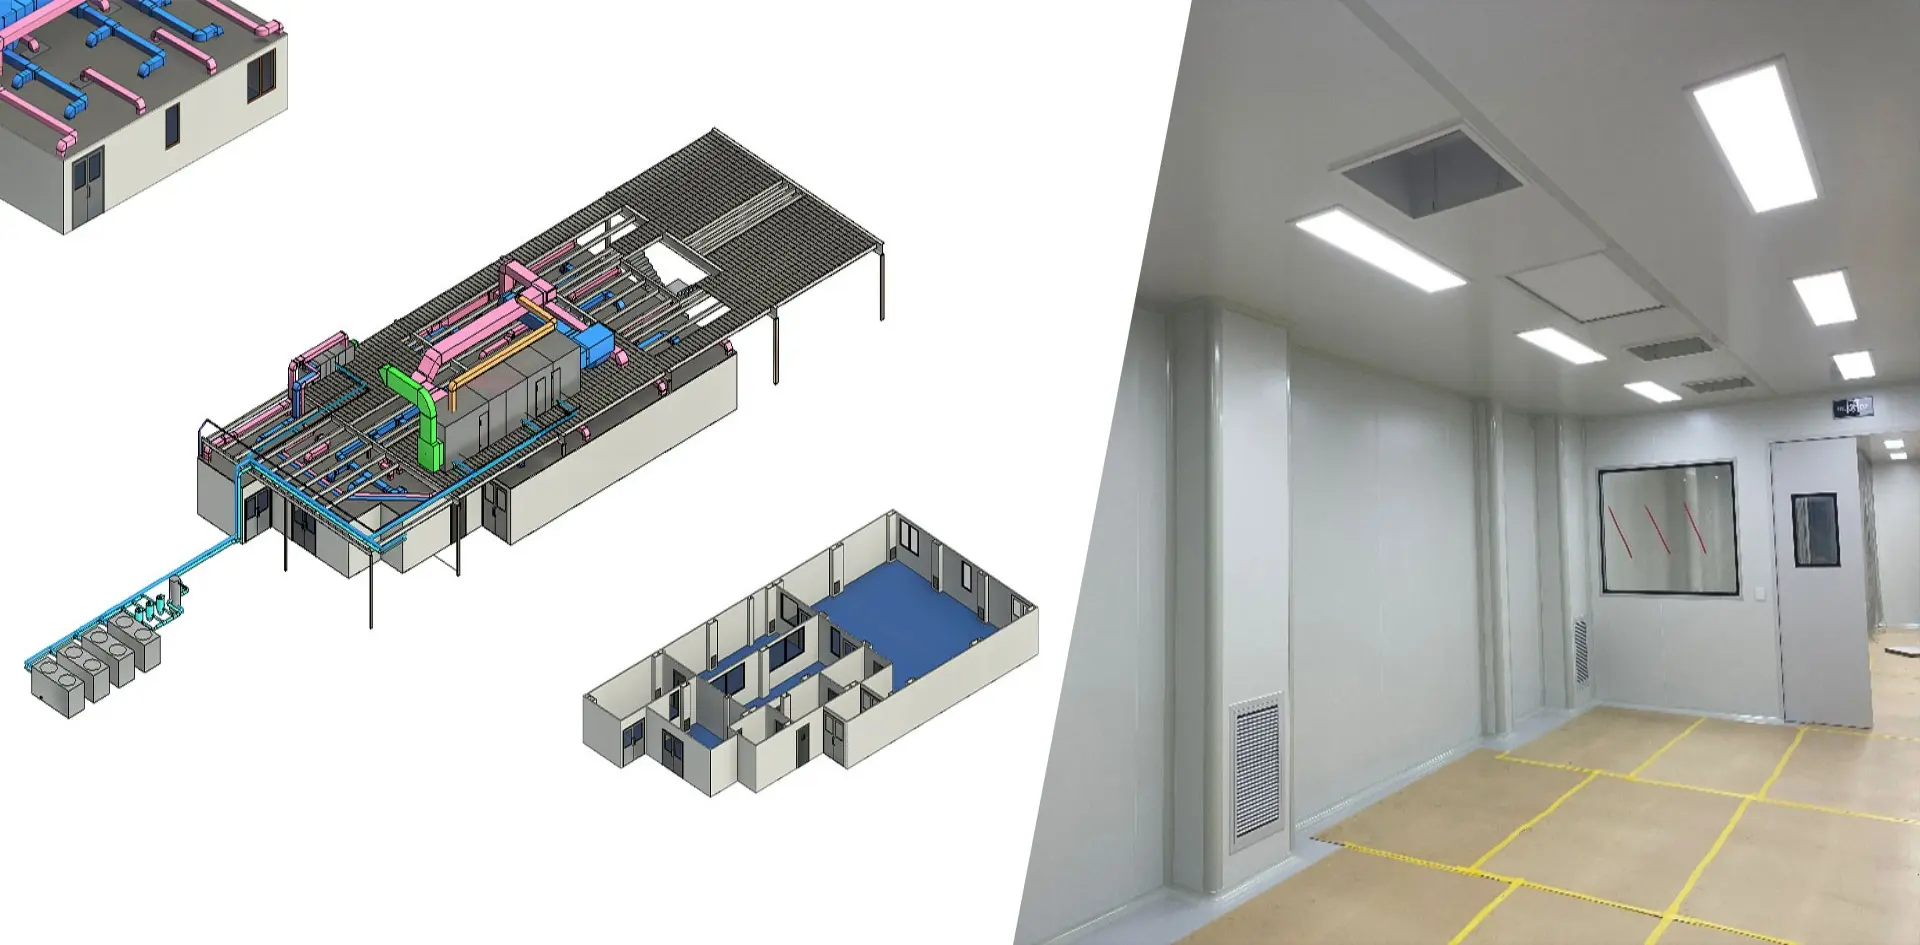 Closed Loop
Dual-stage exhaust purification units designed to eliminate volatile emissions from drying ovens.
View Exhaust Specs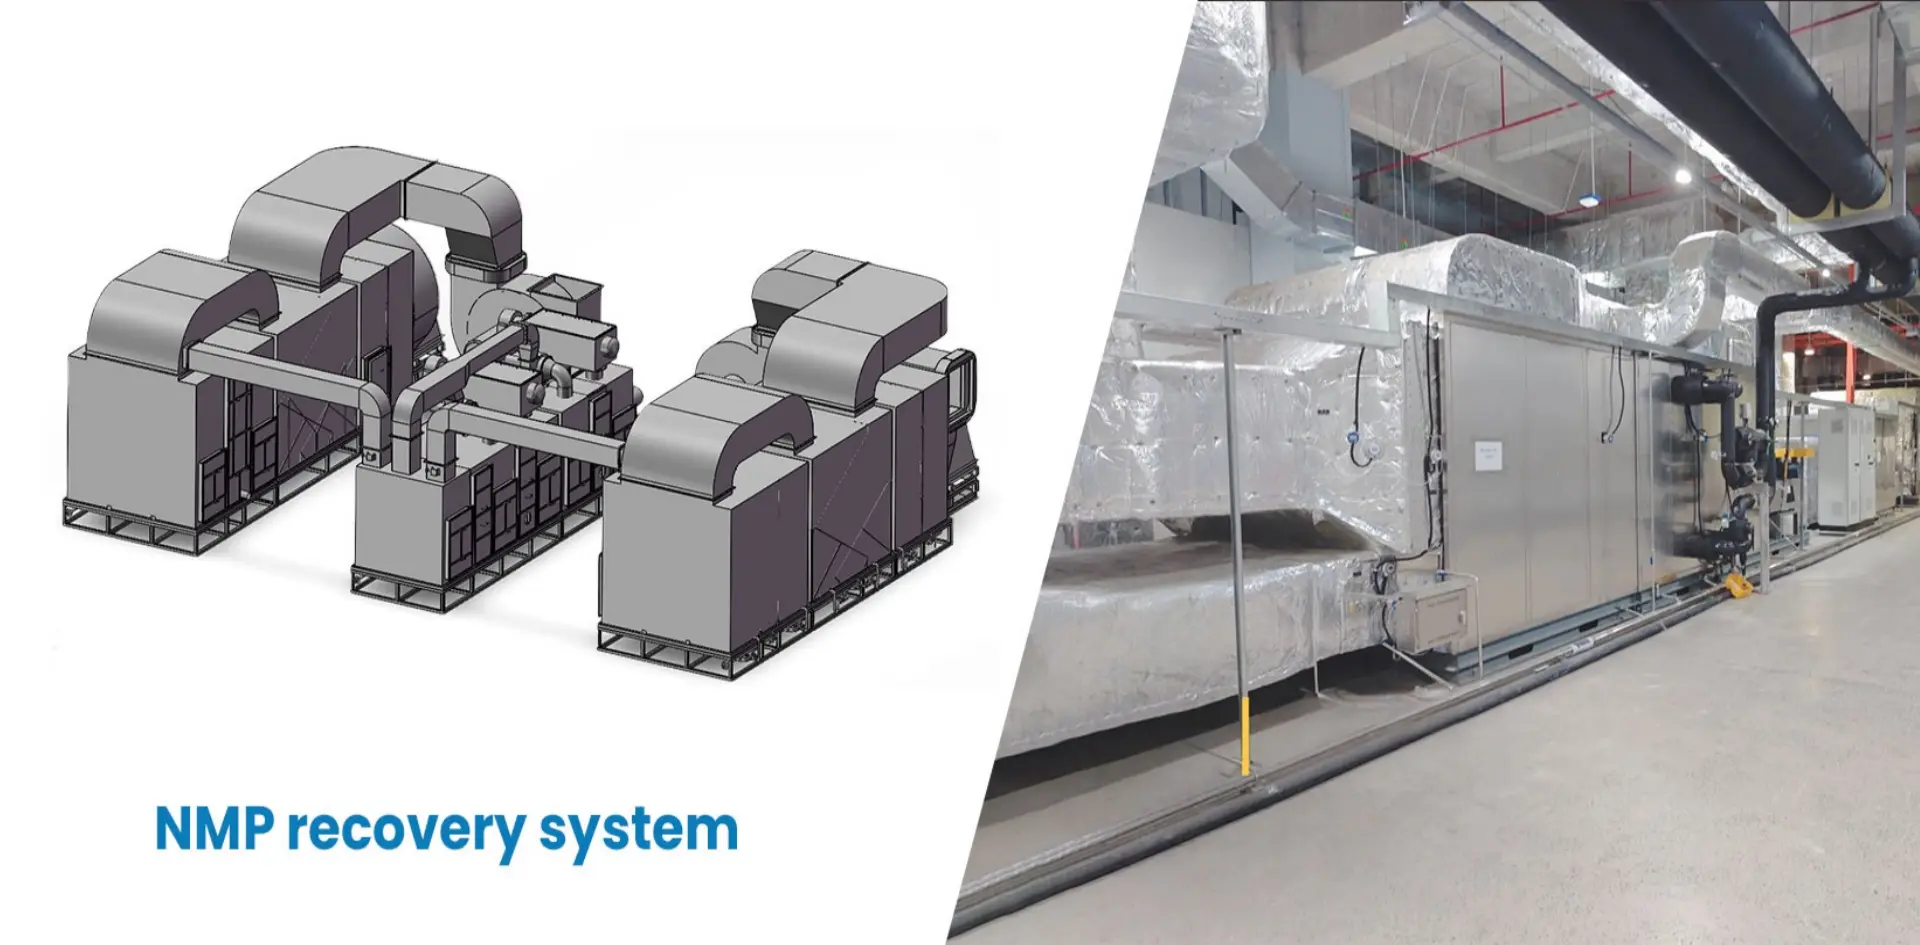 Hybrid Tech
Integrated mechanical deep chilling coupled with oxidation beds for complex chemical compound streams.
View Hybrid SpecsDirect technical guidance on selection, import clearances, and field operation.
Connect directly with our process engineering teams for complete VOC load sizing, equipment footprint studies, and preliminary quotation models.