Direct China Engineering & Turnkey Manufacturing

VOC Abatement System Factory & in China Serving the Czech Republic Market

High-efficiency Regenerative Thermal Oxidizers (RTO), Zeolite Rotor Concentration & Cryogenic Recovery Engineered to Meet Strict EU Industrial Emissions Directives (IED) and Czech Clean Air Act (Zákon č. 201/2012 Sb.).

Send Inquiry Now → Download Czech Technical Dossier
TESLA GIGA BERLIN & AUSTIN NORTHVOLT ETTO CATL CONTEMPORARY AMPEREX ŠKODA AUTO TIER-1 ECOSYSTEM BYD AUTO & BATTERY ATL AMPEREX EVE ENERGY FARASIS ENERGY ENVISION AESC SVOLT ENERGY TTI TECHTRONIC TESLA GIGA BERLIN & AUSTIN NORTHVOLT ETTO CATL CONTEMPORARY AMPEREX ŠKODA AUTO TIER-1 ECOSYSTEM BYD AUTO & BATTERY ATL AMPEREX EVE ENERGY FARASIS ENERGY ENVISION AESC SVOLT ENERGY TTI TECHTRONIC
Engineered Systems for Central Europe

Core Abatement & Climate Solutions for Czech Industry

Certified Chinese manufacturing meeting European CE, ATEX, and EN 12753 environmental engineering norms.

Industrial VOC Abatement System for Czech Chemical and Automotive Plants DRE >99.5%

VOC Abatement System (Czech Industry Series)

Integrated deep-cooling condensation, hydrophobic zeolite rotor concentration, and 3-bed Regenerative Thermal Oxidation (RTO) designed for paint shops and chemical syntheses.

  • Czech Clean Air Act 201/2012 Coll. compliant
  • Self-sustaining auto-thermal concentration

Explore VOC System →
Lithium Battery NMP Solvent Recovery System for Central European Gigafactories Recovery ≥99%

NMP Recovery System (Gigafactory Spec)

Engineered for lithium-ion battery electrode coating lines. Closed-loop chilled water condensation recovering ultrapure N-Methyl-2-pyrrolidone solvent while cutting VOC exhaust to negligible levels.

  • Solvent reuse purity matching fresh raw material
  • Exhaust VOC <20 mg/Nm³ BAT compliance
Explore NMP Recovery →
Rotary Desiccant Dehumidifier Unit for Czech Manufacturing Dew Point -70°C

Desiccant Dehumidifier (DHU Series)

Heavy-duty rotary silica gel and molecular sieve dehumidifiers supplying deep dry air down to -70°C dew point for lithium cell production, defense munitions, and Czech pharmaceutical plants.

  • Waste heat & steam regeneration options
  • EN 1886 standard structural casing
Explore Dehumidifiers →
Turn-key Lithium Battery Dry Room Project Delivered to Europe Turnkey EPC

Turn-key Dry Room System (Full EPC)

Single-source design, modular insulated enclosure construction, ultra-low dew point HVAC, VOC extraction, and European commissioning under unified ISO 9001 and GJB quality governance.

  • Complete architectural air-tight sealing
  • Validated for gigawatt-scale production
Explore Turnkey Systems →
Strategic Market Analysis

Industrial Modernization & Air Pollution Governance in the Czech Republic

Navigating stringent European environmental legislation, rising Central European natural gas tariffs, and cross-border clean technology integration from China.

The Czech Industrial Landscape: Automotive, Chemical & Emerging Cleantech

The Czech Republic stands as one of Central and Eastern Europe's preeminent manufacturing powerhouses. With manufacturing contributing roughly 25% to national GDP—the highest ratio across the European Union—the country's economic spine is heavily concentrated across automotive manufacturing (centered in Mladá Boleslav, Kvasiny, and Kolín), chemical and polymer synthesis (the Ústí nad Labem and Pardubice petrochemical clusters), heavy engineering in Moravia-Silesia, and high-precision pharmaceutical formulations around Prague and Brno.

However, this intensive industrial concentration brings unprecedented emissions compliance pressures. Facilities releasing volatile organic compounds (VOCs)—including toluene, xylene, ethyl acetate, isopropanol, styrene, and toxic N-Methyl-2-pyrrolidone (NMP)—face scrutiny from the Czech Environmental Inspectorate (Česká inspekce životního prostředí - ČIŽP) and regional public health authorities.

With national statutory caps mandated by Act No. 201/2012 Coll. on Air Protection and the overarching European Union Industrial Emissions Directive (IED 2010/75/EU), standard legacy abatement technologies like open-flame flares or single-pass non-regenerative carbon beds are economically and legally non-viable. Plant operators require industrial-scale, thermally efficient VOC abatement solutions that pair proven sub-20 mg/Nm³ total organic carbon (TOC) destruction with minimal secondary CO₂ emissions.

Czech Regulatory Compliance Benchmarks (IED & BAT-AEL)

Act No. 201/2012 Coll. (Zákon o ochraně ovzduší): Sets statutory emission limit values (ELVs) for total volatile organic compounds, demanding continuous real-time monitoring and reporting to national registers (ISPOP).

Surface Treatment BAT Conclusions (STS BREF): Mandates that automated industrial coating and drying processes achieve stack emissions under 20 mg TOC/Nm³ (or 50 mg/Nm³ for complex legacy retrofits).

EU Chemical Strategy for Sustainability & REACH: Places intense regulatory restrictions on reprotoxic solvents like NMP, driving factories to implement solvent recovery loops exceeding ≥99% reclamation yield.

European Energy Efficiency Directive (EED): Central European natural gas price spikes demand Regenerative Thermal Oxidizers with thermal energy recovery efficiencies of ≥95–97%, cutting auxiliary burner fuel consumption to zero under steady solvent load.

Automotive OEM & Tier-1 Coating

Automated paint booths in Central Bohemia generating enormous air volumes (50,000–300,000 Nm³/h) with low-to-medium solvent concentrations. Solved via high-ratio Zeolite Concentration Rotors paired with compact 3-Bed RTO systems.

Chemical Synthesis & Resins

Petrochemical, synthetic resin, and bulk drug manufacturing plants along the Elbe River basin discharging complex, chlorinated, or fluctuating solvent mixtures. Addressed with corrosion-resistant Hastelloy/ceramic oxidizer cores.

Lithium Battery Gigafactories

Electrode slurry drying requiring massive N-Methyl-2-pyrrolidone extraction. Turnkey integration combining multi-stage cooling condensation, chilled recycling loops, and residual polishing oxidizers to safeguard worker health and meet EU battery regulations.

Proprietary Technology Portfolio

Engineering Blueprint: Next-Generation VOC Abatement Methodologies

DryAir's Hangzhou manufacturing center synthesizes advanced thermal thermodynamic engineering, non-combustible hydrophobic zeolite matrices, and precision low-leak poppet valve systems.

1

3-Bed Regenerative Thermal Oxidation (RTO)

The cornerstone of heavy industrial VOC destruction. The process channels raw solvent-laden air through structured ceramic structured packing media preheated from previous cycles. As exhaust reaches the central combustion chamber (820°C–870°C), organic compounds oxidize into benign H₂O and CO₂ with a residence time >1.0 second.

  • Destruction Removal Efficiency (DRE): Guaranteed ≥99.5% through zero-leakage pneumatic poppet valves.
  • Thermal Energy Recovery (TER): 95%–97% efficiency, allowing self-sustaining auto-thermal operation when VOC concentration reaches >1.5–2.0 g/Nm³ (no fuel gas consumption).
  • Low NOₓ Burner Systems: Staged combustion burners compliant with EU Stage V emission limits.
2

Zeolite Concentration Rotor + Auxiliary RTO

Engineered specifically for low-concentration, high-volume air streams typical in automotive painting, furniture spray finishing, and semiconductor cleanroom venting. The hydrophobic zeolite rotor adsorbs VOCs from enormous volumetric flows, which are then desorbed using a low-volume hot air stream (concentration ratio: 10:1 to 30:1).

  • CAPEX & OPEX Reduction: Reduces the volumetric sizing of the subsequent thermal oxidizer by up to 90%, plummeting plant natural gas consumption.
  • High-Temperature Hydrophobic Matrix: Eliminates water vapor competition up to 85% relative humidity; 100% non-combustible inorganic structure preventing thermal runaway fires.
3

Cryogenic Deep-Cooling Condensation & Solvent Recovery

When treating high-boiling solvents or recovering expensive raw materials such as NMP in lithium battery plants or gasoline vapor in tank farms, thermal destruction represents a financial loss. DryAir's multi-stage refrigeration condenser progressively cools gas streams from ambient to 5°C, -15°C, and down to -40°C.

  • Reclamation Purity: Recovers high-purity liquid solvent suitable for direct closed-loop reintroduction into coating lines.
  • Explosion-Proof Design: Full ATEX Zone 1 / Zone 2 certification with inert nitrogen blanket control and continuous LEL sensors.
4

Regenerative Catalytic Oxidizer (RCO) Solutions

For manufacturing processes with VOC streams containing halogen-free, non-silicon compounds, DryAir's RCO systems incorporate precious metal catalysts (Pt/Pd honeycomb) over ceramic beds, dropping the oxidation initiation temperature from 800°C to 280°C–350°C.

  • Ultralow Energy Demand: Self-heating achieved at concentrations as low as 0.7 g/Nm³.
  • Carbon Neutral Footprint: Drastically suppresses plant scope-1 CO₂ emissions relative to thermal combustion.
System Architecture Applicable Air Volume (Nm³/h) Typical VOC Inlet Concentration Destruction / Recovery Efficiency Thermal Efficiency (TER) Compliance Target
3-Bed RTO (Regenerative Thermal Oxidizer) 10,000 – 150,000 1.5 – 10.0 g/Nm³ ≥ 99.5% DRE 95% – 97% BAT-AEL < 20 mg TOC/Nm³
Zeolite Rotor + Catalytic / RTO System 30,000 – 300,000+ 0.1 – 1.2 g/Nm³ (Dilute) ≥ 98.5% System DRE Auto-thermal after enrichment Czech Act No. 201/2012 Coll.
Cryogenic Condensation (NMP / Hydrocarbon) 2,000 – 50,000 High concentration (>15 g/Nm³) ≥ 99.0% Recovery Heat pump integration Circular Economy & REACH
Regenerative Catalytic Oxidizer (RCO) 5,000 – 60,000 0.8 – 4.0 g/Nm³ ≥ 99.0% DRE 93% – 96% @ 300°C Low-Carbon ESG Mandates
International EPC Governance

Global Procurement Economics & Localized Czech Compliance

Combining cost-competitive Chinese advanced fabrication with comprehensive European safety and electrical certifications (CE, ATEX, EN 12753, PED).

CAPEX & Lead Time Advantages

Procuring industrial RTOs or solvent recovery hardware directly from Hangzhou DryAir yields a 30% to 45% CAPEX advantage compared to domestic Western European EPC contractors. With 200+ systems produced monthly across our certified facilities, standard delivery timelines are curtailed to 12–16 weeks from drawing approval to freight dispatch.

Full European Conformity (CE & ATEX)

Every abatement installation configured for the Czech and broader European market carries full third-party verified CE Marking. We strictly implement EN 12753 (Thermal cleaning systems for exhaust gas from surface treatment), ATEX Directive 2014/34/EU for hazardous zone explosion safety, Pressure Equipment Directive (PED 2014/68/EU), and Low Voltage Directive (LVD).

Central European Field Engineering

Cross-continental procurement is safeguarded by our established engineering field support network. Our European-based service partners and dispatch engineers handle on-site supervision, mechanical erection, electrical tie-ins to plant SCADA/DCS (Siemens TIA Portal), statutory emissions stack testing, and routine maintenance with localized spare parts reserves.

Standard Turnkey Execution Protocol for Czech Capital Projects

01

Process Audit

Comprehensive exhaust characterization: air volume, temperature, solvent speciation, moisture, LEL envelope, and Czech ELV requirements.

02

Thermo-Fluid Modeling

Computational Fluid Dynamics (CFD) simulation of chamber flow, poppet valve switching, and ceramic thermal gradient verification.

03

Precision Factory Build

Fabrication in Hangzhou under ISO 9001 and GJB aerospace standards; full pre-shipment FAT (Factory Acceptance Test) validation.

04

On-Site SAT & Comm.

Bilingual engineers oversee mechanical anchoring, piping integration, burner tuning, and official ČIŽP emission qualification.

05

Lifecycle Service

24/7 cloud telemetry, optional 2-year warranty service agreements, rapid ceramic media and pneumatic valve parts availability.

Engineering Depth You Can Audit

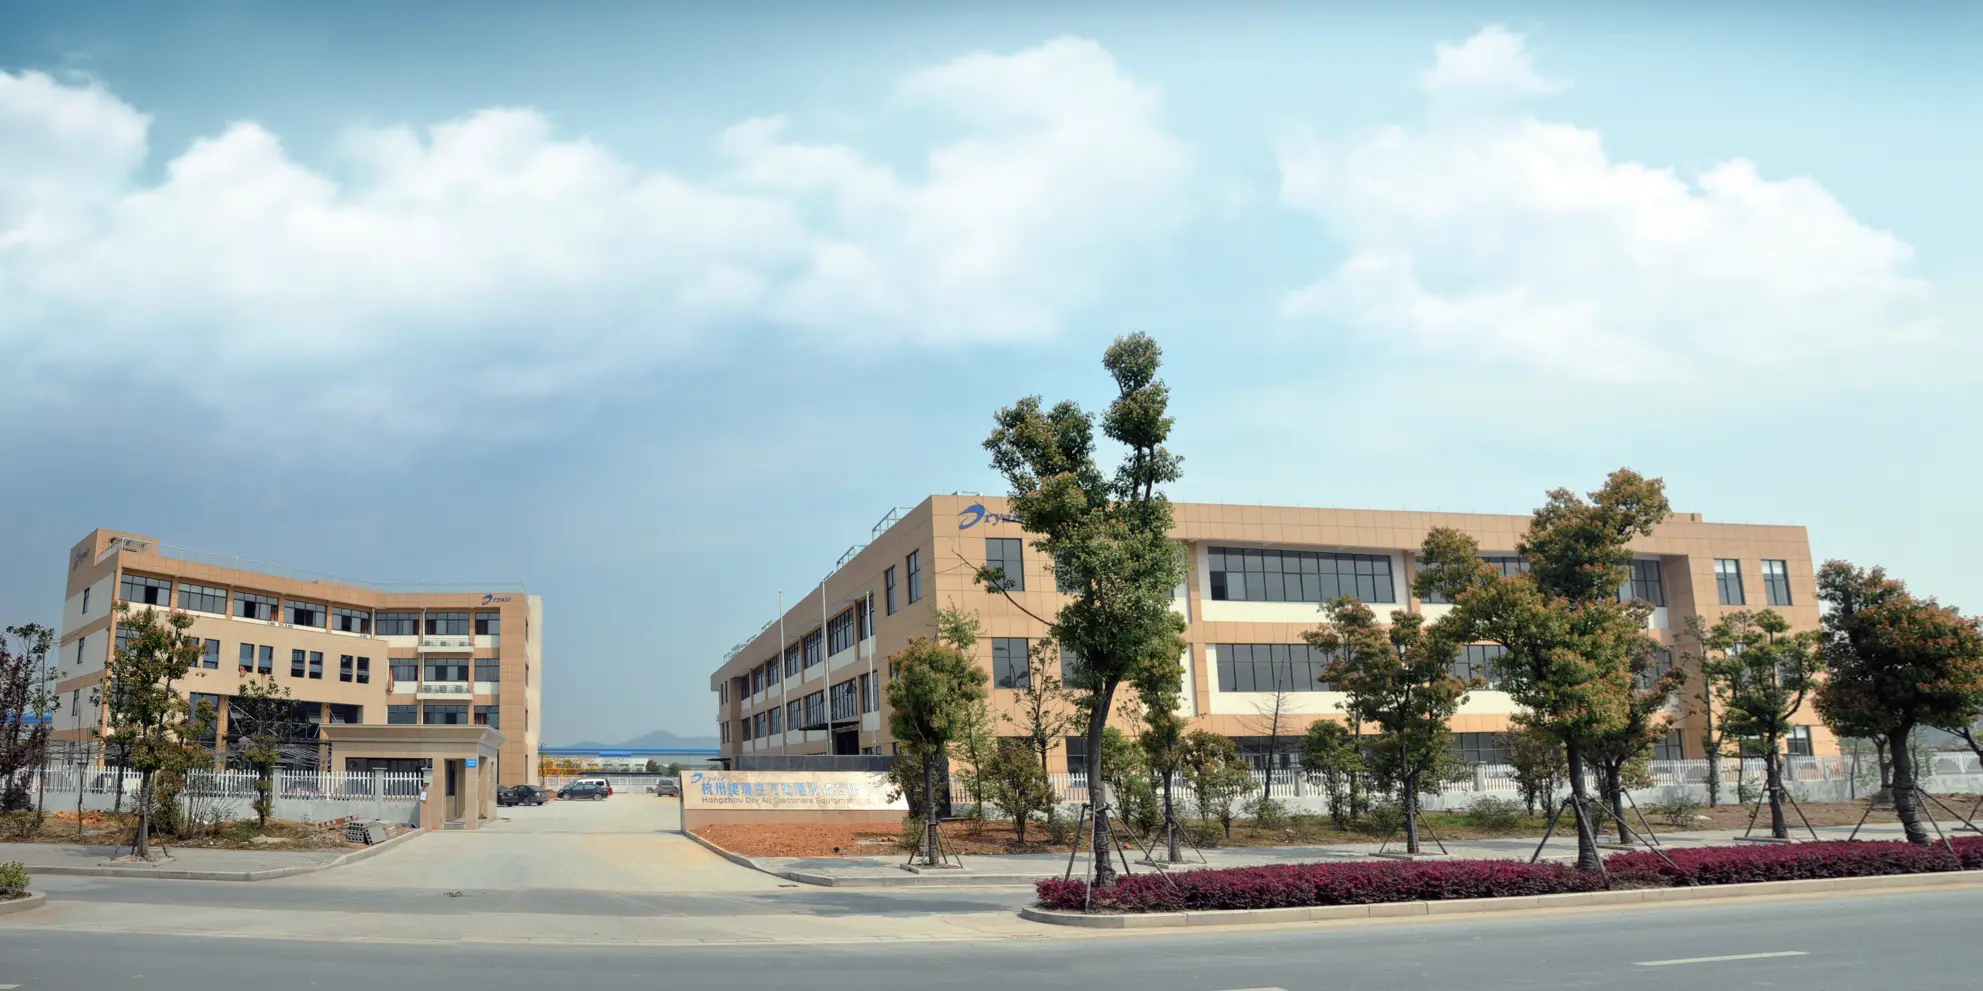
Hangzhou DryAir Treatment Co., Ltd. at a Glance

Empowering the world's most demanding advanced manufacturing plants with cutting-edge environmental and low-dew-point environmental control since 2010.

Headquartered in Lin'an, Hangzhou, Zhejiang, DryAir operates as one of the top three rotary environmental engineering and VOC control manufacturers in China, commanding over 30% domestic market share across gigawatt-scale battery cleanrooms and VOC recovery units.

With a multidisciplinary technical division encompassing 74 specialized engineers, PhDs, masters graduates, and registered national HVAC experts, we architect end-to-end industrial solutions. From ultra-low dew point control reaching -70°C to NMP recovery efficiencies surpassing 99%, we eliminate failure modes from early design stages through commissioning.

ISO 9001 Quality System GJB National Military Standard CE, UL, CSA, ASME, EAC Certified
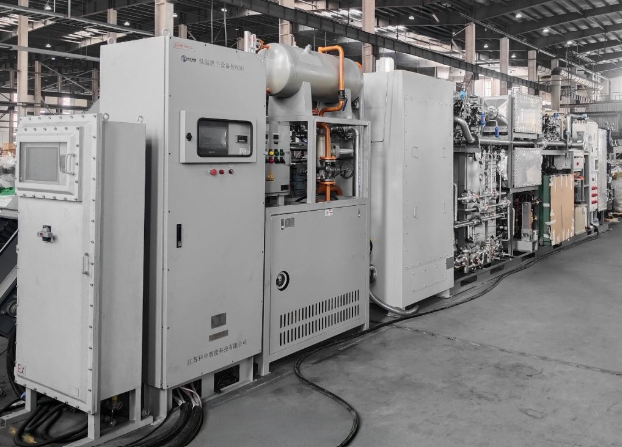
Hangzhou DryAir Heavy Industrial Manufacturing Plant and Performance Testing Room
-70°C
Min. Controllable Dew Point
≥99%
NMP Solvent Recovery Rate
30%+
National Market Share
200+
Monthly Unit Output
74
R&D Engineers & Specialists
Future Outlook

Technology Roadmap (2025–2030): Decarbonization & Intelligent Air Cleaning

Where environmental compliance intersects with circular manufacturing, green hydrogen burner compatibility, and AI predictive maintenance.

H₂-Blend & Electric RTO Heating

To support the Czech Republic's net-zero transition and decouple factory operations from fossil gas vulnerabilities, DryAir's 2025–2028 roadmap introduces dual-fuel burners capable of burning up to 100% green hydrogen, alongside Megawatt-class silicon-carbide (SiC) electrical heating oxidizers powered directly by on-site industrial solar PV arrays.

AI Edge Thermocycling Algorithms

Integrating edge-computing PLC controllers running real-time neural network models that predict thermal bed saturation, poppet valve response latency, and concentration swings. The system dynamically micro-adjusts valve cycle timings (from 90s down to 45s) to extinguish VOC release spikes during purge transitions.

Deep Waste Heat Cogeneration

Moving beyond simple secondary heat exchangers. Our advanced thermal recovery cascades integrate waste heat directly into district heating loops, high-temperature thermal oil circuits (up to 250°C) for curing ovens, or steam regeneration cycles for desiccant dehumidifiers—achieving plant-wide energy integration.

Engineering Insights

Industrial Technical Articles & Field Case Files

Field engineering analyses addressing continuous operational challenges across VOC control, humidity management, and solvent recovery.

Direct Questions & Answers

Engineering & Procurement FAQ for the Czech Republic

Straightforward answers regarding compliance, thermal performance, delivery logistics, and lifecycle servicing.

Can DryAir RTO and VOC abatement systems guarantee compliance with Czech Act No. 201/2012 Coll.?
Yes, absolutely. Our 3-bed and rotary valve Regenerative Thermal Oxidizers (RTO) achieve a guaranteed Destruction Removal Efficiency (DRE) of ≥99.5%. When processing typical solvent emissions (such as ethyl acetate, toluene, xylene, MEK, and alcohols from painting or coating lines), the clean gas stack exhaust concentration is consistently maintained below 20 mg TOC/Nm³, fully compliant with both the Czech Clean Air Act (Zákon č. 201/2012 Sb.) and the European Union BAT-AEL benchmarks under the Surface Treatment Using Organic Solvents (STS) BREF.
What is the minimum controllable dew point achievable by DryAir desiccant dehumidification systems?
DryAir rotary desiccant dehumidifiers can reliably control supply air down to a minimum of -70°C dew point (equivalent to moisture content <0.0033 g/kg of dry air). This ultra-low humidity environment is essential for lithium battery cell assembly, electrolyte filling, solid-state battery R&D, and specialized military pyrotechnic storage facilities across Europe.
How does a China-based factory manage installation, FAT/SAT, and after-sales service in the Czech Republic?
We operate a proven hybrid turnkey model. System engineering, simulation, modular fabrication, and rigorous Factory Acceptance Testing (FAT) occur at our Hangzhou manufacturing center. For European site deployment, DryAir dispatches experienced bilingual commissioning supervisors who work alongside accredited local mechanical, electrical, and ductwork engineering contractors in the Czech Republic. We provide on-site SAT (Site Acceptance Test), coordinate with regional environmental test labs for emission verification, offer an optional 2-year international warranty service agreement, and maintain critical spare parts inventory for immediate dispatch.
Which European safety and electrical certifications are supplied with DryAir export equipment?
Depending on the project specifications and end-use destination, DryAir equipment is fully engineered to conform with CE Marking (Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, EMC Directive 2014/30/EU), ATEX Directive 2014/34/EU for explosive dust/gas atmospheres, EN 12753 for thermal oxidizers, and Pressure Equipment Directive (PED 2014/68/EU). For transatlantic multinational facilities, systems can also be cross-certified to UL, CSA, ASME, and EAC standards.
What solvent recovery efficiency is attained on electrode coating lines by your NMP recovery systems?
DryAir NMP solvent recovery systems routinely achieve a total solvent recovery rate of ≥99% on continuous lithium-ion battery electrode coating and drying ovens. The recovered liquid NMP features a concentration exceeding 80–85% prior to on-site distillation and can be purified to ≥99.8% electronic grade for direct process reuse, drastically reducing raw solvent procurement costs and neutralizing hazardous VOC waste streams.
At what solvent concentration does a DryAir 3-bed RTO reach auto-thermal self-sustaining operation?
Due to our high-density ceramic honeycomb heat exchange media delivering a thermal energy recovery (TER) efficiency between 95% and 97%, our 3-bed RTO systems reach the auto-thermal (self-sustaining) threshold at VOC concentrations as low as 1.5 to 2.0 g/Nm³ (depending on the lower explosive limit and net calorific value of the specific solvent blend). Once auto-thermal balance is established, the auxiliary burner turns off completely, running with zero natural gas consumption.
Complete Equipment Portfolio

Full Engineered Product Systems Portfolio

Explore our full line of low-dew-point environmental systems, solvent recovery units, industrial dehumidifiers, and thermal VOC destruction equipment.

Accelerate Project Procurement

Deploy Compliant, Energy-Efficient VOC Abatement in the Czech Republic

Send our senior engineering team your process air volume (Nm³/h), solvent speciation, target emission limits, and site layout. We deliver full CFD simulation models, psychrometric calculations, and a complete EPC commercial proposal within 24 business hours.

Send Inquiry Now → Request 2025 Catalog
Direct Line: +86 571 8990 5557
Direct Engineering: [email protected]
Global Service: Explore Global Support Hub